What Does a Luxury Handbag Maison Actually Do: Seven Stages From Sketch to Re-Order
A luxury handbag maison carries one style from a sketch to a re-orderable reference, and it does that through seven stages: buildability, hide and lot booking, hardware, sampling with recorded corrections, pre-production, inspection and release, and the file that makes season two cheaper. The minimum is 500 pcs per style and colourway, sampling runs 6-10 working days and bulk 35-50 days, inspection is drawn to AQL 2.5 under ISO 2859-1 and terms are quoted FOB Xiamen. What follows sets the stages out in the order they actually happen.
The Decision Order: Seven Stages in the Sequence They Happen
The stages are often listed as services, which hides the thing that matters about them: each one is a gate, and each gate has to be passed in order because the next stage depends on the output of the one before. You cannot book a hide lot before the pattern tells you how many panels a bag consumes. You cannot build a prototype before the closure exists. You cannot release a run before the pre-production unit has been compared against a sealed reference. Read the sequence as a decision tree and the lead times stop looking arbitrary.
The practical consequence is that delays are almost always caused by a gate being passed out of order rather than by a stage being slow. A house that starts cutting before material declarations are filed is not being efficient; it is moving a compliance failure to the point where it costs a full run. The seven stages below each carry the one decision that has to be right before the next one opens.
Stage 1 — Is the Design Buildable? The Pattern Gate
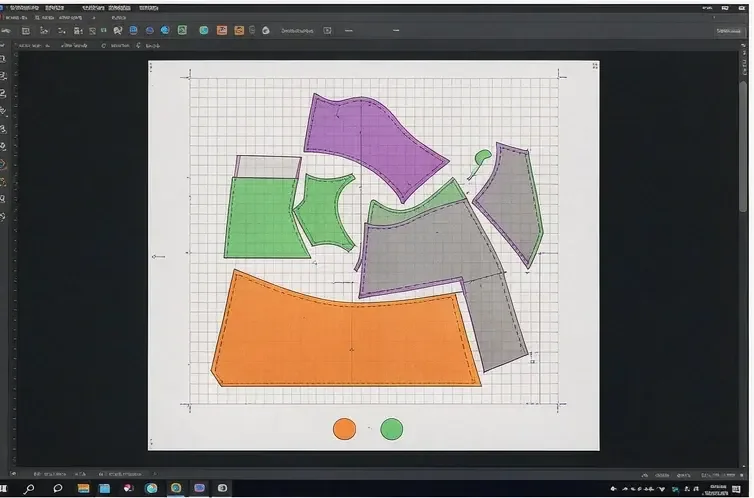
The first thing that happens to a sketch is that it becomes a pattern, and the pattern is where a design is either buildable or not. A flat envelope needs one pattern and four panels. A structured top-handle body with a gusset needs three patterns and eleven. That difference is the whole of the first gate, because it sets how many correction rounds the silhouette will need and how much judgement the work requires. A couture frame bag carries five patterns plus a frame jig, which is why it samples in 12-15 working days rather than 6-10.
The output of this stage is a revision-numbered pattern file, typically moving from Rev 00 at first cut to Rev 03 by the time a structured body is right. Every correction is logged against a revision number rather than applied silently. That log is the single most useful artefact a programme produces, because it is what stops the same correction being rediscovered on the next style.
Stage 2 — Which Hide, and Is the Lot Booked?
The pattern tells you how many panels a bag consumes, which tells you how much hide the season needs, which is the point at which the tannery lot has to be booked. A lot runs to roughly 300-500 hides and will not repeat exactly: the hand moves slightly, the finish takes dye a shade differently and the substance drifts within its band. Booking the lot is what stops a successful bag coming back marginally different in season two.
Two figures belong in this stage and are rarely asked for. Cutting yield on a structured panel runs 82-88 per cent depending on how the pattern nests, and splitting tolerance on a specified substance is held at ±0.1 mm. Together they explain why two houses can quote the same hide and return different per-bag figures: one of them is wasting more of it. Leather Working Group audit status at the tannery is the practical way to evidence the chain, and it should be requested by name.
Stage 3 — House Fitting or Custom-Cast Closure?
Hardware is decided third because it has a tooling lead time and it has to exist before the first prototype can be assembled. The decision is whether the closure is a house fitting or a custom-cast piece. A house fitting keeps cost down and the schedule short. A custom-cast clasp costs more and takes longer, and it is the only component on a bag that cannot be copied without a fresh mould — which, on a design-led line, is usually the argument that settles it.
- Closure route
- House fitting, or custom-cast clasp and turn-lock
- Custom tooling charge
- USD 450-900 per mould, one-off and reusable
- Tooling lead time
- 8-12 days before the first prototype is built
- Plating thickness
- 0.15-0.3 µm over a nickel-free undercoat
- Salt spray resistance
- 24 hours standard, 48 hours for humid markets
- Zipper specification
- #5 metal chain for a structured flap, lighter for a soft body
- Zip pull swing test
- 5,000 cycles on the finished unit, recorded per lot
- Magnet pull on a flap
- 1.2 kg minimum, tested after the bag is stuffed
Stage 4 — What Gets Read at the Bench During Sampling
Sampling is where the specification stops being a document and becomes a set of readings. The prototype is built, held beside the reference images in daylight rather than under studio light alone, and measured against the tolerance ledger. Corrections are written down and the unit is rebuilt. A structured calfskin prototype with custom hardware runs USD 180-320 and is usually credited against the bulk order.
| What is read | Working figure | When it is taken | What it catches |
|---|---|---|---|
| Panel dimension | ±1.5 mm on a cut panel | At pattern approval | A seam that will not line up in bulk |
| Finished body | ±3 mm on a stuffed bag | At prototype review | A silhouette that is right flat and wrong loaded |
| Stitch density | 8-9 stitches per inch visible | Inline during the run | A specification written but not held |
| Edge coats | Three, each about 0.12 mm wet film | Inline during the run | An edge that lifts after a season |
| Shade deviation | ΔE ≤ 1.0 under D65 | At material approval | A colour right in the studio and wrong in a shop |
| Handle load | 15 kg through 2,000 lift cycles | Pre-production | A join that fails in month three |
Stage 5 — What Happens Between Approval and Bulk
Between approval and the run sits the stage most often skipped, and it is the one that decides whether a launch is met. Material certificates are filed: hide lot, lining, thread and plating readings. A pre-production unit is built and photographed against the sealed sample. The clicker dies are cut and checked against the released pattern revision. Restricted-substance declarations are collected before dyeing and plating rather than after packing.
The output of this stage is a sealed golden sample, one per style and colourway, held on both sides. Everything downstream is measured against it — the pre-production unit, the inline checks, the final inspection and, critically, every re-order. A house without a golden sample procedure is telling you that season two will be a re-sampling exercise.
Stage 6 — How the Run Is Inspected and Released
Bulk runs 35-50 days from the approved sample. Final inspection is drawn to AQL 2.5 under ISO 2859-1 at general inspection level II, with defects classified critical, major and minor. On a 500-piece lot the sample is 50 units, accepted at 3 major defects and rejected at 4; on a 3,000-piece lot the sample is 125 units, accepted at 7 and rejected at 8. Critical defects are rejected outright regardless of count. Third-party inspection is worth adding on the first drop of any new style.
Release is then a packing and documentation exercise: dust bag, tissue, carton specification and labelling agreed before the run rather than after it, followed by export documentation and loading. Terms are quoted FOB Xiamen, with CIF and DDP available. The packing specification belongs in the purchase order as a line item, because a carton discovered after the goods are packed is expensive to redo.
Stage 7 — What Carries Into the Next Season
The last stage is the one that makes the model pay. Everything captured in the first six stages — the revision-numbered pattern, the correction log, the mould, the material approvals and the golden sample — is what makes season two faster and cheaper than season one. A re-order against a sealed reference runs 28-35 days rather than 35-50, sampling drops to a confirmation round of 3-5 days, and tooling is already paid.
The pattern file
Held at a recorded revision number against the brand, released to a second house only with written consent. This is the asset; the bag is its output.
The correction log
Every change recorded against a revision, so the same correction is not rediscovered on the next style. The clearest evidence that a specification is being held.
The tooling
A mould paid for by the brand belongs to the brand. Record the mould number and where it is held so a later season is not quoted with the tooling charge included again.
The material approvals
Hide lot, lining, thread and plating readings on file, with a named alternative finish approved in case the first is discontinued.
The golden sample
One sealed unit per style and colourway, held on both sides. Without it, the re-order has no reference and the second season becomes a re-sampling exercise.
Ask which stage the last delay came from and what the correction was. A house running these seven stages can answer in detail. A house listing services instead of gates answers with an assurance.
Seven stages, in one line each
- Buildability: pattern count sets the work. Hide: book the lot of 300-500 hides against the season. Hardware: decide before the prototype. Sampling: 6-10 working days, corrections logged. Pre-production: seal a golden sample. Release: AQL 2.5 under ISO 2859-1, FOB Xiamen. Carry-forward: re-order in 28-35 days. Minimum 500 pcs per style and colourway.
Walk your style through the seven stages
Tell us which stage you are at and what is blocking it, and our team will return the next step, a sampling schedule and a costed first order through our quotation desk.
Frequently Asked Questions
What does a luxury handbag maison actually do?
It carries a style from a sketch to a re-orderable reference through seven stages: buildability and pattern, hide and lot booking, hardware, sampling with recorded corrections, pre-production, inspection and release, and the carry-forward file that makes season two cheaper.
What is the first thing that happens to a new design?
It becomes a pattern. The pattern count sets everything downstream — a flat envelope needs one pattern and four panels, a structured gusseted body three patterns and eleven, and a couture frame bag five plus a frame jig.
How many patterns does a structured handbag need?
A structured top-handle body with a gusset needs three patterns and eleven cut panels, and usually two to three sample rounds. A flat envelope needs one pattern and four panels and one to two rounds. That difference is why the two sample in different windows.
Why does the hide lot have to be booked in advance?
Because a lot runs roughly 300-500 hides and will not repeat exactly — the hand moves, the finish takes dye a shade differently and the substance drifts. Booking the lot and retaining a swatch is what stops a successful bag returning marginally different in season two.
What is cutting yield and why does it matter?
Cutting yield is the share of the hide that becomes panels, running 82-88 per cent on a structured body depending on how the pattern nests. It is the main reason two houses quoting the same hide return different per-bag figures: one of them is wasting more of it.
When is the hardware decision made?
Before the first prototype is built, because the metal part has to exist before the unit can be assembled. A custom-cast clasp adds USD 450-900 per mould and 8-12 days of tooling lead time, and it is the only component that cannot be copied without a fresh mould.
How long does sampling take?
6-10 working days for a standard construction and 12-15 where a frame or a custom-cast clasp is involved, plus a correction round of 5-7 days. A structured calfskin prototype with custom hardware runs USD 180-320 and is usually credited against the bulk order.
What is a golden sample and when is it sealed?
The golden sample is the approved physical unit, sealed one per style and colourway and held on both sides. It is sealed at pre-production, after material certificates are filed and the unit has been photographed against the sealed reference — not at final inspection.
How is a bulk run inspected before release?
Final inspection is drawn to AQL 2.5 under ISO 2859-1 at general inspection level II, defects split critical, major and minor. On a 500-piece lot the sample is 50 units, accepted at 3 major defects and rejected at 4. Critical defects are rejected outright.
How long does bulk production take?
35-50 days from the approved sample, followed by packing, export documentation and loading. Terms are quoted FOB Xiamen with CIF and DDP available. A re-order against a sealed reference runs faster at 28-35 days.
What makes the second season cheaper than the first?
The carry-forward file: the revision-numbered pattern, the correction log, a mould already paid for, material approvals on file and a sealed golden sample. Together they cut the schedule to 28-35 days and reduce sampling to a confirmation round.
What compliance work happens and when?
REACH Annex XVII for the European Union, Prop 65 for California, CPSIA for the United States and EU Regulation 1007/2011 for fibre naming. Declarations are collected from the tannery and plating house before dyeing and plating begin, because the remedy after packing is a re-run.
What is the minimum order to start a programme?
500 pcs per style and per colourway, quoted FOB Xiamen. It reflects fixed cutting, hide purchase and set-up costs. A silhouette can be tested below that figure as a sampling exercise, but the per-bag figure rises steeply below the minimum.
How is colour controlled across a season?
Against a retained physical swatch in a D65 light booth, held at ΔE ≤ 1.0, with colour-fastness verified to ISO 105, finish adhesion to ISO 11644 and tensile strength to ISO 3376. A named alternative finish is approved at the same time.
People Also Ask
What stages does a handbag go through from sketch to delivery?
Seven: buildability and pattern, hide and lot booking, hardware tooling, sampling with logged corrections, pre-production and golden sample, inspection and release, then the carry-forward file. Each is a gate that has to be passed in order.
What is a pre-production sample in handbags?
The unit built after material certificates are filed and before the full run starts, photographed against the sealed reference. It is the last point at which a construction fault is a correction rather than a re-run.
Why does the second season of a handbag cost less?
Because the pattern, the correction log, the mould and the material approvals are reused rather than recreated. A re-order runs 28-35 days instead of 35-50, and sampling falls to a confirmation round of 3-5 days.
What does AQL 2.5 mean on a 500-piece order?
Under ISO 2859-1 at general inspection level II, the drawn sample is 50 units, accepted at 3 major defects and rejected at 4. Critical defects are rejected outright. Third-party inspection is worth adding on a first drop.
How much hide does a handbag consume?
It depends on pattern nesting rather than bag size: cutting yield on a structured body runs 82-88 per cent, with splitting tolerance held at ±0.1 mm against the specified substance.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- ISO — International StandardsInternational Organization for Standardization Publisher of ISO 2859-1 sampling procedures, ISO 105 colour fastness, ISO 11644 finish adhesion and ISO 3376 tensile strength.
- Leather Working GroupLeather Working Group Tannery audit protocol used to evidence a hide chain and to book a lot of 300-500 hides against a season.
- Understanding REACHEuropean Chemicals Agency Annex XVII restrictions on chromium VI, azo dyes, nickel release and phthalates in leather and plated hardware.
- CPSC — Business EducationU.S. Consumer Product Safety Commission CPSIA lead limits, phthalate restrictions and tracking label requirements for goods placed on the United States market.