Luxury Handbag Hardware: Seven Numbers That Separate a Grade From a Look
What separates one grade of luxury handbag hardware from another? Seven numbers: base metal density, plating thickness in microns, the underlayer beneath it, salt spray hours to ISO 9227, plating adhesion, cycle life of any moving part, and dimensional tolerance. Brass sits at 8.4 g/cm³ against zamac at 6.6, gold plating runs 0.15-0.3 µm as a flash and 0.5-1.0 µm as a heavy deposit, and a luxury closure is tested to 24-48 hours of salt spray.
Seven Numbers That Define a Hardware Grade
Hardware is sold on appearance and bought on numbers. Two turn-locks of identical shape and finish can differ by a factor of four in service life, and the difference is entirely in the seven figures below rather than in anything visible.
Ask for all seven on the quotation rather than on the drawing. A component quoted with a finish name and nothing else is a component whose grade has not been specified, and it will be delivered at whatever the line found available that week.
- Base metal density
- Brass 8.4 g/cm³, zamac 6.6 g/cm³, stainless steel 7.9 g/cm³
- Plating thickness
- Gold 0.15-0.3 µm flash, 0.5-1.0 µm heavy; palladium 0.3-1.0 µm
- Underlayer
- Nickel or palladium barrier of 3-5 µm beneath the decorative layer
- Salt spray
- ISO 9227, 24 hours for a standard grade and 48 hours for a premium one
- Plating adhesion
- No lifting after thermal shock and tape testing on the finished component
- Cycle life
- 500 cycles for a standard closure, 1,000 for a premium one
- Dimensional tolerance
- ±0.1 mm on a die-cast component, ±0.05 mm on a machined one
Seven Component Types and What Each Has to Do
Seven families cover almost everything fitted to a handbag, and each has one job that defines its grade. Specifying them all to the same standard is the commonest waste in a hardware bill; specifying the closure to the lowest one is the commonest failure.
| Component | The job it has to do | What grades it | Typical finish |
|---|---|---|---|
| Turn-lock and clasp | Close and release 500-1,000 times without losing tension | Cycle life and spring temper | Palladium, light gold, brushed |
| Zipper | Run 500-1,000 cycles with the slider tracking true | Gauge, tape and slider pull force | Metal teeth #3 or #5, plated |
| Feet | Keep the base off a surface for the life of the piece | Fixing method and plating thickness | Palladium or dark ruthenium |
| D-rings and strap ends | Carry load without opening | Base metal strength and weld quality | Matched to the closure |
| Chain and strap hardware | Carry load and resist kinking | Link section and plating at the contact points | Light gold or palladium |
| Magnetic closures | Hold shut without visible hardware | Gauss rating and corrosion resistance of the housing | Hidden, usually unplated steel |
| Nameplates and logos | Look right and stay attached | Fixing method and edge finishing | Matched to the closure |
Base Metals: Brass, Zamac, Stainless Steel and Aluminium
Base metal governs weight, strength and how well a component takes plating. Brass, a copper-zinc alloy, is the reference for luxury hardware: dense, machinable, and it accepts a plating layer that stays put.
Brass
Around 8.4 g/cm³, and the reference material for fine hardware. Machines to a crisp edge, takes plating well and carries the weight that reads as quality in the hand. Costs more per component than zamac on the same geometry.
Zamac
Around 6.6 g/cm³, a zinc alloy die-cast to a tolerance of ±0.1 mm. Holds fine detail at a lower unit cost and about 25-30% less mass, and it needs a thicker underlayer to plate as durably as brass.
Stainless steel
Around 7.9 g/cm³, chosen where corrosion resistance matters more than warmth of colour. Takes a brushed finish well and is used most often for feet, frames and hidden magnetic housings.
Aluminium
Around 2.7 g/cm³, used where a large component has to stay light: a frame, a chain, an oversized pull. Anodised rather than plated, and the colour range is narrower.
The density figures are worth reading as a weight decision as much as a materials one. On a closure-led design, hardware carries 12-20% of unit weight, and brass against zamac on the same geometry is a 25-30% difference on that share.
Plating: Thickness in Microns, and Where It Wears
Plating is measured in microns and it wears where something rubs it. A flash of gold at 0.15-0.3 µm is a colour, and it will wear through at a contact point within a season; a heavy deposit at 0.5-1.0 µm over a 3-5 µm barrier layer survives ordinary use.
- Flash gold: 0.15-0.3 µm, a colour rather than a surface, suited to low-contact parts.
- Heavy gold: 0.5-1.0 µm, suited to closures, feet and anything the hand touches.
- Palladium: 0.3-1.0 µm over a barrier layer, the commonest luxury finish.
- Ruthenium and gunmetal: darker finishes that show wear less, but chip more when they go.
- Barrier layer: 3-5 µm of nickel or palladium beneath the decorative deposit.
The fifth item is the one that separates a specification from a request. The decorative layer is what is seen; the barrier layer is what keeps it attached, and it is the figure most often omitted from a quotation.
Finishes: How the Surface Is Made, Not Just How It Looks
Finish describes the surface treatment applied after plating: polished, brushed, satin, antiqued or matte. Two components with the same plating thickness and different finishes wear differently, because a polished surface shows every mark and a brushed one hides them.
Antiqued finishes deserve a note. A deliberately darkened recess is applied by hand or by a controlled process, and it will lighten at contact points, which is the intended behaviour and should be stated rather than discovered.
Brushed finishes hide wear and polished finishes advertise it, which is why the same plating thickness produces different complaint rates on two components of identical shape. Where a component sits at a contact point, a brushed or satin surface is the more forgiving choice at any grade.
Testing Hardware: Four Checks Before Bulk
Four checks cover most of what goes wrong with hardware in service. All four can be run on a sample batch, and each produces a pass or a fail rather than an opinion.
- Salt spray to ISO 9227: 24 hours for a standard grade, 48 for a premium one, with no base metal corrosion.
- Cycle the closure 500 times, or 1,000 for a premium grade, and confirm tension is retained.
- Thermal shock followed by tape testing, to confirm the plating has bonded to the base metal.
- Pull test the fixing at 150-250 N, depending on the component and where it sits.
The third check is the one that predicts the failure customers complain about most. Plating that lifts in flakes months after delivery has failed at the bond, and no amount of thickness in the decorative layer prevents it.
A thicker decorative layer over a weak bond peels in larger flakes. Test the bond with thermal shock and tape before you test the surface, and specify the barrier layer alongside the deposit.
Grade Bands: Four Levels and Where Each Belongs
Four bands describe the market honestly, and the right answer is usually to mix them rather than to pick one. A body needs one grade at the closure, another at the feet and a third on a nameplate nobody touches.
| Band | Typical specification | Where it belongs | What it costs |
|---|---|---|---|
| Standard | Zamac, 0.15-0.3 µm flash, 24 h salt spray | Internal fixings, hidden components | Lowest unit cost |
| Mid | Zamac or brass, 0.3-0.5 µm, 24-48 h salt spray | D-rings, strap ends, nameplates | Moderate, and the usual default |
| Premium | Brass, 0.5-1.0 µm over 3-5 µm barrier, 48 h salt spray | Closures, feet, zippers | Highest, and worth it at contact points |
| Bespoke | Machined brass, custom tooling, 1,000 cycles | Signature hardware on a hero style | Tooling cost plus a higher unit price |
Zipper Hardware: The Component With a Mechanism
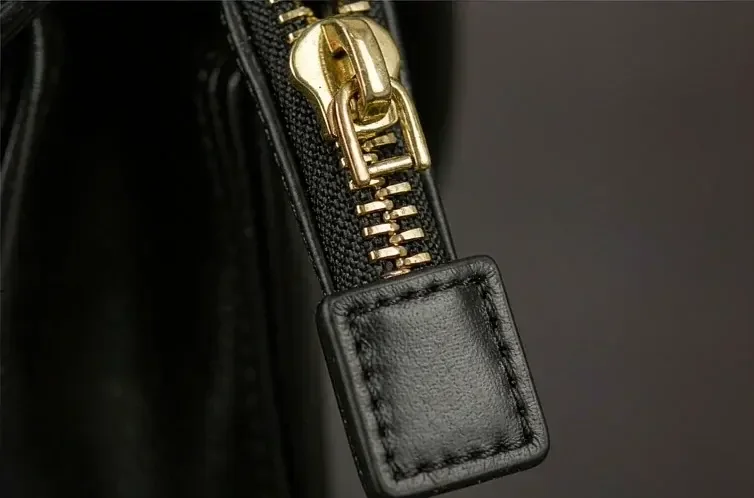
A zipper is the only hardware component with moving parts, and it fails mechanically long before it fails cosmetically. Specify it by gauge, tape and slider rather than by finish alone.
- Gauge: #3 for an interior pocket, #5 for a main closure, #8 for a travel body.
- Tape: 12-15 mm woven, colour matched to the lining or deliberately contrasted.
- Slider pull force: 40-60 N, light enough to run and heavy enough not to self-open.
- Cycle life: 500 cycles for an interior pocket, 1,000 for a main closure.
- Stop and top: metal stops rather than stitched ones on a luxury body.
The second item is a colour decision that is often made too late. A tape matched to the lining keeps the interior quiet; a contrasted tape makes the closure a design line, and both need the tape ordered with the zipper rather than after it.
Cost and Schedule: What a Grade Buys
Hardware runs 12-20% of FOB cost on a closure-led design, and the grade chosen moves that share within a narrow band. What a higher grade buys is not a lower defect rate at intake; it is a lower complaint rate in year two.
Schedule is where bespoke hardware bites. Custom tooling carries its own development time ahead of sampling, and it is booked before the first sample is cut rather than after it is approved. Presentation packing runs separately at about USD 4.80 per unit.
The Hardware Line on the Specification Sheet
A hardware specification is eight lines per component, and it is the part of a tech pack most often filled in with a photograph and a finish name. Neither is enforceable at intake.
Eight lines before you sign a hardware specification
- Base metal named, with the alloy reference where one applies.
- Plating thickness in microns for the decorative layer, as a range.
- Barrier layer thickness in microns beneath it.
- Finish named: polished, brushed, satin, antiqued or matte.
- Salt spray hours to ISO 9227, with the acceptance criterion stated.
- Cycle life for any moving part, with the count stated.
- Dimensional tolerance on the component, in millimetres.
- Fixing method and pull test figure for the component in position.
Our programme works to MOQ 500 pcs per style and colourway, with sampling at 6-10 working days and 12-15 for a complex construction, bulk at 35-50 days on FOB Xiamen terms, inspected to AQL 2.5 under ISO 2859-1. It runs across 7 production lines with about 200,000 pcs per month of capacity and export experience since 2014, delivered through our validated partner factory Quanzhou Yingming Bags, an SGS-validated site. The framework sits under luxury materials and the bench detail under craftsmanship.
Send the hardware list and we will grade it
Tell us the components, the finish you want and where each one sits. We will return the base metal, the plating build, the test figures and a sampling calendar, within two working days. Request a quote.
Frequently Asked Questions
What is the best base metal for luxury handbag hardware?
Brass, at around 8.4 g/cm³, is the reference material: dense, machinable and it holds a plating layer well. Zamac at 6.6 g/cm³ costs less and weighs about 25-30% less on the same geometry, and it needs a thicker barrier layer to plate as durably.
How thick should gold plating be on a handbag closure?
Between 0.5 and 1.0 µm for a heavy deposit over a 3-5 µm barrier layer, on any part the hand touches. A flash at 0.15-0.3 µm is a colour rather than a surface and will wear through at a contact point within a season.
What does a salt spray test actually prove?
It accelerates corrosion so a plating system can be compared, run to ISO 9227 for 24 hours on a standard grade and 48 on a premium one. The acceptance criterion matters as much as the hours: no base metal corrosion, rather than no visible change at all.
Why does plating flake off in sheets?
Because the bond failed rather than the surface wearing. A decorative layer applied over an inadequate barrier, or over a base that was not properly prepared, lifts in flakes months after delivery. Thermal shock followed by tape testing catches it at sampling. Write the figure into the specification, since an unrecorded figure cannot be enforced at intake.
How many cycles should a closure survive?
500 cycles for a standard grade and 1,000 for a premium one, with tension retained at the end. The figure is worth stating because a closure that still closes but has lost its tension is a closure a customer will not trust with the contents.
Should all hardware on one bag be the same grade?
No. Mixing is the better answer: premium at the closure, feet and zipper, where contact happens; mid at D-rings and strap ends; standard on internal fixings nobody touches. Specifying everything to the premium band wastes money in places it is never seen. Confirm it at sampling, which runs 6-10 working days, or 12-15 for a complex construction.
What zipper gauge should a handbag use?
#3 for an interior pocket, #5 for a main closure and #8 for a travel body, with metal stops rather than stitched ones. Tape runs 12-15 mm and is ordered with the zipper, since matching it to the lining afterwards is not possible. Check it per lot at intake, inspected to AQL 2.5 under ISO 2859-1.
How is hardware weight managed on a large body?
By choosing the base metal per component. Brass at 8.4 g/cm³ against zamac at 6.6 is a 25-30% saving on one geometry, and taking that saving on components the hand does not land on changes the scale reading without changing what is felt.
What dimensional tolerance should hardware be held to?
±0.1 mm on a die-cast component and ±0.05 mm on a machined one. Tolerance matters most on a closure, where the two halves have to meet without force, and on any component that is set into a prepared recess in the leather. Our programme works to MOQ 500 pcs per style and colourway, with bulk at 35-50 days.
Does hardware need to meet REACH or Prop 65?
Yes, as part of the article. REACH Annex XVII restricts certain substances in articles placed on the European Union market, including nickel release and lead in metals, and California Prop 65 governs warnings in that state. Both are shown with test reports per lot. Keep the result with the retained sample so a re-order can be checked against it.
How much does bespoke hardware add to a schedule?
Custom tooling carries its own development time ahead of sampling, so it is booked before the first sample is cut. Sampling then runs 6-10 working days, or 12-15 for a complex construction, and bulk 35-50 days on FOB Xiamen terms. Agree the detail before the order is placed and hold it across the life of the style.
What share of unit cost is hardware?
Around 12-20% of FOB cost on a closure-led design, higher where a bespoke closure carries tooling. The grade chosen moves that share within a narrow band; what a premium grade buys is a lower complaint rate in year two rather than a lower defect rate at intake.
People Also Ask
Is brass hardware better than zamac?
Brass is denser, machines to a crisper edge and holds plating better. Zamac is about 25-30% lighter and less costly on the same geometry. The right answer is usually brass at contact points and zamac where the hand does not land.
Why does my gold hardware lose its colour?
The decorative layer has worn through, usually because it was a flash at 0.15-0.3 µm rather than a deposit at 0.5-1.0 µm. Contact points wear first: the closure, the feet and the strap rings.
What is a barrier layer in plating?
A nickel or palladium layer of 3-5 µm applied beneath the decorative deposit. It stops migration between the base metal and the surface and it is what keeps the decorative layer attached in service.
How do I know if hardware will corrode?
Ask for a salt spray result to ISO 9227 with the hours stated and an acceptance criterion. 24 hours is a standard grade and 48 is premium. Corrosion shows first at edges and in recesses, where the deposit is thinnest.
Should hardware be tested on the bag or on its own?
Both. Salt spray and adhesion are tested on the component, while cycle and pull testing are done in position on a sample body, because the leather around a fixing changes how load is carried.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- ISO — International Organization for StandardizationISO Publisher of ISO 9227 on salt spray testing, ISO 2859-1 on sampling procedures and the fastness series used on trims.
- Institute of Materials, Minerals and MiningIOM3 Reference data on copper alloys, zinc alloys and the densities and mechanical properties of hardware base metals.
- ECHA — European Chemicals AgencyEuropean Chemicals Agency Administrator of REACH, including the Annex XVII restrictions on nickel release and lead in metal components.
- Office of Environmental Health Hazard AssessmentOEHHA The California agency that administers Proposition 65 and its warning requirements for listed substances in articles.
- YKK CorporationYKK Zipper and hardware reference on gauges, tape widths and the cycle testing of sliding fasteners.