Luxury Handbag Hardware Certification Checklist: Twelve Points, the Document for Each, and What Fails an Audit
Hardware certification for a luxury handbag is a file, not a certificate. It consists of twelve points grouped into three families: chemical compliance, plating and corrosion records, and mechanical performance. Each point has a document that proves it and a substitute that merely resembles it. This checklist sets out all twelve, names the document for each, and shows the gap an auditor finds when the substitute has been filed instead.
How to Use This Checklist
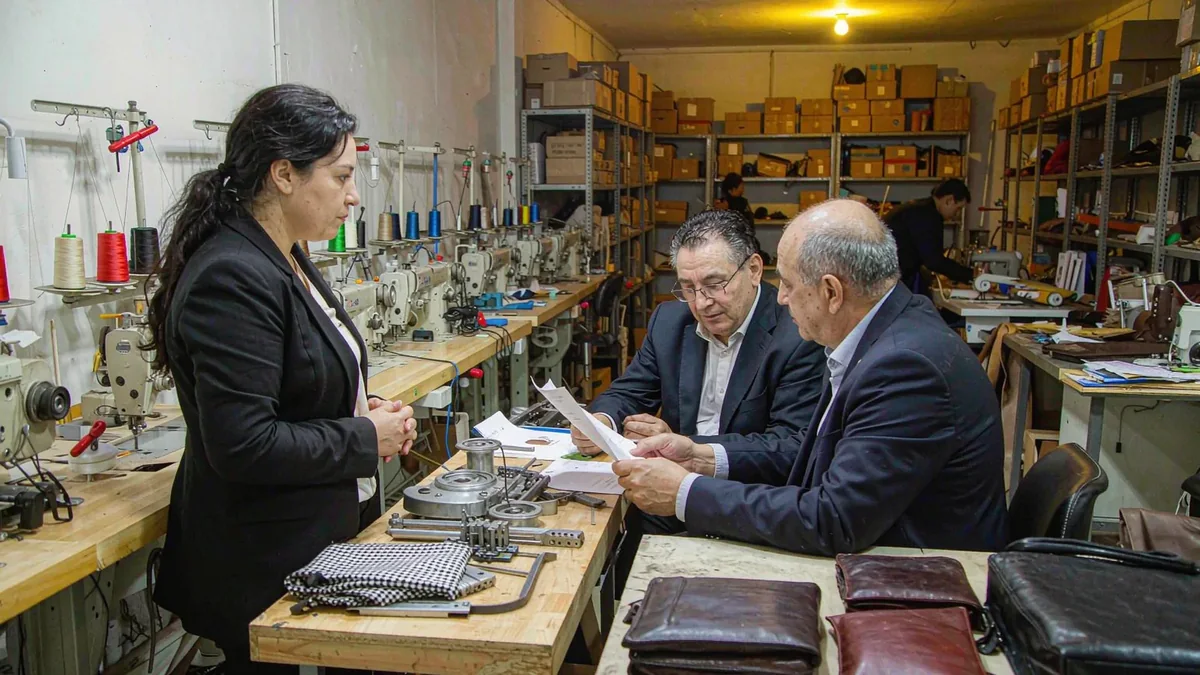
Work through the twelve points at quotation stage rather than at delivery. Every item on this list is obtainable before bulk begins and almost none of them can be produced honestly afterwards. A plating bath log written at the time costs one line in a record; the same log reconstructed eight weeks after a shipment has landed cannot be written at all, and an auditor knows the difference.
The second rule is that every document names a lot. A test report addressed to a company proves the result for the sample that company chose to submit. A report naming your lot reference and the date your material was drawn proves the result for the bag you are about to ship. The difference is one line of text and it decides whether the file survives review.
The Twelve Points
Twelve points, in three families of four. The third column is the one to read if you are short of time: it names the substitute most often filed in place of the real document, and the substitute is what fails.
| Point | Document that proves it | What is filed instead, and fails |
|---|---|---|
| 1. Substrate declared | Mill certificate naming the alloy or the melt, per component | A part number on a purchase order |
| 2. Plating thickness | XRF reading in micrometres, recorded per bath | A finish name such as light gold or palladium |
| 3. Corrosion resistance | ISO 9227 neutral salt spray result, 24 or 48 hours | A note that the finish is durable |
| 4. Cycle life | 5,000 open-close cycles with the action inspected at the end | A sample that opened and closed well once |
| 5. Pull force | 3.0 kgf at a locked cam, 2.5-3.5 kgf for a magnet | Nothing at all, which is the commonest gap |
| 6. Torque on fixings | Torque check on every threaded part after cycling | A screw that felt tight on the sample |
| 7. Nickel release | REACH Annex XVII entry 27 result, per lot | A general REACH statement from a previous year |
| 8. Prop 65 | California listed-substance screen, per lot | A declaration covering a different market entirely |
| 9. CPSIA lead | Lead in substrate and coating, for United States lines | An assurance that the metal is safe |
| 10. Detachment risk | Critical classification with a pass on every fixing | A visual check that nothing looked loose |
| 11. Bath traceability | Bath ID, date, alloy and thickness for each run | A finish sample approved at the start of the season |
| 12. Retained reference | One sealed component per bath, held 24 months | A photograph of the approved sample |
Points five and twelve are the two most frequently missing from a real file. Pull force is omitted because nobody doubts a magnet until it fails, and the retained reference is omitted because it costs a component and a shelf.
Chemical Compliance: REACH, Prop 65 and CPSIA
Three regimes govern metal components on a handbag sold internationally, and they are answered per lot rather than per programme. A result from a previous season describes a previous material, and an auditor will read the date before reading the number.
- REACH Annex XVII entry 27 governs nickel release from articles in prolonged contact with skin, which includes a closure and a strap end.
- California Proposition 65 governs warning requirements for listed substances, and is screened per component rather than per bag.
- CPSIA sets limits on lead in substrates and coatings, and applies wherever the line sells into the United States.
- A chemical report must name the laboratory, the method, the limit and the result; a statement without those four is not a result.
- The report is tied to the lot, and a re-selected lot invalidates it completely.
- Destination markets belong in the brief at quotation, because the screen is chosen by market rather than by habit.
One point that catches houses out: prolonged contact is interpreted broadly. A metal foot that touches a table and a metal strap end that touches a hand are both in scope, and a component dismissed as decorative at the drawing stage is often in scope at the audit.
Screens should be booked rather than hoped for. A laboratory needs the component list, the destination markets and the lot reference before it can quote a turnaround, and a screen ordered at the end of a programme is the commonest reason a finished shipment waits at a port while a report is written.
Plating and Corrosion Records
Plating is the part of the file most houses believe they have and usually do not. What exists is a finish name on a drawing; what is needed is a thickness reading in micrometres tied to a bath, plus a corrosion result tied to the same bath.
- Gold tone thickness
- 0.15-0.3 µm over a 3-5 µm nickel barrier, read by XRF
- Pale gold thickness
- 0.2-0.4 µm, because a pale finish shows wear sooner
- Palladium on brass
- 0.20 µm palladium over solid brass, recorded per bath
- Salt spray standard
- 24 hours neutral spray to ISO 9227, 48 hours for antique finishes
- Bath record
- Bath ID, date, alloy and thickness reading for each plating run
- Contact-point wear
- 5,000 cycles on the assembled bag, with the face inspected for breakthrough
- Tone comparison
- Colour within ΔE 1.0 of the approved master, read under D65 light
The bath record is what makes the other numbers useful. A thickness reading with no bath ID tells you one component was correct; a reading tied to a bath tells you which other components came out of the same bath, which is the question an auditor actually asks.
Mechanical Records: Cycles, Pull and Torque
Mechanical records are the third family and the one with the clearest pass or fail. Either the lock survived five thousand cycles or it did not; either the magnet held above 2.0 kgf at the end or it did not. There is no interpretation in these numbers, which is why they belong in the pack.
Cycle test
Five thousand open-close cycles on the assembled bag, not on the loose component. Alignment faults appear only when the lock sits on the panel, which is why the rig alone is not enough.
Pull force
Three kilograms force at a locked cam, and 2.5-3.5 kgf for a magnet pair, re-tested after cycling rather than before. A lock that cycles smoothly and releases under load has not been specified.
Torque check
Every threaded part is torque-checked after cycling. A fixing screw that works loose in a single layer of leather is a detachment risk, which is classed critical rather than major.
Detachment
Rivets, magnets and screws are pulled and cycled, with no movement accepted. A component that can release is never a cosmetic fault, and no allowance covers it at inspection.
A cosmetic fault on a visible face is a major and counts against the AQL 2.5 allowance. A component that can release is critical and accepts none. Write both classes onto the inspection sheet before the draw, because deciding at the table is how a shipment that should stop gets released.
Documents to File Per Lot
Four documents carry the certification file, and all four are filed per lot. Filed per programme, they describe an intention; filed per lot, they describe the bag.
- Substrate and melt certificate
- Names the alloy, or the melt where recycled content is claimed, per component
- Chemical test report
- Laboratory, method, limit and result, tied to the lot and dated
- Plating bath log
- Bath ID, date, alloy, thickness reading and salt spray result
- Mechanical test record
- Cycle count, pull force and torque result on the assembled bag
A fifth item is worth adding even though no standard requires it: one sealed component per bath, held for 24 months. It is the only way to settle a later disagreement about tone or finish against the object rather than against a photograph.
Who Signs What
Four parties touch this file and each owns a different part of it. Confusion about ownership is the commonest reason a point goes unclaimed and then unproven.
The house
Owns the brief: which markets, which components are in prolonged skin contact, and which classes apply at inspection. Without this the laboratory screens the wrong things.
The component maker
Owns the substrate and melt certificate, the bath log and the thickness reading. These are produced at the time or not at all.
The laboratory
Owns the chemical report, and must be independent of the component maker for the result to carry weight at an audit.
The bench
Owns the mechanical record: cycle count, pull force and torque on the assembled bag, plus the retained component filed against the bath.
The ownership question resolves most delays in this file. A point that is unclaimed is nobody's task to produce, and a point claimed at quotation becomes a condition of approval rather than a request made after delivery. One line in the brief naming who holds each document removes the largest single cause of a missing report.
Common Gaps Found at Audit
Six gaps appear in almost every file that has never been checked against this list. Each has a fix that costs a line in a specification.
- The chemical report names a company rather than a lot, so it describes a material nobody can identify.
- The plating thickness is recorded once at the start of a season rather than per bath, so a drift is invisible.
- The cycle test was run on the loose component, so alignment faults on the assembled bag were never found.
- Pull force is absent entirely, because nobody doubted a magnet until one failed in the field.
- The retained reference is a photograph rather than a sealed component held under controlled light.
- The inspection sheet has no critical class written on it, so a detachment risk is argued at the table.
Commercial Frame: MOQ, Sampling and Bulk
MOQ 500 pcs per style and per colourway. Sampling for a new style runs 6-10 working days, extending to 12-15 where a frame, a moulded handle or a new tool is involved. Bulk production at 35-50 days. FOB Xiamen as the standard term, with alternatives available where a programme needs them.
Inspection is drawn to AQL 2.5 under ISO 2859-1, which on a 500 pc lot at general inspection level II gives a 50-piece sample with three majors allowed and no critical defects accepted. The programme runs across 7 production lines with about 200,000 pcs per month of capacity and has held export experience since 2014, carried out through our validated partner factory Quanzhou Yingming Bags, an SGS-validated site.
Certification in five numbers
- Twelve points: four chemical, four plating and corrosion, four mechanical.
- Four documents per lot: substrate certificate, chemical report, bath log, mechanical record.
- 0.15-0.3 µm: the plating thickness read by XRF over a nickel barrier.
- 24 hours: neutral salt spray to ISO 9227, rising to 48 for antique finishes.
- 24 months: how long a sealed component per bath is retained.
Have your hardware file checked against the twelve points
Send your component list, the markets you sell into and the documents you hold. You will receive a point-by-point gap list showing what proves, what needs requesting and what must be re-run, within two working days. Request a quote.
Frequently Asked Questions
What certification does luxury handbag hardware need?
Twelve points across three families: chemical compliance for REACH, Prop 65 and CPSIA; plating and corrosion records including a bath log; and mechanical records covering cycle life, pull force and torque. Each point has a document, filed per lot.
Why must a test report name a lot?
Because a report addressed to a company proves the result for the sample that company chose to submit. A report naming your lot reference and the date your material was drawn proves the result for the bag you are about to ship.
How thick should hardware plating be?
Between 0.15 and 0.3 µm of gold tone over a 3-5 µm nickel barrier, rising to 0.2-0.4 µm for pale finishes. Palladium is usually specified at 0.20 µm over solid brass, read by XRF and recorded per bath.
What salt spray standard applies to bag hardware?
Neutral salt spray to ISO 9227, run for 24 hours as standard and 48 hours for antique finishes. The result must be tied to the same bath as the thickness reading, or the two numbers describe different components.
How many cycles should a closure survive?
Five thousand open-close cycles, run on the assembled bag rather than on the loose component. Alignment faults appear only when the lock sits on the panel, so a rig test on the component alone misses them.
What pull force should a magnet have?
Between 2.5 and 3.5 kgf when new, retained above 2.0 kgf at 5,000 cycles and tested on the assembled bag. A pair fitted off centre reads as weak to the customer before any real decay has occurred.
Is a decorative component in scope for nickel release?
Usually yes. Prolonged contact is interpreted broadly, so a metal foot and a strap end are both in scope even where the drawing describes them as decorative. Screens are chosen by market and by component.
How is a hardware defect classified at inspection?
A visible cosmetic fault is a major and counts against the AQL 2.5 allowance. A component that can release is critical and accepts none, which is why detachment testing belongs in the pack rather than at the table.
What sample size does AQL 2.5 give on a 500 pc lot?
Fifty pieces at general inspection level II under ISO 2859-1, with three majors allowed. No critical defects are accepted at any level, so a single component that can release stops the shipment.
How long should retained hardware samples be kept?
Twenty-four months, one sealed component per bath, labelled with the bath ID and the date. A photograph cannot settle a dispute about tone, and a component stored under uncontrolled light is little better.
Who is responsible for the chemical test report?
An independent laboratory, not the component maker. The report must name the laboratory, the method, the limit and the result, and it is tied to the lot. A statement missing those four is not a result.
When should the certification file be requested?
At quotation. Every item on the twelve-point list is obtainable before bulk begins and almost none can be produced honestly afterwards, which is why document delivery belongs to sample approval rather than to final payment.
People Also Ask
What certificates are needed for bag hardware?
A substrate or melt certificate, a chemical report covering REACH, Prop 65 and CPSIA, a plating bath log with a thickness reading, and a mechanical record of cycles, pull force and torque, all filed per lot.
How do you prove hardware is REACH compliant?
With a laboratory report naming the method, the limit and the result for nickel release under Annex XVII entry 27, tied to the lot and dated. A general statement from a previous year does not describe the material being shipped.
What is a plating bath log?
A record of each plating run giving the bath ID, the date, the alloy, the thickness reading in micrometres and the salt spray result. It is what lets a finish drift be traced to one bath rather than to a season.
Does CPSIA apply to handbag hardware?
Yes, wherever the line sells into the United States. It limits lead in substrates and coatings, and it is screened per component rather than per bag, so the brief names destination markets at quotation.
What is a critical defect in bag hardware?
Any component that can release: a rivet that spins, a magnet that comes out of its housing, a screw that backs out. It accepts no allowance at inspection, so a single piece stops the shipment.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- European Chemicals AgencyECHA Administrator of REACH, including Annex XVII entry 27 on nickel release from articles in prolonged contact with skin.
- California Office of Environmental Health Hazard AssessmentOEHHA The authority behind California Proposition 65, which governs warning requirements for listed substances in metal components.
- CPSCU.S. Consumer Product Safety Commission Administrator of CPSIA limits on lead in substrates and coatings, screened per component for lines sold in the United States.
- ISO — International Organization for StandardizationISO Publisher of ISO 9227 neutral salt spray testing and ISO 2859-1 sampling procedures used for the AQL 2.5 draw.
- Leather Working GroupLeather Working Group Tannery audit protocol behind the leather that certified hardware is fitted to, since metal and hide are approved as one assembly.