How to Specify Luxury Handbag Hardware in Tech Packs: Five Decisions, Twelve Fields and a Callout That Cannot Be Misread
A tech pack fails at hardware more often than at any other component, because hardware is the only part of a bag that has to be described well enough for someone else to make it from scratch. Five decisions shape the specification: stock, modified or custom; which drawing views; what tolerance scheme; which material and finish callout; and what test data is attached. Behind them sit twelve fields that every hardware sheet needs, from the part number to the sealed reference. This piece walks the five decisions as a tree, sets out the twelve fields in order, gives the plating callout in the standard classification form, and closes with the review to run before the pack is issued, because the pack is the last point at which a change costs nothing.
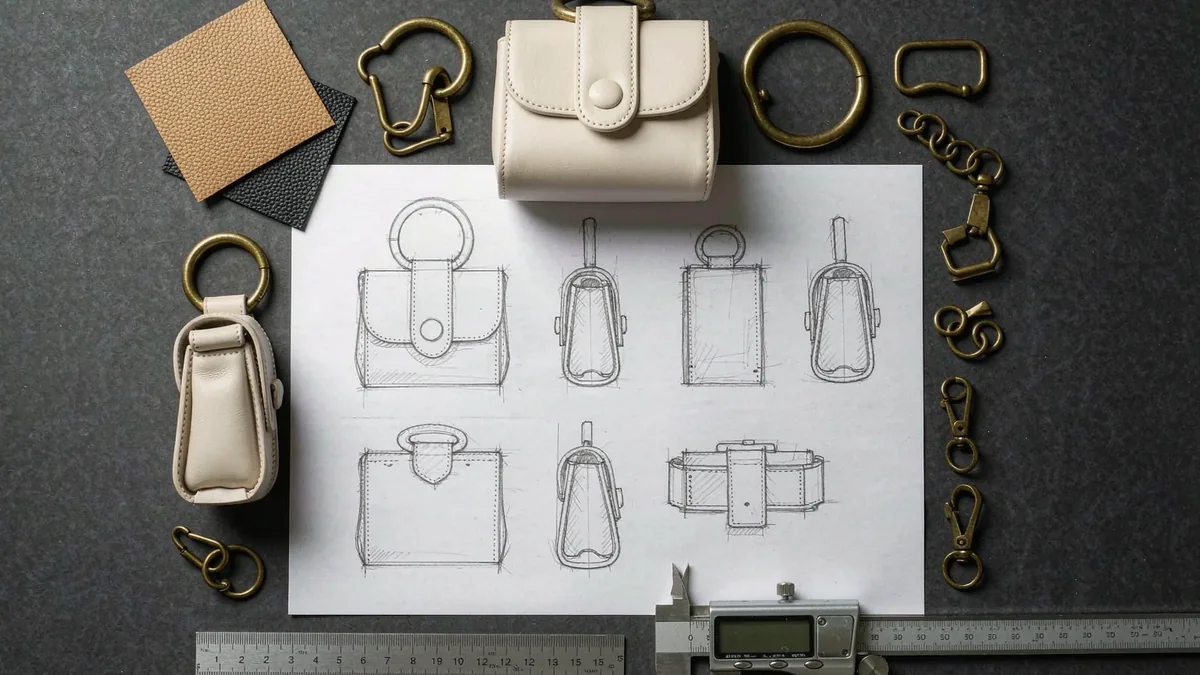
What a Tech Pack Has to Achieve for Hardware
A tech pack has one job for hardware: it must let someone who has never seen the bag produce the fitting correctly, and it must let someone who has never seen the fitting decide whether it is correct.
Those are two different readers. The first needs geometry, material, finish and quantity. The second needs tolerance, test targets and a reference. A pack written for only one of them produces a fitting that can be made but cannot be checked, or checked but not made.
The test of a finished hardware sheet is simple: hand it to someone unfamiliar with the programme and ask them to quote it. If they have to ask a question, the sheet is missing a field.
Decision One: Stock, Modified or Custom?
This decision sets how many of the remaining fields the sheet needs, and getting it wrong is the most common way a pack becomes either bloated or incomplete.
- Stock: the sheet needs a part reference and a finish only. Drawing views are not required, since the form already exists.
- Modified stock: the sheet needs the catalogue part reference, your finish callout and the branding detail. One view, showing where the mark sits.
- Fully custom: the sheet needs everything. All twelve fields, full views, a tolerance scheme and test data.
- The threshold: if the form is the signature of the house, it is custom. If it merely closes the bag, modified stock is usually enough.
- The calendar consequence: custom adds 20-28 days of tooling before sampling can begin, which the pack must state.
The threshold line is worth writing into the pack as a note. It prevents the slow drift by which a stock fitting acquires custom requirements until it is effectively custom without the tooling time being allowed for.
Decision Two: Which Drawing Views?
A fitting drawing is not a product drawing, and the views needed depend on how the part will be made.
- Scale
- 2:1 for a fitting under 40 mm, so the detail is legible on A4
- Projection
- Third angle, stated in the title block rather than assumed
- Units
- Millimetres throughout, with the unit stated once and not repeated
- Minimum views
- Front, side and section for a custom form; front only for modified stock
- Section
- Through the fixing, since the prong length and the hole are what fail
- Datum faces
- Marked on every custom view: three is usually enough
The section through the fixing is the view most often omitted and the one that prevents the most faults. A front elevation shows a lock that looks correct; a section shows whether its prong will reach through the stack.
Decision Three: What Tolerance Scheme?
A tolerance scheme has two levels, and applying one level to every dimension is what makes a sheet either unbuildable or unenforceable.
| Dimension class | Tolerance | How many, typically |
|---|---|---|
| Critical | ±0.08 mm | Two or three per fitting: fixing centres, prong length, engagement faces |
| General machined | ±0.15 mm | Applies to any face cut after casting |
| General cast | ±0.20 mm, or ±0.20 mm per 25 mm on a long dimension | Everything not otherwise marked |
| Angular | ±1 degree | Rotation of a lock cam, or the rake of a foot |
| Mass | ±3 percent of the stated figure | One line, and it catches a hollow or a porosity problem inexpensively |
The mass tolerance is an underused line. A fitting that is 5 percent light is usually a fitting with porosity, and weighing it takes seconds where inspecting for pinholes takes minutes.
Decision Four: Which Material and Finish Callout?
Standard designations replace paragraphs of description, and a callout written in the standard form is unambiguous to anyone who reads one.
- Substrate: Zamak 5 to EN 1774 for a load-bearing die-cast part, or brass CW612N for a machined one.
- Plating: write it in classification order, outermost first, as in Au 0.2 over palladium-nickel 0.7 over Zamak 5.
- Reference the classification standard, ISO 27874 for electrodeposited gold and gold alloy coatings.
- Surface texture: Ra 0.4 µm for a mirror polish, Ra 0.8-1.6 µm for a brushed satin.
- Gloss: 20-40 gloss units at 60 degrees for satin, 70-90 for a mirror, stated alongside the roughness figure.
Writing the plating outermost-first is the part that removes ambiguity. A callout reading 'gold over palladium' can be read two ways; one written Au 0.2 / Pd-Ni 0.7 cannot.
Decision Five: What Test Data Is Attached?
Five documents turn a specification into an enforceable one, and four of them are produced during sampling rather than during bulk.
- Plating thickness record
- Measured on a piece from the production batch, not quoted from a catalogue
- Corrosion report
- Salt spray duration and the rating, with the arrises reported separately
- Chemical declaration
- Naming the finish and the batch, requested with the plating trial
- Functional test record
- Pull and cycle figures recorded at the start and at the end of the test
- Sealed reference record
- The identity and location of the sealed fitting held by both sides
Attach them to the sheet rather than filing them separately. A specification that says where to find the evidence is a specification that gets enforced.
The Twelve Fields of a Hardware Spec Sheet
Twelve fields, in this order, and a sheet is complete. Most incomplete packs are missing the last four.
Twelve fields, in order
- Part number, in a scheme that survives revision: HW-LOCK-001-Rev B, with the revision letter changing every issue.
- Part name and the position on the bag, since one bag can carry two locks.
- Quantity, stated as 500 pcs per style and colourway, with the number of colourways named.
- Route: stock, modified stock or fully custom, with the consequence for the calendar stated.
- Drawing: views, scale, projection and units, with the section through the fixing included.
- Tolerance scheme: critical, general machined, general cast, angular and mass.
- Substrate, by standard designation rather than by description.
- Finish callout, in classification order outermost first, with roughness and gloss figures.
- Colour and tone: the coordinate targets, the tolerance and the illuminants.
- Test targets: thickness, corrosion hours, pull and cycle figures.
- Attachment: hole size, washer, prong length and the reinforcement behind the panel.
- Reference: the sealed fitting, where it is held, and when it was last requalified.
How to Write the Callout So It Cannot Be Misread
Four habits remove most of the ambiguity from a hardware sheet, and none of them adds length.
- Use a standard designation for every material, so nobody has to interpret an adjective.
- Write numbers with their units, always, including on a drawing already stated to be in millimetres.
- Name the standard for every test, so a result from one laboratory can be compared with another.
- Avoid relative words entirely: 'slightly darker' and 'a little tighter' cost more than any figure.
- Write the acceptance condition as a measurable outcome rather than as an instruction to be careful.
The last habit is the one that changes behaviour on the line. 'Fit the lock carefully' produces whatever the operator considers careful; 'engagement torque between 0.15 and 0.35 N·m' produces a checkable result.
How the Spec Sheet Connects to the Rest of the Pack
A hardware sheet is not standalone. Four references tie it to the rest of the pack, and a missing one is how a fitting ends up dimensioned for the wrong stack.
| Reference | Where it comes from | What breaks without it |
|---|---|---|
| Stack thickness at each fitting point | The construction sheet, which lists leather, interlining, foam and board | Prong length is wrong and the fitting spins or tears the panel |
| Panel material and thickness | The materials sheet | The washer size and the reinforcement are guessed |
| Lining specification | The materials sheet | A magnet or a rivet interferes with a lining seam |
| Colour standard | The colour sheet, with the sealed reference | The fitting is correct alone and different on the bag |
Cross-reference by number rather than by description. 'See construction sheet, stack at position 3' survives a revision; 'see the base panel' does not.
Six Mistakes That Recur on Hardware Sheets
The same six omissions appear on most first drafts, and each one produces a specific and predictable fault downstream.
| Mistake | What it produces | The field that fixes it |
|---|---|---|
| No stack thickness at the fitting point | A prong too short or too long, so the fitting spins or tears the panel | A cross-referenced stack figure from the construction sheet |
| Finish described rather than classified | Two parties holding two different ideas of the same adjective | A callout in classification order with a thickness per layer |
| No datum faces marked | A fitting measured three different ways by three people | Two or three datums marked on every custom view |
| Test written as an instruction | A result nobody can check, because nobody defined the outcome | A measurable target with the standard named beside it |
| Sealed reference missing or held in one place | A dispute about memory rather than about a measurement | A reference held in three places, requalified every 12 months |
| Revision rule not stated | A change after tooling argued about instead of priced | One line: changes after tooling cost the die, not the drawing |
Silence is the expensive failure mode on a specification. A wrong figure gets corrected during sampling; a missing one is discovered when the goods are already packed, and by then the question is who pays rather than what is right.
Reviewing a Tech Pack Before Issue
Six questions, asked in one sitting, and the pack is ready to issue.
- Can someone quote it without asking a question? If not, find the missing field.
- Is every critical dimension marked, and are there no more than three of them?
- Is the finish written in classification order, with a thickness figure for each layer?
- Is the stack thickness at every hardware point stated and cross-referenced?
- Are the test targets attached, with the standard named for each?
- Is the revision rule stated, and does it say that changes after tooling cost the die?
The last question is the commercial one. A revision rule written into the pack turns a later change from a disagreement into a line item, and that is worth more than any other field on the sheet.
Our programme runs export experience since 2014 across 7 production lines with about 200,000 pcs per month of capacity, delivered through our validated partner factory Quanzhou Yingming Bags, an SGS-validated site, with inspection at AQL 2.5 (ISO 2859-1) and handover on FOB Xiamen terms.
Have your hardware sheet reviewed before it is issued
Send the drawing, the construction stack and the markets you sell into. We will return the twelve fields completed, the test targets and a piece price at 500 pcs. Request a quote.
Frequently Asked Questions
What should a hardware specification include?
Twelve fields: part number with revision, name and position, quantity, route, drawing with views and scale, tolerance scheme, substrate by standard designation, finish callout, colour coordinates, test targets, attachment detail and the sealed reference.
How many critical dimensions should a fitting drawing have?
Two or three, at ±0.08 mm. Marking eight makes the part unnecessarily expensive and marking none leaves any disagreement unresolvable. General cast dimensions sit at ±0.20 mm and angular ones at ±1 degree.
How should a plating finish be written on a spec sheet?
In classification order, outermost layer first, with a thickness in micrometres for each: Au 0.2 over palladium-nickel 0.7 over Zamak 5. Reference the classification standard, ISO 27874 for electrodeposited gold and gold alloy coatings.
What scale should a hardware drawing be?
2:1 for a fitting under 40 mm, so the detail is legible on an A4 sheet. State third-angle projection and millimetres in the title block rather than leaving either to be assumed.
Should a tech pack include a section view of a fitting?
Yes, through the fixing. A front elevation shows a lock that looks correct; a section shows whether its prong reaches through the full stack of leather, interlining, foam and board, which is what actually fails.
How do I reference the leather stack on a hardware sheet?
By number, not by description: 'see construction sheet, stack at position 3'. A cross-reference by number survives a revision, whereas a reference to 'the base panel' does not, and prong length depends on that figure.
What is a mass tolerance for on a fitting?
It catches porosity inexpensively. State the mass in grams at ±3 percent; a fitting that comes in 5 percent light usually has voids in the casting, and weighing takes seconds where inspecting for pinholes takes minutes.
How should surface texture be specified?
As a roughness figure: Ra 0.4 µm for a mirror polish and Ra 0.8-1.6 µm for a brushed satin, with the gloss figure stated alongside, since the two together describe how the surface reads rather than how it feels.
What test data belongs with a hardware sheet?
Five documents: the plating thickness record measured on the batch, the corrosion report with the arrises rated separately, the chemical declaration naming the finish and batch, the functional test record, and the sealed reference record.
Why does a tech pack fail on hardware more than other parts?
Because hardware is the only component that has to be described well enough for a third party to make it from nothing. Leather is selected from a range and fabric is specified by reference; a fitting has to be built to the drawing alone.
What revision rule should a tech pack state?
That the revision letter changes with every issue, and that any change requested after tooling has started costs the die rather than the drawing. Written into the pack, a later change becomes a line item instead of a disagreement.
Do stock fittings need a full specification sheet?
No. A stock fitting needs a catalogue part reference and a finish callout. Modified stock adds one view showing where the branding sits. A full twelve-field sheet is required for a fully custom form, which also adds 20-28 days of tooling.
People Also Ask
How do I write a tech pack for bag hardware?
Work through twelve fields in order: identity, quantity, route, drawing, tolerance, substrate, finish, colour, tests, attachment and reference. If someone can quote from the sheet without asking a question, it is complete.
What is the most common error in a hardware spec?
Omitting the stack thickness at the fitting point. The drawing is dimensioned from the silhouette rather than from the construction sheet, so the prong is too short once interlining and board are added behind the leather.
Should I specify tolerance on every dimension?
No. Mark two or three critical dimensions at ±0.08 mm and let a general note cover the rest at ±0.20 mm. A drawing where every dimension is critical is a drawing that will be expensive to make and argued about anyway.
How do I describe a finish without ambiguity?
Use standard designations and write layers outermost first with a thickness for each. Replace adjectives with figures: roughness in micrometres Ra, gloss in gloss units, and colour in CIE coordinates with a stated tolerance.
Do I need a drawing for a stock fitting?
Usually not: a catalogue part reference and a finish callout are enough, with one view if branding is added. Reserve full drawing packages for custom forms, where geometry has to be communicated rather than referenced.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- ISO — International Organization for StandardizationISO Publisher of ISO 27874 for electrodeposited gold coatings, ISO 2859-1 sampling and the geometrical tolerancing standards used on drawings.
- ASTM InternationalASTM International Publisher of practices for plating thickness, salt spray and abrasion, referenced when test targets are written onto a specification.
- CENCEN — European Committee for Standardization Publisher of EN 1774 for zinc casting alloys and the copper alloy designations used in substrate callouts.
- ECHA — REACHEuropean Chemicals Agency Administrator of REACH Annex XVII, whose nickel limit is declared against the finish named on the sheet.
- Sourcing JournalSourcing Journal Trade reporting on specification practice, hardware quality and compliance across the accessories industry.