Luxury Handbag Workstation and Method Guide: Nine Stations, Set in Numbers
A luxury handbag workstation is nine stations, each with one accountable measurement: lay, click, skive, assemble, stitch, edge, hardware, finish and inspection. Set the bench at 900-950 mm, light it to 800-1000 lux at 4000 K with a colour rendering index of 90 or above, space the pricking iron at 3.18 mm for eight per inch, and apply edge coats at 60-80 µm wet. Set up in that order and the method follows.
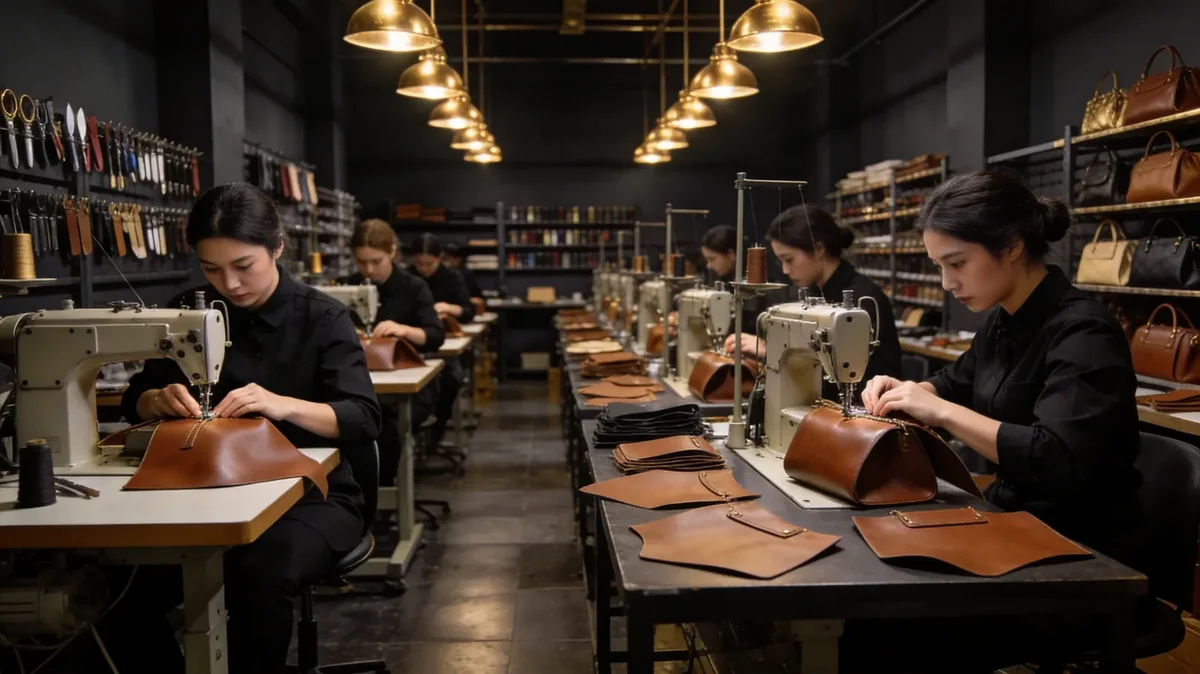
The Nine Stations and What Each One Is Accountable For
Work on a designer piece moves through nine stations, and the discipline of the method is that each station owns exactly one measurement it is accountable for. Lay owns tile and grain direction. Click owns panel dimension. Skive owns thickness at the turn. Assembly owns glue line and open time. Stitch owns pitch. Edge owns film. Hardware owns seating. Finish owns surface. Inspection owns the record.
| Station | Accountable for | Checked with | Tolerance |
|---|---|---|---|
| Lay | Grain direction, tile or defect placement | Chalk map and hide lot tag | 2 mm from the drawn mark |
| Click | Panel dimension against the pattern | Steel rule and pattern | ±0.5 mm on a cut edge |
| Skive | Thickness at the turn | Dial gauge | 0.6-0.7 mm exotic, 0.8 mm calf |
| Assemble | Glue line width and open time | Timer and spreader | 3-5 min open, 8 mm line |
| Stitch | Pitch and distance from the edge | Stitch gauge | 8-9 per inch, 2.5 mm |
| Edge | Dry film after the last coat | Micrometer | 0.10-0.15 mm dry |
| Hardware | Plate seating and closure feel | 0.2 mm feeler | No rock, gap under 0.2 mm |
| Finish | Surface, gloss and handling marks | Reference panel under retail light | No dull patch, no print |
| Inspect | The record of readings | AQL 2.5 plan sheet | Readings, not verdicts |
Bench, Height and Board: Setting the Physical Station
The bench is set from the maker, not from a catalogue. Height is taken as elbow height minus roughly 50 mm, which lands most makers between 900 and 950 mm for seated stitching work and 850-900 mm for edge work that is done standing. The top is 40 mm beech or maple, unfinished, because a finished top reflects light into the eye and a soft top will not hold a pricking iron.
- Bench at 900-950 mm seated, 850-900 mm standing, taken from elbow height minus 50 mm.
- A 40 mm unfinished hardwood top, so it holds a strike and does not glare.
- A glass board of 8 mm for skiving and clicking, with the edge rounded and polished.
- A leather-covered pad at the stitch station so the shell is not marked by the bench.
- Footrest and seat at a height that puts the maker's forearm level with the board.
The glass board is often treated as a consumable and should not be. An 8 mm board with a polished edge is what allows a skiving knife to take a clean 8-10 mm bevel rather than a ragged one, and a scratched board telegraphs its scratches through a gloss panel under retail light.
Light, Colour Temperature and Why 800 Lux Is the Floor
Lighting is the least costly station upgrade and the one most often skipped. Work at 800-1000 lux measured at the board, at 4000 K, with a colour rendering index of 90 or above, positioned so the light comes over the maker's opposite shoulder to avoid a shadow under the hand. Below about 500 lux the eye cannot resolve a 0.5 mm seam deviation, which means the station is producing work it cannot check.
- Illuminance at the board
- 800-1000 lux
- Colour temperature
- 4000 K, neutral
- Colour rendering index
- 90 or above
- Light direction
- Over the opposite shoulder, no hand shadow
- Second source
- Retail-type spot at 3000 K for a final look
- Room temperature
- 20-22 degrees
- Relative humidity
- 45-55 per cent
- Bench surface reflectance
- Low, unfinished timber or grey
The second source matters more than it appears to. A piece approved only under neutral light can read differently under the 3000 K spot used in a boutique, particularly on a dyed shell where the dye has a blue undertone. Checking the first piece of a run under both is a two-minute step that prevents a colour dispute after delivery.
Hand Tools: Awl, Pricking Iron, Knife and Slicker
Four tools carry most of the work, and each has a specification rather than a brand. The pricking iron is spaced to the pitch: 3.18 mm for eight per inch, 2.82 mm for nine, with the teeth kept sharp because a blunt tooth tears the grain side. The awl blade is 1.2 mm and is replaced rather than re-ground once it has lost its point, because a dulled blade pushes the fibres apart instead of parting them.
Pricking iron
Spaced to pitch at 3.18 mm for eight per inch or 2.82 mm for nine. Teeth are kept sharp and the tool is held vertical, because a leaning iron produces a slant that flips along the run.
Awl
A 1.2 mm blade, replaced rather than re-ground. A dull blade parts fibres by pressure rather than by cutting, which is what leaves a seam that looks raised rather than drawn.
Skiving knife
Ground to a 20-25 degree bevel and stropped at the start of every shift. The bevel, not the pressure, is what sets the 8-10 mm width of the turn.
Slicker and folder
Boxwood or bone, worked warm at 60-70 degrees on an edge, used to close a turned fold before any adhesive is applied.
What the four have in common is that each is maintained to a specification rather than replaced when it fails. A station that strops its knife at the start of a shift produces a consistent bevel; one that does not produces a bevel that varies with the sharpness of the blade, which is the sort of variation that shows up as inconsistency across 500 pieces. The bench discipline behind this is described on the craftsmanship page.
Adhesives, Open Time and Press Settings
Assembly is the station where a method failure is hardest to see, because a bad glue line is invisible until it fails. A water-based adhesive at 45-50 per cent solids is applied in an 8 mm line, left open 3-5 minutes until it is touch-dry rather than wet, and pressed at 3-4 bar for 8 seconds. Too little open time traps solvent and the bond creeps; too much and the bond has already begun to set before the panels meet.
- Apply an 8 mm line, not a puddle; squeeze-out at the edge is a sign of over-application.
- Wait 3-5 minutes to touch-dry, checked by finger rather than by clock alone.
- Press at 3-4 bar for 8 seconds, with the pressure taken across the whole panel.
- Leave the assembly 30 minutes before any stitch is run through it.
- Record the adhesive batch against the order, so a failure can be traced to a lot.
The batch record is the item most stations skip and the one that pays for itself the first time a bond fails. Adhesive performance drifts with age and storage temperature, and without a batch against the order there is no way to tell whether a failure was the adhesive, the open time or the press setting.
Edge Station: Coats, Viscosity and Cure
Edge work is three coats, applied at 60-80 µm wet each, with 10-12 minutes of flash-off at 60 degrees between coats and a light pass at 400 grit before the second and third. The dry film that results measures 0.10-0.15 mm, and the test is tactile: run a nail from panel to edge and there should be no ridge at the coat boundary. A line that reads as a strip stuck onto the edge means the film is above about 0.25 mm.
Two station rules keep it consistent. First, the coat is applied to a panel that is flat and supported, never held in the hand, because the hand flexes the edge and the film cures with the flex in it. Second, cure is measured in hours before the piece is packed, not in the time it takes to look dry, because a film that is dry to the touch will still take a print from a packing surface.
Hardware Station: Setting, Seating and the Feel Check
Hardware is set with the panel supported on a block that matches the shape of the piece, so the force goes into the setting and not into the shell. Seating is checked with a 0.2 mm feeler: no gap larger than that between plate and panel, and no rock when the piece is set down. The closure is then worked ten times and the resistance recorded as a description, because feel is the one specification on a luxury piece that cannot be read off a gauge.
One-Piece Flow or Batch: Choosing the Method
Two methods are available and the choice depends on the piece. One-piece flow takes a single unit through all nine stations before the next is started, which suits a complex or exotic build where a mistake is expensive and the sample has to be matched piece by piece. Batch moves a group through each station in turn, which suits a simpler build at 500 pieces where repetition is the point.
| Factor | One-piece flow | Batch |
|---|---|---|
| Best for | Complex or exotic builds, first drops | Repeat colourways of an established style |
| Detection speed | A fault is found at the next station | A fault is found at inspection |
| Bench minutes per piece | Higher, 10-15 per cent more | Lower, repetition shortens each step |
| Consistency risk | Low, each piece is compared to the last | Higher, drift within a group |
| Suits a run of | Under 300 pieces per style | 500 pcs per style and colourway |
Most programmes use both. The first drop runs one-piece flow until the method is settled and the tolerances are confirmed, then the repeat colourways run in batch with a piece from each group pulled and checked against the approved sample. That hybrid is what allows a 500-piece run to be consistent without paying one-piece bench time on every unit.
Station-by-Station Checks Before a Piece Moves On
- Lay: is the panel within 2 mm of the drawn mark, and is the lot tag recorded?
- Click: does the panel measure within ±0.5 mm against the pattern?
- Skive: does the dial gauge read 0.6-0.7 mm on exotic or 0.8 mm on calf at the turn?
- Assemble: was the line 8 mm, the open time 3-5 minutes, and the press 8 seconds at 3-4 bar?
- Stitch: does the gauge read 8-9 per inch, and is the topstitch 2.5 mm from the edge?
- Edge: does the micrometer read 0.10-0.15 mm dry, and is there no ridge under a nail?
- Hardware: does a 0.2 mm feeler pass anywhere between plate and panel?
- Finish: under both light sources, is there any dull patch or print?
- Inspect: are the readings recorded against the order rather than a verdict?
Nine questions, roughly twenty minutes, and the whole method in one list. The point of putting the check at the station rather than at the end is that a fault found at the next station is corrected on one piece, while the same fault found at inspection is corrected on whatever portion of the run has already passed through.
Setting a Station Up Before Sampling Starts
The programme runs through our validated partner factory Quanzhou Yingming Bags, an SGS-validated site with 7 production lines and about 200,000 pcs per month of capacity, holding export experience since 2014. Sampling takes 6-10 working days on a standard build and 12-15 on a complex one, bulk occupies 35-50 days, minimums sit at 500 pcs per style and colourway, and shipments leave FOB Xiamen with FOB, CIF and DDP terms available. Inspection is drawn at AQL 2.5 under ISO 2859-1.
Material behind the stations is tested against ISO 3376 for tensile strength, ISO 11644 for finish adhesion and ISO 105 for colour fastness, with hide traceability evidenced through Leather Working Group tannery audits. Setting the nine stations up to the figures above, rather than to an ordinary tolerance, adds roughly USD 4.80 per unit, and it is worth paying on the seams and edges a hand finds rather than on the interior.
Station set-up checklist
- Bench 900-950 mm seated; 800-1000 lux at 4000 K with a rendering index of 90 or above; room at 20-22 degrees and 45-55 per cent humidity; pricking iron 3.18 mm; awl blade 1.2 mm; knife bevel 20-25 degrees; glue line 8 mm, open 3-5 min, press 3-4 bar for 8 s; edge 60-80 µm wet per coat and 0.10-0.15 mm dry; hardware gap under 0.2 mm.
Have your method reviewed station by station
Send drawings, material direction, quantity per colourway and delivery date. You will receive a station set-up sheet naming the tolerance and check at each of the nine. Request a quote.
Frequently Asked Questions
What are the stations in a luxury handbag workshop?
Nine: lay, click, skive, assemble, stitch, edge, hardware, finish and inspection. Each is accountable for one measurement, checked before the piece moves on, so a fault is found at the next station rather than at the end of the run.
How high should a leather working bench be?
Elbow height minus roughly 50 mm, which lands most makers at 900-950 mm for seated stitching and 850-900 mm for edge work done standing. The test is that the forearm sits level with the board without the shoulder rising.
How much light is needed at the bench?
800 to 1000 lux measured at the board, at 4000 K, with a colour rendering index of 90 or above. Below about 500 lux the eye cannot resolve a 0.5 mm seam deviation, so the station produces work it cannot check.
Why is a second light source recommended?
Because a piece approved only under neutral light can read differently under a 3000 K boutique spot, especially on a dyed shell with a blue undertone. Checking the first piece under both takes two minutes and prevents a colour dispute after delivery.
What spacing should a pricking iron have?
3.18 mm for eight stitches per inch and 2.82 mm for nine. The iron is held vertical, because a leaning iron produces a slant that flips part-way along a run, which is the inconsistency an eye notices first.
When should an awl blade be replaced?
Once it has lost its point, rather than being re-ground. A 1.2 mm blade that has dulled parts the fibres by pressure instead of cutting them, and the seam then reads as raised rather than drawn into the panel.
What are the correct adhesive settings?
A water-based adhesive at 45-50 per cent solids, applied in an 8 mm line, left open 3-5 minutes to touch-dry and pressed at 3-4 bar for 8 seconds. Too little open time traps solvent and the bond creeps.
How thick should each edge coat be?
60-80 µm wet per coat, over three coats, drying to 0.10-0.15 mm. Between coats there are 10-12 minutes of flash-off at 60 degrees and a light pass at 400 grit. Above about 0.25 mm the edge reads as a stuck-on strip.
How is hardware seating checked?
With a 0.2 mm feeler at the plate, and by setting the piece down to feel for rock. The closure is worked ten times and the resistance described in writing, because feel is the one specification that cannot be read off a gauge.
Should a run use one-piece flow or batch?
One-piece flow for a complex or exotic first drop, where a mistake is expensive and the sample has to be matched piece by piece; batch for repeat colourways at 500 pcs where repetition is the point. Most programmes use both.
How long does it take to set nine stations up?
The physical set-up is a day or two, but the tolerances are agreed during sampling, which runs 6-10 working days on a standard build and 12-15 on a complex one, counted from an approved tech pack rather than from an enquiry.
What does setting the stations to luxury tolerances cost?
Roughly USD 4.80 per unit above an ordinary tolerance, concentrated in edge work, hardware seating and stitch consistency. It is worth paying on visible and loaded areas and not worth paying uniformly across the interior.
People Also Ask
Why give each station only one measurement?
Because accountability with one number is enforceable. A station that owns pitch, edge and seating owns nothing measurable, and a fault then travels to inspection instead of being caught at the next bench.
Can a bench be too low?
Yes. Below the elbow-minus-50 mm target the maker leans in, the pricking iron is held off vertical, and the slant of the stitch changes along the run, which reads as inconsistency across the drop.
Is 4000 K the only acceptable colour temperature?
It is the working standard because it renders dyed shells neutrally. Some benches add a 3000 K source for a final look so a piece approved at the bench matches what a boutique light will show.
How long should an assembly rest before stitching?
About 30 minutes after pressing. Stitching into a bond that has not begun to set drags the panels and produces a seam that sits off the line it was placed on.
What is the fastest station upgrade?
Lighting. Raising the board from 400 to 800-1000 lux costs very little and immediately makes a 0.5 mm seam deviation visible to the maker who is producing it.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- ISO - International Organization for StandardizationISO Publisher of ISO 2859-1 for the inspection plan, ISO 3376 for tensile strength, ISO 11644 for finish adhesion and ISO 105 for colour fastness.
- SATRA Technology CentreSATRA Independent testing body for leather goods, referenced for abrasion, flex and finish adhesion methods used at the edge and hardware stations.
- Leather Working GroupLeather Working Group Tannery audit protocol through which hide traceability behind the lay station is evidenced.
- European Chemicals AgencyECHA Administrator of REACH, whose Annex XVII restrictions govern the adhesives, finishes and dyes used at the assembly and edge stations.