How Premium Handbag Craftsmanship Holds Value: Three Build Tiers Compared
Premium handbag craftsmanship holds value through four things that survive a decade: three edge coats at 0.10-0.14 mm, solid brass hardware at 28-34 g with plating at 0.15-0.3 µm, waxed linen thread at 0.45-0.55 mm, and reinforcement that reaches the stitch line. Where all four are present a piece typically retains 60-70% of its value; where two are present, 40-55%; where none are, 20-35%.
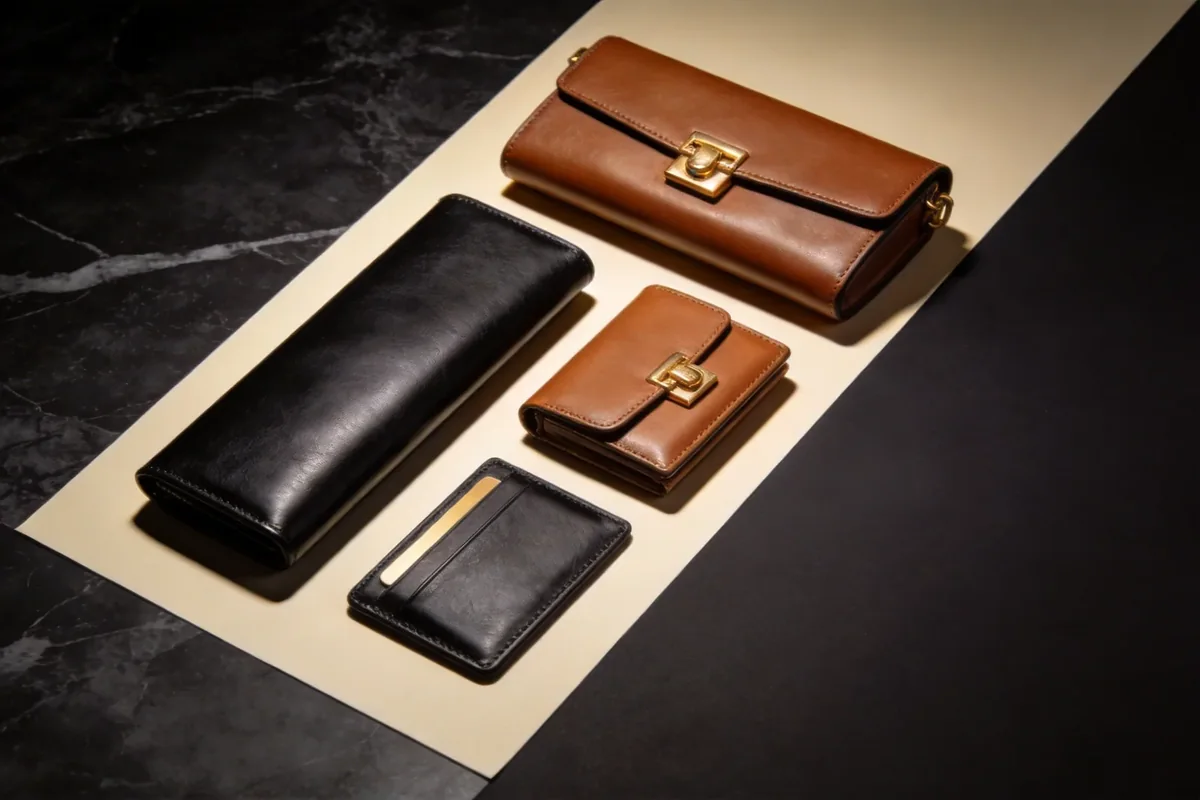
Three Build Tiers, Compared on What Survives
Value retention on the secondary market is not a function of the name on the piece so much as a function of what is still intact when the piece arrives for resale. Three build tiers describe almost everything on the market, and the differences between them are measurable rather than matters of opinion: how many edge coats were applied, whether the hardware is solid or cast, whether the thread is waxed linen or bonded filament, and whether the reinforcement reaches the stitch line.
What separates the tiers is not what looks better on day one — a well-finished piece from any tier photographs well — but what has failed by year five. Edge cracking, plating bloom, thread lift and handle drop are the four faults that decide a resale price, and all four are decided on the bench rather than in the market.
| Attribute | Top tier | Middle tier | Entry tier |
|---|---|---|---|
| Edge build | Three coats at 0.10-0.14 mm, sanded | Two coats | One thick coat |
| Flex cycles survived | 20 or more | 8-12 | Under 10 |
| Hardware | Solid brass, 28-34 g | Brass-plated alloy | Cast alloy, 11-14 g |
| Plating thickness | 0.15-0.3 µm over nickel | 0.10-0.15 µm | Under 0.10 µm |
| Thread | Waxed linen, 0.45-0.55 mm | Bonded filament | Bonded filament, light |
| Reinforcement | Reaches the stitch line | Stops 3-5 mm short | Absent or partial |
| Typical retention | 60-70% | 40-55% | 20-35% |
Edge Build: The First Thing a Resale Buyer Inspects
Anyone assessing a pre-owned piece looks at the edges first, because the edge is where the build cannot be hidden. Three coats at 0.10-0.14 mm wet, sanded at 400 then 800 grit between the second and third, produce a contour that is flush to slightly convex and survives twenty flex cycles at the fold. A single thick coat produces a rounded bead that cracks within ten, and once it has cracked the piece is graded down before any other attribute is considered.
- Coats
- Three, at 0.10-0.14 mm wet
- Sanding between coats
- 400 grit, then 800 grit
- Flex cycles survived
- 20 or more at the fold
- Contour
- Flush to slightly convex, never proud
- Repairability
- A three-coat edge can be re-finished; a cracked one needs rebuilding
- Retention effect
- The largest single driver among the four attributes
Repairability is the part that resale markets price and buyers rarely consider. A three-coat edge that has dulled can be refinished by a restoration specialist in an afternoon; an edge that has cracked through to the fibre has to be rebuilt, and the rebuild is visible. That difference alone moves a piece between grades, which is why the fourth coat of patience on the bench is worth more than any other single minute spent on the body.
Hardware: Mass, Plating and the Bloom Test
Hardware is the second attribute, and it is assessed by mass and by bloom. A 32 mm turn-lock in solid brass weighs 28-34 g and holds a warm colour at the contact points; the same silhouette in cast alloy weighs 11-14 g and, if the plating is under 0.10 µm, shows the base metal as a grey bloom on the raised edges within a season. A bloom cannot be polished out, because polishing removes what remains of the coating rather than restoring it.
Mass
Solid brass at 28-34 g for a 32 mm closure against 11-14 g in cast alloy. Mass is the first thing a hand reads and the first thing a resale buyer comments on, and it is invisible in a photograph.
Plating
0.15-0.3 µm of gold over a nickel barrier, evidenced by a 24-hour salt spray report. Below 0.10 µm the high points wear through and the bloom that follows cannot be reversed by polishing.
Fixings
Screws seated flush with no cam-out mark, checked on every fixing. A chewed screw head tells a resale buyer that the piece has been opened, which raises a question nobody can then answer.
Seam and Thread: What Ten Years Does to a Stitch
Thread choice determines whether a seam is still where it was put after a decade. Waxed linen at 0.45-0.55 mm, drawn through an awl-opened slit at 7-8 stitches per inch, grips the fibre and holds position; bonded filament at about 0.30 mm runs through a tension disc and is more uniform on the day but lifts sooner. Under-drawn thread is the visible failure: it stands proud of the surface and a fingernail catches it, which is exactly the test a resale buyer runs without thinking about it.
- Waxed linen at 0.45-0.55 mm for hand work; bonded filament at about 0.30 mm for machine work.
- Pitch at 7-8 per inch on heavy gauge, with no more than one stitch of spread across three points.
- Thread sitting 0.1-0.2 mm below the surface, so a fingernail passes over it without catching.
- Back-stitch of three at the finish, buried rather than clipped, at every visible seam end.
Reinforcement and the Load Path
Reinforcement is the attribute that decides whether a piece has structurally survived rather than cosmetically. Follow the load from the handle join through the reinforcement to the body seam and the base board: at each junction, the reinforcement should reach the stitch line rather than stop 3-5 mm short of it. Where it stops short, the handle drops under sustained load, and a dropped handle is the fault that takes a piece out of the resale market altogether rather than down a grade.
A dropped handle is not a grading question. Reinforcement stopping short of the stitch line lets the handle drop within a season, and a piece with a dropped handle is generally not offered at all.
There is a fourth interior detail, and it is the one that separates a piece that has been looked after from one that has merely been used: whether the body still holds its shape when empty. That is a function of gauge and base reinforcement rather than of the lining, but it is read through the lining, because a softened base shows first as a crease in the interior floor of the piece. Specifying a face gauge of 1.4-1.6 mm and a base board at 0.8 mm is what protects it, and both are decisions taken long before the interior is fitted.
Lining and Interior: Where Value Leaks Quietly
The interior is where value leaks without anybody naming it. Pocket bags anchored at one end rather than both drop their contents into the body and stretch the lining permanently; a seam allowance left untrimmed at 10 mm prints through the lining and reads as a fault; and a lining cut without shrinkage allowance pulls at the seams after cleaning. None of these are visible in a listing photograph, and all of them are found by whoever inspects the piece in person.
Two further interior details are worth specifying because they cost little at build and return a great deal at resale. A dust bag that fits, and a card stating the material and the care, both of which turn up with the piece years later and signal that it was looked after. Neither touches the silhouette and both move a buyer's confidence more than any single exterior attribute below the top tier.
One more attribute deserves a place on the list because it is routinely left out of briefs and routinely priced by the market: whether the piece can be repaired at all. A bag built with standard hardware sizes, a conventional edge construction and accessible seams can be restored by a specialist anywhere. One built with a bespoke closure, a bonded-only assembly and a lining sealed to the body cannot, and a piece that cannot be repaired is priced accordingly regardless of how well it was made in the first place.
What a Photograph Cannot Show
Everything above has one thing in common: none of it photographs. A listing shows silhouette, colour and condition of the visible faces. It cannot show coat count, hardware mass, thread position or reinforcement reach, which is precisely why those four decide the price once the piece is in someone's hands. A brand building for retention should therefore specify the invisible attributes rather than the photogenic ones, which is the opposite of how most briefs are written.
The corollary for a brand is uncomfortable but worth stating: the attributes that hold value are also the attributes that cost the most per unit, and none of them are visible at launch. Three edge coats rather than one, brass rather than alloy, linen rather than filament, and reinforcement taken all the way to the stitch line together add about USD 4.80 per unit. That figure is the distance between the top tier and the middle one, and it is paid once at build and recovered years later at resale — by the customer rather than by the brand, which is precisely why it is so often the first thing cut from a brief.
How to Buy for Retention
Buying for retention means specifying four attributes with numbers and then inspecting them at goods-in. Three edge coats at 0.10-0.14 mm passing twenty flex cycles; hardware at 28-34 g with plating at 0.15-0.3 µm evidenced by a 24-hour salt spray report; waxed linen at 0.45-0.55 mm at 7-8 per inch with thread 0.1-0.2 mm below the surface; and reinforcement reaching the stitch line at every loaded join. Written that way, retention is a specification rather than a hope.
- Specify coat count and thickness, not 'finished edges'.
- Specify hardware mass and plating thickness, not 'solid brass'.
- Specify thread material and diameter, not 'strong thread'.
- Specify reinforcement reach, not 'reinforced handles'.
- Inspect all four at goods-in on a sample drawn at AQL 2.5.
Retention in one line
- Specify the four attributes that do not photograph: coat build, hardware mass and plating, thread, and reinforcement reach. Those are what a resale buyer inspects.
Programme Figures
Our programme runs through our validated partner factory Quanzhou Yingming Bags, an SGS-validated site with 7 production lines and roughly 200,000 pcs per month of capacity, holding export experience since 2014. Sampling takes 6-10 working days, or 12-15 on a complex build; bulk occupies 35-50 days; minimums sit at 500 pcs per style and colourway; and shipments leave FOB Xiamen with FOB, CIF and DDP terms all available. Inspection is drawn at AQL 2.5 under ISO 2859-1, with finish adhesion tested against ISO 11644 and leather against ISO 3376. Material selection is covered on luxury materials.
Build for what the piece is worth in year five
Send the silhouette, hardware direction, quantity per colourway and the attributes you care about. You will receive a specification naming all four retention attributes with numbers. Request a quote.
Frequently Asked Questions
How does premium handbag craftsmanship hold value?
Through four attributes that survive a decade: three edge coats at 0.10-0.14 mm, solid brass hardware at 28-34 g with plating at 0.15-0.3 µm, waxed linen thread at 0.45-0.55 mm, and reinforcement reaching the stitch line. Where all four are present a piece typically retains 60-70%.
Why does edge build matter so much to resale?
Because the edge is where the build cannot be hidden. Three coats sanded between passes survive twenty flex cycles and can be refinished later; a single thick coat cracks within ten and has to be rebuilt, and the rebuild is visible to anyone inspecting the piece.
What hardware specification holds value?
Solid brass at 28-34 g for a 32 mm closure, with gold plating at 0.15-0.3 µm over a nickel barrier, evidenced by a 24-hour salt spray report. Below 0.10 µm the raised points bloom grey, and polishing cannot restore what has worn through.
Which thread lasts longest on a handbag?
Waxed linen at 0.45-0.55 mm, drawn through an awl-opened slit at 7-8 stitches per inch. It grips the fibre and holds position. Bonded filament at about 0.30 mm is more uniform on the day but tends to lift sooner under flex.
Why does reinforcement reach matter?
Because that is where load transfers from the handle to the body. Reinforcement stopping 3-5 mm short of the stitch line lets the handle drop within a season, and a dropped handle generally removes a piece from the resale market rather than downgrading it.
What interior faults reduce value quietly?
Pocket bags anchored at one end rather than both, an untrimmed allowance printing through the lining, and a lining cut without shrinkage allowance that pulls after cleaning. None show in a listing photograph and all are found in person.
What is the typical retention for each build tier?
Around 60-70% where all four attributes are present, 40-55% where roughly two are, and 20-35% where none are. The spread is driven by what has failed by year five rather than by the name on the piece.
Why do photographs fail to show quality?
Because a listing shows silhouette, colour and the condition of visible faces. It cannot show coat count, hardware mass, thread position or reinforcement reach, which is precisely why those four decide the price once the piece is handled.
Can an edge that has cracked be restored?
Not invisibly. A three-coat edge that has dulled can be refinished in an afternoon; one cracked through to the fibre has to be rebuilt, and the rebuild reads as a repair. That difference alone moves a piece between grades.
How should a brand brief for retention?
By specifying the four invisible attributes with numbers rather than the photogenic ones: coat count and thickness, hardware mass and plating thickness, thread material and diameter, and reinforcement reach. Then inspect all four at goods-in.
What does a chewed screw head signal?
That the piece has been opened at some point, which raises a question a seller cannot then answer. Screws should be seated flush with no cam-out mark, and the torque check should cover every fixing rather than a sample.
How long does sampling and bulk take?
Sampling takes 6-10 working days, or 12-15 on a complex build, and bulk occupies 35-50 days at 500 pcs per style and colourway. Shipments leave FOB Xiamen, with FOB, CIF and DDP terms all available.
People Also Ask
Does brand name matter more than build for resale?
Less than most buyers assume. Within a tier, condition decides the price, and condition at year five is decided by coat build, hardware plating, thread and reinforcement reach rather than by the name.
What is the single biggest driver of retention?
Edge build. It is the first thing inspected, the most visible failure, and the one attribute where a repair is either invisible or obvious with nothing in between.
Should a brand specify hardware mass in grams?
Yes. Writing 28-34 g for a 32 mm closure makes the attribute inspectable. Writing 'solid brass' leaves the door open to a cast part with a brass-coloured coating that blooms in a season.
How do you assess a piece's build in a shop?
Run a fingernail along the seam to feel for proud thread, look at the high points of the hardware for grey bloom, flex the fold gently to check the edge, and lift the piece by the handle to feel the mass.
Is it worth paying more for invisible attributes?
Yes, if retention matters. The four attributes that do not photograph are the four a resale buyer inspects, so money spent on photogenic details returns less than money spent on the build.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- Business of FashionBusiness of Fashion Trade coverage of the secondary market for luxury goods, including how condition and build affect resale pricing.
- FashionUnitedFashionUnited Industry data and reporting on luxury pricing, materials and the resale market.
- ISO — International Organization for StandardizationISO Publisher of ISO 2859-1 for the AQL 2.5 inspection plan, ISO 11644 for finish adhesion and ISO 3376 for tensile strength.
- SATRA Technology CentreSATRA Independent testing body for leather goods, referenced for flex, plating durability and seam strength test methods.