How Luxury Handbag Hardware Is Plated and Polished: The Stack, the Grit Sequence and the Four Tests That Decide It
How is luxury handbag hardware plated and polished? In one fixed order: pick the base metal, build a copper strike and a nickel barrier of 1.5-2.5 µm, lay the decorative metal at 0.15-0.3 µm for gold tone, then polish through descending grit from 220 to 800 before buffing. A finish is proved rather than asserted — by X-ray fluorescence thickness reading under ISO 3497, a 24-hour neutral salt spray floor under ISO 9227, and an adhesion check after thermal shock. On a programme run at MOQ 500 pcs per style and colourway, that stack is written into the technical pack before sampling, because the same gold reads differently over brass than over zinc alloy.
Where the Plating Decision Starts: Choosing the Base Metal
Every plating decision begins with the base metal, because each layer above it inherits its porosity, its flatness and its preparation cost. Choosing the substrate first prevents the common error of specifying a beautiful finish on a casting too porous to hold it.
Three substrates cover almost every bag component: milled or extruded brass, die-cast zinc alloy, and stainless steel for the small share of parts that must never take colour. Brass takes the finest polish and the tightest thread; zinc alloy holds intricate relief at lower weight and lower tool complexity; stainless is chosen for feet and hidden reinforcements. Each asks for a different pre-treatment, and the pre-treatment is where most finish failures are actually decided.
| Base metal | What it suits | How it behaves in plating | Watch for |
|---|---|---|---|
| Milled or drawn brass | Turn-locks, feet, strap ends, any threaded part | Polishes to a mirror, holds tolerances to roughly ±0.05 mm, takes gold directly over a nickel barrier | Heavier, and slower to produce at around 20-25 working days |
| Die-cast zinc alloy | Logo bars, decorative plates, magnetic housings | Fills intricate relief well; needs a heavier copper strike to bridge casting porosity | Micro-porosity causes plating blisters if the strike stage is shortened |
| Stainless steel | Base feet, internal frames, reinforcement stays | Usually left natural or PVD-coated; electroplating needs an activation step | Colour matching against plated brass parts is difficult and often visible |
Note the tolerance column before anything else. A turn-lock cam that is 0.10 mm out of round will feel stiff or mushy in the hand no matter how well it is plated, and that dimension is set by the substrate and the machining, not by the finish.
How the Plating Stack Is Built, Layer by Layer
A decorative finish is a stack, not a coat: the part is cleaned and activated, then carries a copper strike to level the surface, then a nickel barrier to stop migration, then the decorative metal, and only then any antique darkening or lacquer. Skipping a layer saves time at the bath and costs far more at inspection.
- Cleaning and activation: ultrasonic degrease followed by an acid dip, so the surface is chemically live and water-break free.
- Copper strike, roughly 1.0-2.0 µm: levels micro-porosity on castings and gives the nickel something flat to sit on.
- Nickel barrier, 1.5-2.5 µm: this is the layer that actually stops the substrate migrating into the decorative metal.
- Decorative metal: gold tone at 0.15-0.3 µm, rose at 0.2-0.35 µm because the copper in the alloy tarnishes faster.
- Optional antique pass: a darkening chemical wiped into recesses and relieved on the high points by hand.
- Protective lacquer on request: a thin cathodic or solvent lacquer that slows tarnish but can itself abrade at contact points.
- Cleaning
- Ultrasonic degrease at 50-60 °C, then acid activation; water-break test before loading
- Copper strike
- 1.0-2.0 µm, heavier toward the top of the range on die-cast zinc
- Nickel barrier
- 1.5-2.5 µm; below 1.0 µm, copper migration discolours gold tone within a season
- Palladium or palladium-nickel alternative
- 0.1-0.3 µm where a nickel-free claim needs to be supported by EN 1811 release testing
- Gold tone decorative layer
- 0.15-0.3 µm; anything thinner wears through at the cam and high points first
- Rose tone decorative layer
- 0.2-0.35 µm, then lacquered if the brand will accept the added abrasion risk
- Chrome or palladium tone
- 0.2-0.4 µm over the same nickel barrier, with no copper read-through tolerable
The barrier is the layer buyers omit most often and regret longest. Gold laid directly over brass without nickel will drift in colour as copper diffuses upward, and the drift shows first on parts customers touch, since skin and handling accelerate it.
Which Plating Thickness Belongs in Your Technical Pack
Thickness is specified per contact class rather than per collection: a part that slides against leather every time the bag opens needs two to four times the deposit of a decorative plate that nobody touches. Writing a single house figure and applying it to every component is the most common cause of premature wear-through.
High-contact parts
Turn-lock cams, dog clips, feet and strap sliders. Specify 0.3-0.5 µm gold over a 2.0-2.5 µm nickel barrier, and accept that these are the components most worth paying for.
Medium-contact parts
Handle anchors, magnetic housings, zip pullers. Around 0.2-0.3 µm over 1.5-2.0 µm of nickel reads well and survives daily handling.
Low-contact decoration
Logo bars, back plates, internal plates. 0.15-0.2 µm is defensible here because nothing rubs against them in normal use.
Hidden structural parts
Internal stays, reinforcement plates, feet that face the floor. Natural brass or stainless with no decorative deposit is often the honest answer.
Thickness is verified rather than assumed. X-ray fluorescence measurement to ISO 3497 reads the actual deposit on the actual part in seconds, and a buying plan should require it recorded per batch, not once per tool.
How Polishing Actually Changes the Surface
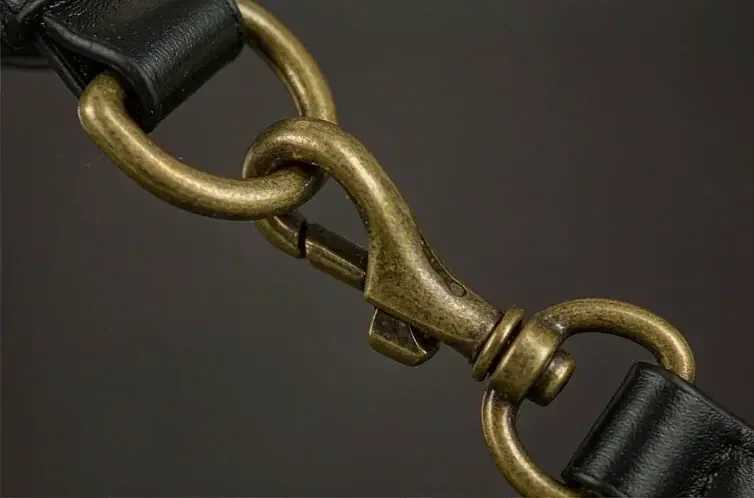
Polishing removes material in a descending sequence of abrasives; it does not add shine. The rule is that each grit must fully erase the scratch pattern of the previous one, and any stage skipped leaves lines that reappear the moment the plating brightens the surface.
- Pre-grind at 180-220 grit to remove gate marks, parting lines and die marks from castings.
- Cut at 320-400 grit until every previous scratch is gone under raking light rather than overhead light.
- Fine at 600-800 grit for finishes that will be bright plated; lower grits are left visible under a satin or brushed requirement.
- Buff with a cutting compound such as tripoli on a cotton wheel to bring colour up without rounding edges.
- Colour with a fine rouge or jeweller's compound for mirror parts, using light pressure so relief edges stay sharp.
- Deburr and inspect under 10x magnification before loading, because plating magnifies rather than hides defects.
There is a genuine tension here worth naming. Aggressive cutting rounds the crisp edge of a logo relief, so a deeply coined plate loses definition if it is buffed to a mirror. The specification has to say which matters more: edge definition or reflectivity.
Rack Plating or Barrel Plating: Which Route Fits Your Part
Rack plating mounts each part individually on a jig and holds it through every stage; barrel plating tumbles loose parts in a rotating barrel. Rack is slower and more expensive per piece and is the only realistic route for visible hardware, because barrel contact leaves marks where parts touch each other.
Choosing the route
- Rack plating for every visible part, every corner that will be seen, and anything with a critical dimension.
- Barrel plating only for genuinely hidden small components such as rivets and washers.
- Check that the rack contact point is allowed to be unplated, or specify a secondary contact that moves mid-cycle.
- For threaded parts, confirm whether the thread must be masked, since deposit builds in the root and changes fit.
- Ask how many pieces the jig carries, because a small rack raises per-piece cost and lengthens the queue.
Masking is the small detail that separates a clean job from a rejected one. A threaded boss left unmasked gains deposit in the root, and the screw that fitted the first article suddenly will not turn on the second.
When PVD Beats Electroplating
Physical vapour deposition lays metal from a vapour rather than from a bath, and it earns its place where wear resistance or colour consistency across different substrates matters more than the lowest cost per piece. For a bag that will be carried every day, that trade is often worth taking.
- PVD gives a harder surface than electroplating, which matters at feet, strap sliders and bag-to-table contact points.
- It produced the same tone across brass and stainless because the deposit chemistry is identical on both.
- Typical deposits run 0.3-0.5 µm, thicker than most decorative electroplate, at no loss of definition.
- The route adds roughly 5-8 working days after the base surface is finished, so it belongs on the critical path.
- Colour range is constrained by available targets; a specific house gold is still easier to hit with electroplating.
PVD is not a universal answer. Where a brand needs an exact vintage gold developed against a physical reference, electroplating over brass still gives finer control over hue, and the materials team will usually steer you there first.
How the Finish Is Proved: Thickness, Corrosion and Adhesion
A finish is proved against three independent questions: how thick is it, how long does it resist corrosion, and will it stay attached when the part flexes or changes temperature. Each question has a recognised method, and none is answered by looking at the part under a showroom light.
| Question | Method | Floor commonly written into the pack |
|---|---|---|
| Thickness | ISO 3497, X-ray spectrometric measurement | Gold tone 0.15-0.3 µm; 0.3-0.5 µm on high-contact parts; nickel barrier 1.5-2.5 µm |
| Corrosion resistance | ISO 9227 neutral salt spray; ASTM B117 is the parallel route often requested by North American buyers | 24 hours neutral salt spray as a floor, 48 hours for antique and dark finishes, with any base-metal show recorded as failure |
| Adhesion | Thermal shock followed by bend or taping, reviewed under ISO 2819 | No blistering or flaking after the agreed thermal cycle and bend |
| Abrasion resistance | Linear abrasion with a CS-10 wheel at 500 g loading | Agreed cycle count before the barrier shows, typically 500-1,000 depending on contact class |
| Nickel release, where claimed | EN 1811, referenced against the EU nickel restriction | Below the migration limit set for prolonged skin contact articles |
| Restricted substances | REACH Annex XVII review and California Prop 65 declarations | Per-batch declarations rather than an annual statement |
Two of those rows are regulatory rather than aesthetic. REACH Annex XVII governs restricted substances in articles placed on the European Union market, and California Prop 65 carries its own warning thresholds; both are answered with a per-batch declaration, which is why plating lines keep lot records rather than annual certificates.
What Commonly Goes Wrong, and the Fix for Each
Nearly every finish failure seen at inspection has one of five causes, and all five are specification or process problems rather than bad luck. Naming them in advance lets the technical pack prevent them.
- Wear-through at the cam: the decorative layer was specified too thin for a high-contact part. Raise gold to 0.3-0.5 µm there.
- Blistering after a week: insufficient copper strike over a porous casting, or contamination in the cleaning stage.
- Colour drift toward pink: the nickel barrier was too thin and copper diffused upward. Restore to 1.5-2.5 µm.
- Stiff or binding threads: unmasked threads gained deposit. Mask them, or cut the thread after finishing.
- Uneven tone between parts: brass and zinc components were plated to the same nominal figure in the same batch. Treat them as two lots with two references.
How Finish Choice Moves Your Calendar
Finish choice moves dates more than it moves unit cost, because each additional stage is a queue rather than a price. The shortest route uses a stock base with a stock finish; the longest introduces tooling, then first articles, then a batch approval, and only then takes its place on the bulk line.
Stock base, catalogue finish
The fastest path. Standard gold, palladium and light gold are available immediately and add no working days beyond finishing.
Stock base, custom finish
A bespoke tone over an existing base typically adds 7-10 working days while the bath is matched to your reference.
New tooled part
A die-cast tool takes around 15-20 working days, then 6-10 working days for first articles, longer at 12-15 for complex geometries.
PVD topcoat
Adds 5-8 working days after the base finish, booked before rather than after bulk material is cut.
Against that backdrop the programme itself runs 6-10 working days for sampling, 12-15 where the construction is complex, and 35-50 days for bulk at MOQ 500 pcs per style and colourway, inspected at AQL 2.5 under ISO 2859-1 and handed over FOB Xiamen. Finish samples ahead of that commitment are billed at USD 4.80 and credited against the first bulk order.
What to Send When You Brief a Finish
A finish brief becomes a real number when it arrives with six items attached. Without them, any quotation is a placeholder.
- A dimensioned drawing or a reference part, with which surfaces are classified as visible versus hidden.
- Target tone described against a physical reference, not a photograph, and the substrate each part will be made from.
- Contact class for each component, since that drives thickness far more than appearance does.
- The standards you will inspect against: ISO 3497 for thickness, ISO 9227 for corrosion, plus any buyer-specific protocol.
- Destination markets, because REACH, Prop 65 and CPSIA declarations are booked per batch for each one.
- The immovable date, so the finish sequence can be planned backwards rather than fitted in.
Production runs across 7 production lines with about 200,000 pcs per month of capacity, held through export experience since 2014 and carried out by our validated partner factory Quanzhou Yingming Bags, an SGS-validated site. Approvals for the sample route sit under luxury sampling, and the inspection protocol that receives the finished parts under luxury quality control.
Put a finish specification behind your drawing
Send the part list, the target tone and the date you cannot move. You will receive a stack specification with thickness, contact class and test lines completed, within two working days. Request a quote.
Frequently Asked Questions
What is the standard plating stack for luxury handbag hardware?
A decorative finish is a stack built in order: ultrasonic cleaning and acid activation, a copper strike around 1.0-2.0 µm to level the surface, a nickel barrier at 1.5-2.5 µm to stop the substrate migrating upward, then the decorative metal at 0.15-0.3 µm for gold tone. Antique darkening or a protective lacquer comes last.
How thick should gold plating be on a turn-lock?
A turn-lock cam is a high-contact part, so its cam and housing should be specified at 0.3-0.5 µm of gold over a 2.0-2.5 µm nickel barrier. The general house figure of 0.15-0.3 µm suits decoration and low-contact parts, but it wears through quickly where metal slides against metal every time the bag opens.
Why does a nickel barrier matter under gold?
Without a nickel barrier the copper in brass diffuses upward into the gold layer, and the colour gradually drifts toward pink. Handling accelerates that drift, so it appears earliest on the parts customers touch most. A barrier of 1.5-2.5 µm blocks the migration and is the single most cost-effective part of the stack.
What does polishing actually do to a component?
Polishing removes material through descending abrasives rather than adding shine. Typical sequence runs 180-220 grit to remove gate and parting marks, 320-400 to cut, and 600-800 to fine before buffing. Each stage must erase the scratch pattern of the previous one, because any skipped line reappears once the plating brightens the surface.
Should high-relief logo plates be buffed to a mirror?
Usually not. Aggressive cutting rounds the crisp edge of coined or cast relief, so the letter definition softens exactly as reflectivity rises. The technical pack should state which matters more for each part; where both matter, reduce buffing pressure, shorten the colour stage and accept a slightly lower mirror on the flat field.
What is the difference between rack plating and barrel plating?
Rack plating mounts each part on a jig that holds it through every tank, giving even deposit and no contact marks, at a higher cost per piece. Barrel plating tumbles loose parts together, which is faster and suits hidden rivets and washers, but leaves marks where components touch. Every visible component should be racked.
How is plating thickness measured?
X-ray fluorescence spectrometry, by the ISO 3497 method, reads the actual deposit on the actual part non-destructively in seconds. Ask for the reading to be recorded per batch and taken at a named point on the part, because thickness varies across geometry and a single reading on a flat field will overstate what sits at an edge.
How many hours of salt spray should hardware survive?
A 24-hour neutral salt spray run under ISO 9227, or ASTM B117 where a North American buyer requests it, is a reasonable floor for bright finishes. Antique and dark finishes are pushed to 48 hours, since the darkening chemistry can retain salts. In each case any base-metal show is recorded as a failure rather than a variation.
When is PVD a better answer than electroplating?
PVD suits parts where wear resistance or tone consistency across different substrates dominates: feet, strap sliders, bag contact points, and any line that mixes brass and stainless components. It typically deposits 0.3-0.5 µm with a harder surface, adds 5-8 working days after base finishing, and offers a narrower range of hues than a custom electroplated house gold.
Do REACH and Prop 65 apply to plated hardware?
Yes, because hardware is a component of an article placed on the market. REACH Annex XVII restricts certain substances in the European Union, and California Prop 65 sets its own warning thresholds. Both are answered with per-batch declarations from the finishing house rather than one annual certificate, which is why batch identity must be kept intact through finishing.
What makes a turn-lock stiff after plating?
Two causes account for most of it. The cam casting may be more than 0.10 mm out of round, which no finish will correct, or the thread gained deposit because it was not masked. Specify the dimensional tolerance, then either mask the thread or machine it after finishing and record the fit check per batch.
How much does finish choice move the bulk date?
A stock finish on stock components adds nothing. A bespoke tone adds 7-10 working days, a new die-cast tool adds 15-20 before first articles, and a PVD topcoat adds 5-8 after base finishing. Bulk itself runs 35-50 days at MOQ 500 pcs per style and colourway, so finish is usually the variable that must be booked earliest.
People Also Ask
How is handbag hardware plated?
Parts are cleaned and activated, then receive a copper strike around 1.0-2.0 µm, a nickel barrier at 1.5-2.5 µm and finally the decorative metal, usually gold tone at 0.15-0.3 µm. Visible parts are racked individually so nothing touches. Thickness is verified on the part itself by X-ray fluorescence.
Why does fine hardware suddenly lose its colour?
Because the decorative layer is too thin and the nickel barrier underneath is thinner still, so the copper in the substrate diffuses upward. Handling accelerates the drift, which shows first on cams, feet and strap sliders. Specifying 0.3-0.5 µm gold over a 2.0-2.5 µm barrier prevents most of it.
Is PVD better than electroplating for bag hardware?
For wear-critical parts, yes. PVD deposits 0.3-0.5 µm of a much harder surface and gives identical tone over brass and stainless. It costs more and adds 5-8 working days, and it cannot match every custom gold that electroplating can produce.
What test proves hardware will not rust?
Neutral salt spray under ISO 9227, or ASTM B117 where the buyer asks. Twenty-four hours is a normal floor for bright finishes and 48 hours for antique ones. Pair it with X-ray thickness reading under ISO 3497 so the result can be traced to an actual deposit.
Can brass and zinc parts be plated to match?
To a point. The two substrates reflect differently, so the same nominal gold reads warmer over brass. PVD narrows the gap, but for close matching the parts should be treated as two lots against two references, with approval carried out under controlled lighting rather than from photographs.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- ISO — International Organization for StandardizationISO Publisher of ISO 3497 for coating thickness measurement by X-ray spectrometry, ISO 9227 for neutral salt spray testing and ISO 2819 for adhesion methods, all referenced here.
- ASTM InternationalASTM International ASTM B117 is the alternative salt spray practice frequently requested by North American buyers alongside ISO 9227.
- European Chemicals AgencyECHA Administrator of REACH, including the Annex XVII restrictions that apply to metal components placed on the European Union market.
- California Office of Environmental Health Hazard AssessmentOEHHA The authority behind California Proposition 65, which governs warning requirements for listed substances in goods sold in that state.
- International Union of Leather Technologists and Chemists SocietiesIULTCS The body behind harmonised leather test methods, whose approach the metal and leather houses coordinate when a component is specified alongside its panel.