How to Avoid Luxury Bag Packaging Damage in Shipments: A Case Sequence
Why does fine presentation packaging arrive crushed when the piece inside is perfect? Because the outer carton, not the presentation carton, carries the journey, and it is usually the specification nobody drew. Three numbers prevent most claims: an outer board rated at edge crush 32 or better, at least 25 mm of void between the presentation carton and every outer wall, and a desiccant charge near 10 g per carton. Add a 460 mm corner-first drop test and most damage claims disappear before despatch rather than after.
A Shipment That Went Wrong
A European label ships four hundred pieces for a seasonal launch. The bags arrive perfect. A quarter of the presentation cartons arrive with crushed corners and scuffed wrap, and the launch photography has to be rescheduled because nothing in the set can be photographed. Nobody disputes what happened; everybody disputes whose specification failed, because the outer pack was never properly drawn by anybody at all.
The review afterwards found three things, and they are the same three found nearly every time. The outer board was too light for the stack height. The presentation cartons carried no void protection, so they acted as structure and took the load directly. And the pallet had been wrapped tightly enough to pull the top cartons inward, which is how that particular triangular crush along the upper layer appeared.
Where Does Damage Actually Occur?
Almost all of it happens in three places, and almost none of it happens where teams expect. Roughly half occurs during handling at consolidation and transhipment rather than during the ocean leg. Most of the remainder occurs in the last mile, particularly where cartons are hand-stacked into a van. Only a small residual comes from compression over a long stand rather than from any single event.
That distribution matters because it changes the correct answer. A pack designed against a week of ocean motion is protecting against the wrong hazard. The specification that works is built around drops, throws and stacking: impacts lasting milliseconds rather than days. That is precisely what the ISTA sequences and ASTM D4169 are written to simulate, and why they belong in the drawing rather than in a telephone conversation.
Specifying the Outer Carton
Start with the outer, because it takes everything. Specify by performance rather than by thickness: an edge crush test rating of 32 corresponds to about 4.5 kilonewtons per metre, and anything below that struggles under a full mixed pallet. Double-wall construction matters more than caliper, since two thin walls resist buckling considerably better than one thick wall of equal weight.
Size is specified next and is often where the trouble begins. The presentation carton should sit with at least 25 mm of void on every face, filled with a shock-absorbing medium that will not settle. A close-fitting outer transfers every impact straight through to the presentation carton, and a presentation carton is engineered to look immaculate rather than to absorb a thrown parcel.
- Outer board rating
- Edge crush test 32 or better, roughly 4.5 kN per metre
- Construction
- Double-wall preferred over single-wall at equal weight
- Void protection
- 25 mm minimum on every face, non-settling medium
- Drop test height
- 460 mm corner-first for parcels under about 9 kg
- Desiccant charge
- Near 10 g per carton, higher for ocean freight
- Pallet wrap
- Three layers minimum with about 50 percent overlap
- Stack overhang
- 25 mm maximum beyond the pallet footprint
Void, Cushioning and What Settles
Void fill fails by settling rather than by compressing. Loose fill migrates downward during a long transit, leaving the upper face unprotected exactly where handling is heaviest. Bubble cushioning performs better but tends to sit at the base rather than around the carton. The reliable answer is a moulded or folded paper structure that occupies the whole void and holds its shape for the duration.
Whatever is chosen, prove it rather than assume it. Pack one carton, drop it from 460 mm corner-first, open it and measure whether anything moved. Then repeat after twenty-four hours standing, because the movement that matters on a multi-week transit accumulates rather than shocks, and only the standing test reveals accumulation before it is discovered by a customer.
Moisture: The Quiet Cause Behind Many Claims
Moisture damages in ways that look like rough handling. A carton arriving slack, wrap lifting at the corners, faint tide lines along a base edge: all three are humidity rather than impact, and they are most common on ocean freight, where a container can swing dramatically in temperature between day and night across twenty-eight days at sea.
Two controls remove most of it. Charge each carton with desiccant near 10 g, sized upward for long ocean legs and humid destinations. Avoid sealing cartons late on a humid afternoon without conditioning, because trapping damp air inside a sealed carton guarantees the very problem the desiccant was included to solve, only faster and from the inside.
Palletising and Container Loading
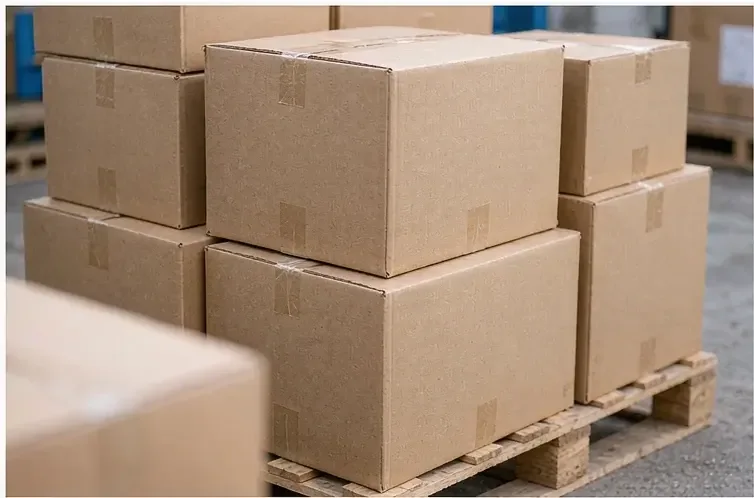
Pallet decisions cause more presentation damage than any other single choice. Align every carton to the pallet footprint, allowing no overhang beyond about 25 mm, and avoid mixed heights within a single layer. Build columns rather than interlocking patterns where the cartons permit it, because interlocking transfers load into the carton body rather than down into the pallet structure.
Wrap tension is the avoidable error that repeats most often. Three layers with about 50 percent overlap secure the load without pulling it inward, whereas wrapping tightly in order to feel secure deforms the top layer before midday. Add edge protectors on any stack taller than about 1.2 m, since they spread the strap load and stop the strap biting into the upper cartons.
The Sequence Worth Testing Before Every Programme
Testing does not need a laboratory, only an agreed sequence repeated identically each time. One conditioning period at the temperature and humidity the shipment will meet. One drop test from 460 mm delivered corner-first onto a hard floor. One compression period under a loaded stack. Then a full open and inspection against photographs taken before packing, since damage found afterwards is always argued about.
- Condition cartons for twenty-four hours at the humidity the route will actually meet.
- Photograph every sample face before packing, so that later comparison has a fixed reference.
- Drop from 460 mm corner-first, then repeat on the two adjacent corners rather than only one.
- Stack under a load equivalent to the tallest pallet in the route for twenty-four hours.
- Open, photograph again, and record movement in millimetres rather than in adjectives.
- Repeat the whole sequence after any change to board, void fill or pallet pattern.
What to Do When a Claim Arrives
Claims are settled with evidence rather than with argument, and evidence has to be planned for in advance. Photograph the pallet before unloading, including the whole stack rather than the damaged carton alone. Photograph during unloading, showing how the load was arranged. Retain the outer carton from any damaged presentation pack, because it is the piece of the puzzle almost always thrown away first.
Three questions then resolve most claims cleanly. Was the outer board to specification, checked rather than assumed? Did the carton fail at the corners, which points to handling, or across the faces, which points to compression? And was the desiccant present and dry, which distinguishes an impact claim from a humidity one that no amount of board would have prevented.
Last-Mile Handling and What Boutiques Do Wrong
The final stage deserves its own attention because it is the one nobody controls. Cartons arrive at a boutique and are stacked against a wall three high, opened from the top with a blade run along the seam, and then moved again once the stock room is full. Every one of those steps can undo twenty-eight days of careful packing.
Three countermeasures help and none cost anything. Mark the outer clearly with a this-way-up indicator and a slash line rather than a lift point, because a blade run along the wrong seam will cut straight into the presentation carton beneath. Request that cartons are opened with a low-penetration blade. And specify an easy-open tear strip on the outer, which removes the blade from the process altogether.
Stack limits are worth stating on the outer as well, printed rather than implied. A carton designed for three-high stacking will survive a warehouse and will fail beneath a six-high pile in a stock room during a sale week. Stating three high costs nothing and is read by anybody who has ever wondered how far to go.
The presentation carton is engineered to look immaculate, not to carry a stack. Everything structural belongs on the outer specification, and it belongs there before the inner carton is drawn.
Reading the Damage Pattern
Damage patterns are diagnostic once somebody learns to read them. A crush along the top edge of the upper layer is almost always wrap tension. Crushed lower corners point to insufficient board strength or to overhang beyond the pallet. Scuffing confined to one face suggests sliding rather than dropping, usually against another pallet during transhipment. Each pattern has a different correction, so misreading costs a second failure.
The patterns that matter least visually are sometimes the most serious commercially. A slight bow across a lid is invisible in a photograph and obvious to a customer holding it, and it usually means board below specification rather than anything that happened in transit. That is why board properties are worth verifying on arrival rather than trusting to a printed mark on the carton.
Insurance, Terms and Who Carries the Risk
Terms decide who pays, and they are agreed long before anyone knows whether the shipment will arrive whole. Under FOB terms, risk passes at the port of loading, which means the pack has to be specified to survive everything after that point without the seller being able to influence it. This is the reason export pack specification matters more than domestic presentation for houses shipping from Asia.
Cargo cover is worth carrying regardless of how well the pack performs, and it is far easier to claim against when the testing sequence above has been documented. An insurer presented with photographs, drop results and board ratings settles quickly; the same insurer presented with a description of what the pack looked like does not, whatever the terms say.
Building the Specification Into the Drawing
The correction after the opening case was unglamorous: five lines added to the packaging drawing. Outer board rated at edge crush 32 or better, double-wall. Twenty-five millimetres of non-settling void protection on every face. Ten grams of desiccant per carton. Pallet pattern with columns, no overhang beyond 25 mm. Three layers of wrap at 50 percent overlap, with edge protectors above 1.2 m.
Those five lines cost very little per unit and removed the problem entirely on the following season. The lesson generalises: presentation damage is rarely caused by a presentation carton being too light, and almost always caused by an outer specification that nobody wrote down because nobody owned it.
Programme Figures and Export Timing
Our programme runs through our validated partner factory Quanzhou Yingming Bags, an SGS-validated site with 7 production lines and roughly 200,000 pcs per month of capacity, holding export experience since 2014. Sample presentation packs take 6-10 working days, or 12-15 where export cartons are developed alongside them; bulk occupies 35-50 days; and minimums sit at 500 pcs per style and colourway leaving FOB Xiamen.
Presentation cartons are inspected on the standard plan, a sample drawn at AQL 2.5 under ISO 2859-1 and read against an approved first article. The presentation specification itself sits on luxury packaging, the full inspection regime on luxury quality control, and the sample and tooling sequence on luxury sampling.
Have the export pack specified before the booking is made
Send the route, the outer case size, the pallet pattern and the quantity per style. Include the destination climate, since a humid route changes the desiccant charge and deserves to be decided before the booking rather than after the first arrival. You will receive an export pack specification naming board rating, void protection, desiccant charge and pallet rules. Request a quote.
Frequently Asked Questions
Why does presentation packaging arrive crushed when the piece inside is fine?
Because the outer carton takes the journey and the presentation carton only has to look right. Where no outer specification exists, the presentation carton becomes structure, and it is not built to carry a stack or a drop.
What board strength suits an export outer carton?
An edge crush test rating of 32 or better, roughly 4.5 kilonewtons per metre, in double-wall construction. Two thin walls resist buckling considerably better than one thick wall carrying the same weight of material.
How much void protection is needed inside an outer case?
At least 25 mm on every face, using something that will not settle. Loose fill migrates downward over a long transit and leaves the upper face unprotected exactly where handling is heaviest.
What drop height should an export carton survive?
460 mm delivered corner-first onto a hard floor for parcels under about 9 kg, repeated on two adjacent corners rather than once only. The ISTA sequences and ASTM D4169 give fuller programmes for mixed freight.
Why do cartons arrive slack and discoloured along the base?
Humidity rather than impact. Ocean containers swing widely in temperature between day and night, condensing moisture inside the case. Charge around 10 g of desiccant per carton and avoid sealing damp air inside.
How much overhang is acceptable on a pallet?
About 25 mm at most beyond the pallet footprint. Anything beyond that leaves the carton unsupported, and crushed lower corners are almost always an overhang problem rather than a board specification problem.
Why is the top layer always the one that suffers?
Usually wrap tension pulling it inward. Three layers at about 50 percent overlap secures a load without deforming it, whereas wrapping tightly to feel secure deforms the upper cartons before they leave the warehouse.
Should cartons be stacked in columns or interlocked?
Columns, where carton sizes permit it. Interlocking patterns transfer load sideways into the carton body, while column stacking carries it down through the strongest axis of every carton into the pallet structure.
How should a damage claim be documented?
Photograph the whole pallet before unloading, photograph again during unloading to record the arrangement, and retain the outer carton from every damaged presentation pack rather than discarding it first.
How can you tell whether damage came from humidity or impact?
Check whether the desiccant is spent and look for tide lines along a base edge. Both indicate condensation. Clean crushed corners without those signs point unambiguously to handling rather than to moisture.
What are the minimum programme terms for export packs?
Minimums sit at 500 pcs per style and colourway, with sample export cartons taking 6-10 working days and up to 12-15 where outer cases are developed alongside the presentation pack. Bulk occupies 35-50 days.
When does risk transfer under FOB terms?
At the port of loading, which means the pack has to survive everything afterwards without the seller influencing it. That is why export specification matters more than domestic presentation for houses shipping from Asia.
People Also Ask
Is double-wall board worth the extra cost?
Yes for anything palletised. Two thin walls resist buckling better than one thick wall of equal weight, and the additional cost is small against the value of the damage avoided.
Can the existing presentation carton simply be made heavier?
It can, and it rarely helps. Presentation cartons fail for structural reasons rather than weight reasons, so the correct answer is almost always void protection and a stronger outer instead.
How often should the transit sequence be repeated?
Whenever anything changes: board, void fill, pallet pattern or route. As packaging goes, few things cost less than re-running a drop and a stack test before committing several hundred units.
Do edge protectors really matter?
On stacks above about 1.2 m, yes. They spread strap load across the corners and stop the strap biting into upper cartons, which is the most common cause of damage nobody remembers causing.
Should every carton be inspected before despatch?
A sample drawn at AQL 2.5 under ISO 2859-1 read against an approved first article is sufficient, provided the outer specification is documented. Undocumented assumptions, not inspection gaps, cause most claims.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- International Safe Transit AssociationISTA Publishes the ISTA 3 series of transit simulation sequences used to prove export packaging before despatch.
- ASTM International standardsASTM International Publisher of ASTM D4169 for performance testing of shipping containers and the methods behind edge crush measurement.
- ISO - International Organization for StandardizationISO Publisher of ISO 2859-1 for attribute sampling and of the paper and board conditioning standards used before testing.
- SGS - Inspection and verificationSGS Third-party validation and goods-in inspection body referenced for site validation and pre-shipment checks.