Luxury Handbag Hardware Failure QC Checks
Hardware is the part of a luxury bag that fails first and costs most to put right. Leather wears gracefully; a loosened turn-lock, a zip that catches at the same tooth every time, or a plating that clouds after a season reads as a defect immediately and cannot be blended into a patina story. The answer is to specify hardware in numbers before it is ordered: plating thickness, salt spray exposure, cycle endurance and pull load, each with a pass threshold and a documented method. Our bench runs 24-hour neutral salt spray, 5,000 open-and-close cycles on a rigged closure, and a 25 kg static pull held for 60 seconds on load-bearing rings. This guide sets out every check, the number behind it, and the order in which to run them.
Why hardware fails more often than leather
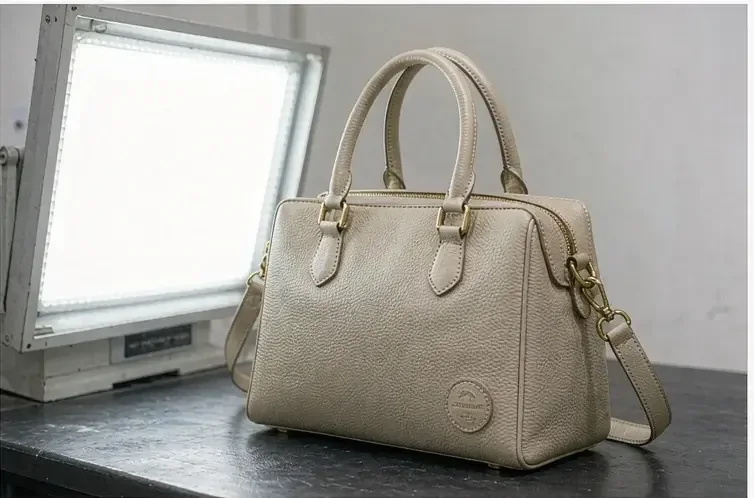
Leather is forgiving. It absorbs variation, develops character and hides small inconsistencies in a way that clients read as quality. Hardware has no such tolerance. A closure either seats cleanly or it does not, a plating either holds its colour or it clouds, and a client notices a stiff lock on the first attempt rather than the fifth. That asymmetry is why hardware attracts a disproportionate share of returns relative to the surface area it occupies on the bag.
The second reason is that hardware arrives from outside. It is bought to a specification, plated by a specialist, and assembled onto the bag by a bench that did not make it. Every handover in that chain is a place where the specification can quietly change, which is why the checks have to run at intake as well as at final inspection.
The numbers that define a hardware check
A hardware standard that says the finish must be good is not a standard. The following are the numbers we write into every order, and each one has a method, a threshold and an action if it fails. Where a brand has its own figures we apply theirs, but we require a figure rather than an adjective for all six.
| Check | Method and threshold | Sample | Action if it fails |
|---|---|---|---|
| Plating thickness | X-ray fluorescence measurement, minimum 0.5 microns gold over a barrier layer | 3 pieces per batch | Quarantine the batch, return to the plater |
| Salt spray | 24 hours neutral salt spray, no base metal corrosion or blistering | 3 pieces per batch | Reject the batch, review bath records |
| Cycle endurance | 5,000 open-and-close cycles on a rigged closure, no loosening or tooth wear | 2 pieces per style | Redesign the engagement, re-tool if needed |
| Static pull | 25 kg held for 60 seconds on load-bearing rings and strap anchors | 3 pieces per batch | Reject the batch, review the alloy and the rivet setting |
| Magnet strength | 1.5 kg of separation force on a magnetic closure | 3 pieces per batch | Re-specify the magnet grade |
| Nickel release | Compliance with REACH Annex XVII limits for items in prolonged skin contact | 1 piece per batch | Reject the batch, escalate to compliance |
Plating: thickness, adhesion and salt spray
Plating failure has two faces. The first is thickness: a layer too thin to survive contact with skin, perfume and the inside of a client's coat. We hold gold plating at a minimum of 0.5 microns over a barrier layer and measure it by X-ray fluorescence rather than by eye, because the difference between a plating that lasts a season and one that lasts five years is invisible at the point of delivery.
The second face is adhesion, which thickness measurement cannot see. A thick plating poorly bonded will lift in sheets; a thin plating well bonded will wear evenly and look intentional. Salt spray is the practical proxy for both. Twenty-four hours of neutral exposure will reveal pinholing, edge breakthrough and contamination in the barrier layer, all of which appear as corrosion at the edges and on the inside surfaces where the spray settles.
- Measure thickness on a flat face, not on a corner, where plating naturally runs thin.
- Read the inside surfaces after salt spray; edge corrosion there precedes visible failure outside.
- Compare every batch against the reference clasp under D65 and TL84 for shade, not just corrosion.
- Log the plating bath identity against the hardware batch so a failure traces to a run.
- Re-test after any re-polishing, because polishing removes thickness as well as imperfections.
Mechanical endurance: cycles and pull loads
Endurance answers the question a client will ask in year two. A closure that feels correct in the showroom and loosens after a season has failed a test nobody ran. We rig closures to a cycling frame and run 5,000 open-and-close cycles, inspecting at intervals for tooth wear, spring fatigue and any increase in the force needed to operate the mechanism. A closure that requires noticeably more force at cycle 4,000 than at cycle 200 will not survive a client's second winter.
Load paths: rings, anchors and strap attachments
Load-bearing hardware fails differently from closures: it does not wear, it lets go. Every D-ring, strap anchor and handle attachment point is tested with a 25 kg static load held for 60 seconds, applied in the direction the bag will actually be carried. The failure we are looking for is rarely the metal itself; it is the rivet setting, the reinforcement beneath the leather, or the leather tearing around a plate whose edges were never eased.
Where a pull test fails, we cut the piece open and look at the reinforcement rather than simply rejecting the batch. A rivet set through a single thickness of leather will fail at a load that a rivet set through a reinforced panel carries comfortably, and the correction is in the pattern rather than in the hardware.
Fit and seating: the visible half of hardware QC
Half of what a client perceives as hardware quality is not the hardware at all. It is how the hardware sits on the bag. A plate that rocks because the leather beneath it was not skived evenly, a lock whose escutcheon is a millimetre off centre, feet that do not all touch a flat surface at once: these are assembly faults that read as hardware faults and are corrected at the bench rather than at the plater.
Plating clouding
Finish clouds or spots within a season. Caused by thickness below specification or contamination in the barrier layer, caught by salt spray at intake rather than by inspection at the end.
Closure loosening
Operating force drops and the lock rattles. Caused by spring fatigue or tooth wear, caught by cycle endurance testing before the style is released.
Anchor pull-out
A ring or strap anchor separates under load. Usually a reinforcement or setting fault rather than a metal fault, caught by static pull testing.
Seating deviation
A plate rocks or sits off centre. An assembly and skiving fault that clients read as poor hardware, corrected at the bench with a jig.
The checklist, in order
- At intake, count and identify the batch, log the plating bath identity, and compare shade against the reference clasp under D65 and TL84.
- Measure plating thickness by X-ray fluorescence on three pieces, on a flat face rather than a corner.
- Run 24 hours of neutral salt spray on three pieces and read the inside surfaces as well as the outside.
- Rig two closures per style and cycle 5,000 times, recording operating force at intervals.
- Apply a 25 kg static load for 60 seconds to three rings or anchors in the carrying direction.
- Confirm nickel release compliance against REACH Annex XVII limits for items in prolonged skin contact.
- At the bench, check seating: no rocking plates, centred escutcheons, and all feet touching a flat surface together.
- At final inspection, cycle every closure on every drawn piece twenty times and record any change in feel.
What a hardware failure costs
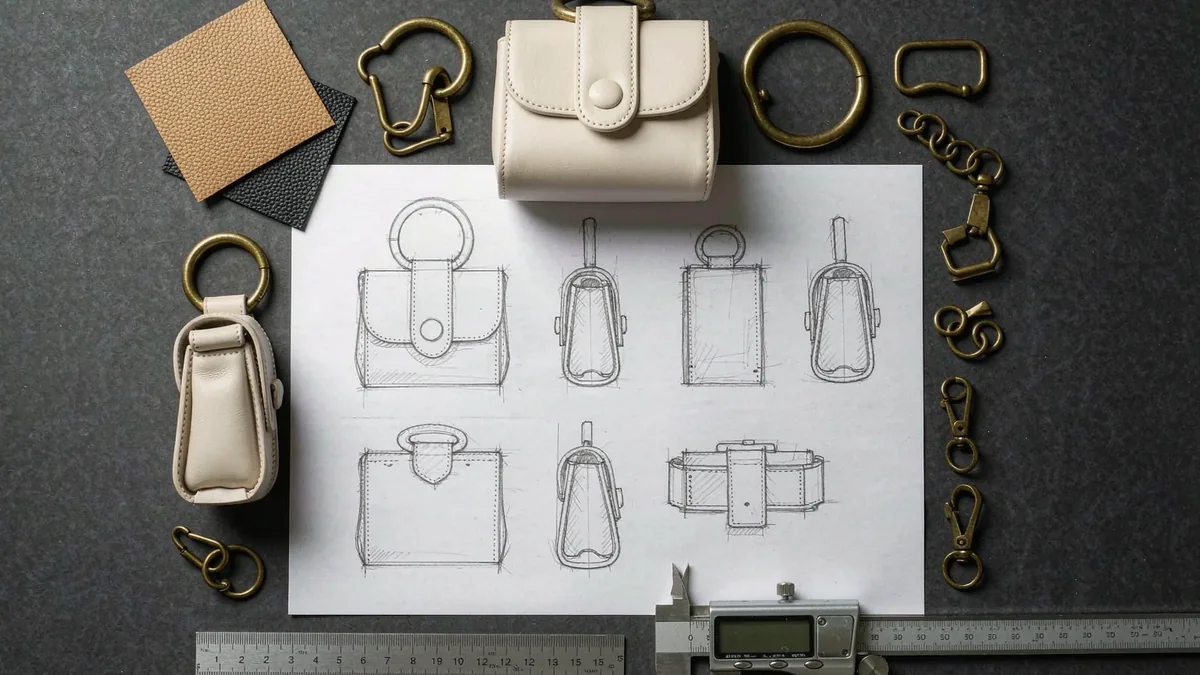
Hardware failure is expensive because it is rarely repairable in the field. A strap anchor that has pulled out cannot be corrected by a boutique; the bag comes back, and the return carries freight both ways, a client service touch and the reputational cost of a piece that failed in public. Replacing one failed closure assembly, including the parts, the bench time to set it and the re-inspection of the finished piece, costs around USD 4.80. That figure excludes every cost that actually hurts.
Against that, the full intake regime — thickness measurement, salt spray, cycling and pull testing — costs a small fraction of the value of one returned piece and is run once per batch rather than once per bag. The arithmetic favours testing heavily at intake and rarely arguing later.
Plating thickness is the single figure most correlated with hardware longevity. Hold it at 0.5 microns minimum over a barrier layer and measure it; do not accept a description of the finish.
Reading the results without over-reacting
Not every failure means the same thing. A single piece failing salt spray inside a batch of three usually points at a contaminant in one rack position rather than at the whole bath, and we re-sample before condemning. Three pieces failing together is a bath problem and the batch is rejected. A closure that reaches 4,000 cycles before loosening is a different conversation from one that fails at 600, and both are worth recording even when the style is eventually approved.
Setting the hardware standard on your order
Name the alloy, the plating and its thickness, the finish, the cycle expectation and the load expectation, and attach a reference clasp that has been through the full regime. That reference is what settles every later argument, exactly as a signed leather panel settles a shade dispute. Where a brand has a house hardware standard, we work to it and report against it; where it does not, we build one from these figures and record it on the order file.
- Plating thickness
- Minimum 0.5 microns gold over a barrier layer, measured by X-ray fluorescence
- Salt spray exposure
- 24 hours neutral, no base metal corrosion or blistering
- Closure endurance
- 5,000 open-and-close cycles on a rigged frame
- Bench cycling
- 20 cycles per closure on every drawn piece at final inspection
- Static pull load
- 25 kg held for 60 seconds on load-bearing rings and anchors
- Magnetic closure force
- 1.5 kg separation force
- Nickel release
- Within REACH Annex XVII limits for prolonged skin contact
- Intake sample
- 3 pieces per batch for thickness and salt spray, 2 per style for cycling
- Seating tolerance
- No rocking plates, escutcheon centred within 0.5 mm
- Final inspection frame
- General level II, 50 pieces on a 500-piece lot, AQL 2.5
- Rework cost reference
- Around USD 4.80 to replace one closure assembly including re-inspection
- Minimum order quantity
- 500 pieces per style per colourway
- Sampling lead time
- 6 to 10 working days, 12 to 15 for complex constructions
- Bulk lead time
- 35 to 50 days from approved sample
- Shipment terms
- FOB Xiamen
Hardware QC in one paragraph
- Specify hardware in numbers and test it at intake, not only at the end. Hold gold plating at 0.5 microns minimum over a barrier layer and measure it, expose three pieces per batch to 24 hours of neutral salt spray, cycle two closures per style 5,000 times while recording operating force, and apply 25 kg for 60 seconds to every load-bearing anchor. Check seating with a jig at the bench, because half of what a client calls a hardware fault is an assembly fault. Replacing one failed closure costs around USD 4.80 before freight and reputation, which is the argument for testing heavily once per batch.
Put numbers on your hardware standard
Send us your hardware specification or a physical sample and we will return measured thickness, salt spray results and cycle endurance before you commit to a batch. Request a hardware consultation and quotation at /contact-quote/.
Frequently Asked Questions
Why does hardware fail more often than leather on a luxury bag?
Leather absorbs variation and develops character; hardware does not. A closure either seats cleanly or it does not, and a client notices a stiff lock on the first attempt. Hardware also arrives from outside, so every handover is a place the specification can quietly change.
What plating thickness should I specify?
We hold gold plating at a minimum of 0.5 microns over a barrier layer and measure it by X-ray fluorescence on a flat face rather than a corner. Thickness below that survives a season rather than years, and the difference is invisible at delivery.
How long should a salt spray test run?
Twenty-four hours of neutral salt spray on three pieces per batch is our standard. It reveals pinholing, edge breakthrough and barrier layer contamination, all of which appear as corrosion on edges and inside surfaces.
What is cycle endurance testing?
A closure is rigged to a frame and opened and closed 5,000 times, with operating force recorded at intervals. A closure needing noticeably more force at cycle 4,000 than at 200 will not survive a client's second winter.
How much load should a bag strap anchor carry?
We apply 25 kg held for 60 seconds in the direction the bag is actually carried. Failure is usually in the rivet setting or the reinforcement beneath the leather rather than in the metal itself.
Does nickel release matter for bag hardware?
Yes. Hardware in prolonged contact with skin must sit within REACH Annex XVII limits. We test one piece per batch and escalate any exceedance to compliance rather than releasing it.
How many pieces are tested from each hardware batch?
Three pieces per batch for thickness and salt spray, two per style for cycle endurance, and three for static pull. Final inspection then cycles every closure twenty times on each of the 50 drawn pieces.
What should I do if one piece fails salt spray?
Re-sample before condemning the batch. A single failure usually points at a contaminant in one rack position, while three failures together indicate a bath problem and the batch is rejected.
What is seating and why is it checked separately?
Seating is how hardware sits on the bag: no rocking plates, centred escutcheons, all feet touching a flat surface together. Clients read a seating fault as a hardware fault, but the correction is a skiving and jig issue at the bench.
What does it cost to replace a failed closure?
Around USD 4.80 for the parts, the bench time to set it and the re-inspection of the finished piece. That excludes return freight, client service handling and the reputational cost of a piece that failed in public.
Should hardware be tested at intake or only at final inspection?
Both, but intake carries the weight. Testing at intake catches a whole batch before it is assembled onto five hundred bags; final inspection only confirms what has already been built.
Can re-polishing fix a plating fault?
It can remove imperfections, but it also removes thickness, so any re-polished piece must be re-measured. A plating brought back to a bright finish at 0.3 microns will fail in the field even though it passed visually.
People Also Ask
How do you test bag hardware quality?
Measure plating thickness, expose samples to neutral salt spray, cycle closures on a rig, apply static pull loads to anchors, and check seating with a jig. Each test has a numeric threshold rather than a visual judgement.
What causes plating to tarnish on a handbag?
Usually thickness below specification, contamination in the barrier layer, or pinholing that lets moisture reach the base metal. Contact with perfume and skin chemistry accelerates what the plating was too thin to resist.
How many times should a bag clasp open and close?
A luxury closure should survive 5,000 cycles on a rigged frame with no loosening and no significant change in operating force. At final inspection we cycle every closure twenty times per drawn piece.
What is a pull test on a handbag strap?
A static load, typically 25 kg, applied for 60 seconds in the carrying direction to a ring or anchor. It reveals whether the setting and reinforcement, rather than the metal, are adequate.
Is hardware covered by the same AQL as the rest of the bag?
Yes. A hardware fault is classified by severity like any other: a stiff closure is major and counted against AQL 2.5, while a detachable small part is critical and carries zero tolerance.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- ISO 2859-1:1999 Sampling procedures for inspection by attributesInternational Organization for Standardization Defines the sampling frame of 50 pieces on a 500-piece lot used when hardware findings are classified and counted.
- ISO 9001:2015 Quality management systemsInternational Organization for Standardization Framework for the documented intake testing, batch traceability and corrective action described here.
- REACH Annex XVII restrictions, including nickel releaseEuropean Chemicals Agency Basis for testing nickel release on hardware in prolonged contact with skin before a batch is released.
- Consumer product safety and recall guidanceU.S. Consumer Product Safety Commission Basis for treating detachable hardware parts and sharp edges as critical defects at zero tolerance.
- Reporting on hardware, trims and compliance in luxury supply chainsSourcing Journal Industry reporting on the outsized share of returns attributable to hardware relative to its surface area.