How SGS Testing Complements Luxury Bag QC: Six Questions, Answered in Order
SGS testing complements a luxury bag inspection because the two answer different questions: an AQL 2.5 plan decides whether a lot should be released, while laboratory testing decides whether the material behind it was ever compliant. Physical tests cover tensile strength to ISO 3376, finish adhesion to ISO 11644 and rubbing to ISO 105-X12; chemical tests cover chromium VI and azo dyes under REACH Annex XVII.
Question One: What Does an AQL Inspection Not Tell You?
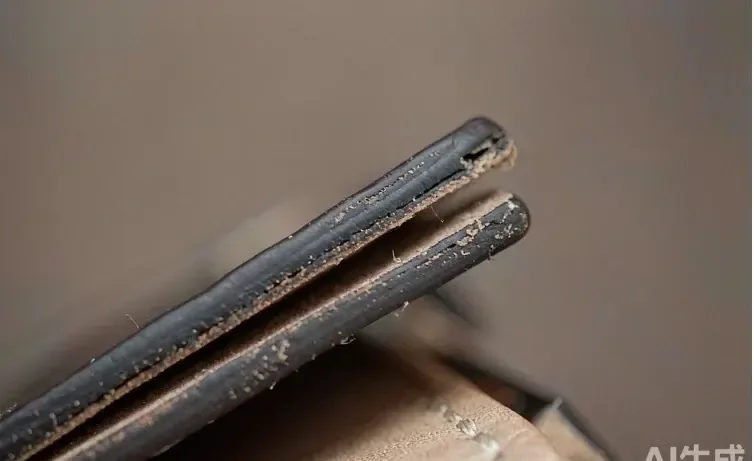
An AQL 2.5 inspection is a count taken on a table. It tells you how many of the drawn pieces carry a visible fault, and it tells you whether the lot passes. It does not tell you whether the finish on the shell will adhere after six months, whether the dye contains a restricted aromatic amine, or whether the hardware plating is thick enough to survive a season of handling.
Those three are laboratory questions, and no amount of looking answers them. Finish adhesion is measured by pulling a coated surface off its substrate under ISO 11644 and reading the force in newtons. A restricted amine is measured in milligrams per kilogram of material. Plating thickness is read on an X-ray fluorescence instrument in micrometres. An inspector with a loupe can suspect all three and prove none of them.
Question Two: Which Tests Cover What the Plan Misses?
The tests worth specifying on a designer handbag fall into two groups. Physical tests describe how the material behaves: tensile strength to ISO 3376, tear resistance to ISO 3377, finish adhesion to ISO 11644, flexing resistance to ISO 5402 and colour fastness to rubbing under ISO 105-X12. Chemical tests describe what the material contains: chromium VI, azo dyes, formaldehyde, pH and heavy metals.
- Tensile strength
- ISO 3376, minimum agreed per hide lot
- Tear resistance
- ISO 3377
- Finish adhesion
- ISO 11644, read in newtons per 10 mm
- Flexing resistance
- ISO 5402, cycle count agreed for the article
- Colour fastness to rubbing
- ISO 105-X12, grey scale 4-5 dry and 4 wet
- Chromium VI
- ISO 17075, against the REACH Annex XVII limit
- Azo dyes
- Against the REACH limit of 30 mg per kg
- Formaldehyde
- ISO 17226
- pH of the leather
- ISO 4045
- Plating thickness
- X-ray fluorescence, 0.15-0.3 µm on brass
- Salt spray
- ISO 9227, 24 hours standard and 48 for high wear
A note on limits: the numbers are set by regulation rather than by preference, and they differ by market. The REACH restriction on chromium VI in leather is expressed as 3 mg per kg, and the restriction on certain azo dyes as 30 mg per kg for each listed aromatic amine. Testing is therefore specified against the market the piece will be sold in, not against a single universal figure.
Question Three: How Are Physical Tests Actually Run?
Physical testing begins with sampling the material rather than the finished piece. Swatches are cut from the same hide lot and the same finishing batch that the run will use, conditioned for 24 hours, and then tested. Tensile strength pulls a dumbbell-shaped specimen until it breaks and reports the force over the cross-section. Finish adhesion bonds a standard tape or a defined substrate to the finish and pulls it off at a controlled rate.
- Swatches are cut from the hide lot and finishing batch that the run will actually use.
- Conditioning runs 24 hours at a standard temperature and humidity before testing.
- Tensile and tear specimens are cut in two directions, along and across the hide.
- Colour fastness is read on a grey scale after a defined number of rubs, dry and wet.
- Reports are issued against the swatch, so the lot identity has to be recorded.
The first item is where most programmes go wrong. A test run on a swatch from a different hide lot proves nothing about the lot that was used, and because the report carries the sample description rather than the order number, the discrepancy is only found when a question is raised and the report cannot answer it.
Question Four: How Does Chemical Compliance Testing Work?
Chemical testing asks whether restricted substances are present above a legal limit, and the tests are set by regulation rather than by the industry. Under REACH Annex XVII, chromium VI in leather is restricted, as are certain azo dyes that can release listed aromatic amines, nickel release from metal items in prolonged contact with skin, and certain phthalates. California Prop 65 adds a separate list with its own warning obligations.
Chromium VI
Tested to ISO 17075 against the REACH Annex XVII limit, expressed as 3 mg per kg. It is a tanning by-product, so the result belongs to the tannery lot rather than to the bench.
Azo dyes
Tested against the REACH restriction of 30 mg per kg for each listed aromatic amine. Relevant wherever a dyed shell or lining is specified in a strong colour.
Nickel release
Tested on metal items in prolonged contact with skin against the REACH Annex XVII limit. Relevant to buckles, chains and any metal that sits against the hand.
Prop 65
A separate Californian list with its own warning obligations, checked on the substance list rather than on an EU limit. Specify it where the piece is sold in that market.
One structural point matters. Chemical results belong to the material, not to the piece. A chromium VI result traces to the tannery and its lot, and a nickel release result traces to the plating and its bath, which is why the reports have to be read alongside the lot records rather than filed beside the inspection report.
Question Five: When Should Testing Happen Relative to the Run?
Material testing belongs before cutting, during the same window as the pre production check, because a result that arrives after the panels are cut is a result about a lot that has already been spent. Reports typically take 5-7 working days, which fits inside the 6-10 working days of sampling window if the swatches are sent on the first day rather than the fifth.
| Test | Moment | Why then | Report time |
|---|---|---|---|
| Material physical | Before cutting, day one of sampling | The lot has not been spent yet | 5-7 working days |
| Chemical compliance | Before cutting, same window | A restriction is not a defect to re-work | 5-7 working days |
| Plating thickness | On the hardware lot before setting | A bath drifts within a week | 2-3 working days |
| Salt spray | On the hardware lot, before setting | A finish failure is a replacement | 3-5 working days |
| Finished piece testing | On a drawn piece at final inspection | Confirms the build, not the material | 5-7 working days |
The sequencing is worth stating plainly because it is the part most often got wrong. Testing ordered after the final inspection produces reports about material that has already been cut, closed and packed, and a failure at that point is not a correction but a recall. Testing ordered on day one of sampling costs the same and is instead a decision about which lot to use.
Question Six: Who Pays, and What Does a Report Prove?
Who pays is a commercial term and belongs in the order. What the report proves is narrower than most buyers assume: it proves that the sample described in it passed the test named in it, on the date it was tested. It does not prove that the lot is the same as the sample unless the lot identity is recorded on the requisition, and it does not prove anything about the next lot.
State the hide lot, the finishing batch and the hardware lot on the test requisition, not the style name. A report is about the sample, and the sample has to be traceable to the lot.
The programme runs through our validated partner factory Quanzhou Yingming Bags, an SGS-validated site with 7 production lines and about 200,000 pcs per month of capacity, holding export experience since 2014. Sampling takes 6-10 working days, or 12-15 on a complex build; bulk occupies 35-50 days; minimums sit at 500 pcs per style and colourway; and shipments leave FOB Xiamen with FOB, CIF and DDP terms available.
Reading a Test Report: Limits, Units and Pass Criteria
A report has four parts that matter, and they are read in this order. The sample description, which tells you what was tested. The standard reference, which tells you how. The result with its unit, which tells you the number. And the limit or requirement, which tells you what the number had to beat. Anything reported without a unit is not a result, and anything reported without a limit is not a pass.
Four parts of a report, read in order
- Sample description, tied to the hide lot and finishing batch. Standard reference, ISO or otherwise. Result with a unit, such as newtons per 10 mm or mg per kg. Limit or requirement, stated on the report rather than assumed.
Three habits make reports useful rather than decorative. The first is to read the sample description before the result, because a pass on the wrong sample is the commonest failure in a testing programme. The second is to keep reports against the order and the lot rather than in a folder by date. The third is to re-test whenever a lot changes, since a report is a statement about one sample on one date. First, keep them against the order and the lot rather than in a folder by date, so a question raised a season later can be answered without a search. Second, read the sample description before the result, because a pass on the wrong sample is the commonest and least noticed failure in a testing programme.
What Testing Does Not Prove Either
Testing has its own blind spots, and they are the mirror of inspection's. It says nothing about whether 500 pieces were made consistently, because it examines material rather than output. It says nothing about whether the piece looks and feels right, which is the entire purpose of the bench. And it says nothing about traceability, which is a document evidenced through Leather Working Group tannery audits rather than a measurement.
The two therefore have to be run together, and the combination is what a designer programme needs: inspection to decide whether the lot leaves, testing to decide whether the material behind it was ever right, and documents to say where the material came from. Missing any one of the three leaves a gap that only shows itself once a piece is on a shelf.
Combining Testing and Inspection on One Programme
A workable combination fits inside the existing schedule. During the 6-10 working days of sampling window, swatches go for physical and chemical testing on day one and the pre production conformance check runs on day two. At 20-30 per cent complete, the bench compares five pieces against the approved sample. At 100 per cent packed, the AQL 2.5 draw is taken and, where required, a finished piece is tested as well.
Budgeted together, the testing provision and the tightened inspection plan with its re-work reserve come to roughly USD 4.80 per unit on a designer run. Against it sits what either one alone would miss: a non-compliant material that inspection cannot see, or an inconsistent lot that testing cannot describe. Neither is a substitute for the other.
Build a testing and inspection plan for your run
Send drawings, material direction, quantity per colourway, target market and delivery date. You will receive the test list, standards and limits for your programme. Request a quote.
Frequently Asked Questions
Why is laboratory testing needed if an AQL inspection passes?
Because the two answer different questions. An AQL 2.5 plan counts visible faults on a drawn sample; testing measures what a loupe cannot see, such as finish adhesion in newtons, a restricted amine in mg per kg, or plating thickness in micrometres.
Which physical tests should be specified on a handbag?
Tensile strength to ISO 3376, tear resistance to ISO 3377, finish adhesion to ISO 11644, flexing resistance to ISO 5402 and colour fastness to rubbing to ISO 105-X12, read on a grey scale at 4-5 dry and 4 wet.
Which chemical tests apply in the European market?
Chromium VI, certain azo dyes, nickel release from metal in prolonged skin contact and certain phthalates, all under REACH Annex XVII, plus California Prop 65 obligations where the piece is sold in that market.
What is the REACH limit for chromium VI in leather?
It is expressed as 3 mg per kg, tested to ISO 17075. The substance is a tanning by-product, so a result traces to the tannery and its lot rather than to the bench that worked the hide.
What is the limit for azo dyes?
30 mg per kg for each listed aromatic amine that a restricted azo dye can release. It is relevant wherever a dyed shell or lining is specified in a strong colour, and it is set by regulation rather than by preference.
When should testing be ordered?
On day one of the 6-10 working days of sampling window, on swatches from the hide lot and finishing batch the run will use. Reports take 5-7 working days, and a result arriving after cutting is a result about material already spent.
How is hardware tested?
Plating thickness by X-ray fluorescence, at 0.15-0.3 µm on brass, and corrosion resistance by salt spray to ISO 9227 for 24 hours on a standard specification and 48 on a high-wear one, recorded against the lot.
What should be stated on a test requisition?
The hide lot, the finishing batch and the hardware lot, rather than the style name. A report is about the sample described in it, and unless the sample traces to the lot the result cannot be applied to the run.
How long does a test report take?
Typically 5-7 working days for physical and chemical tests, 2-3 for plating thickness and 3-5 for salt spray. Sequencing them into the sampling window rather than after it is what makes them useful.
Does a pass on one lot cover the next one?
No. A report proves that the named sample passed on the date it was tested. The next hide lot or plating bath is a different sample, and a programme that reuses reports across lots is not testing at all.
What does testing not tell you?
Whether 500 pieces were made consistently, how the piece looks and feels, or where the material came from. Those are a bench discipline, an inspection question and a document respectively.
What does the combined provision cost?
Roughly USD 4.80 per unit on a designer run, covering the testing provision and the tightened inspection plan with its re-work reserve. Either one alone leaves a gap that only appears once a piece is on a shelf.
People Also Ask
Is testing a substitute for pre shipment inspection?
No. Testing examines material, inspection examines output. A compliant hide can still be assembled badly, and a well assembled piece can still carry a restricted substance above limit.
Can one test report cover several colourways?
Only if the swatches came from the same hide lot and finishing batch. Colour is usually a different batch, so each colourway needs its own requisition even when the style is identical.
Why is the sample description read before the result?
Because a pass on the wrong sample is the commonest failure in a testing programme. The result is meaningless if the specimen described does not trace to the lot that was used.
Should a finished piece ever be tested?
Occasionally, at final inspection, to confirm the build rather than the material. Routine testing belongs on swatches taken before cutting, where a failure is a decision rather than a recall.
How are test reports stored?
Against the order number and the lot identity rather than by date. A question raised a season later is answered in an afternoon if the report traces to the lot, and not at all if it does not.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- SGSSGS Third-party testing and inspection body whose reports cover the physical and chemical tests described above.
- ISO - International Organization for StandardizationISO Publisher of ISO 3376, ISO 3377, ISO 11644, ISO 5402, ISO 105-X12, ISO 17075 and ISO 9227.
- European Chemicals AgencyECHA Administrator of REACH, whose Annex XVII sets the restrictions on chromium VI, azo dyes, nickel release and phthalates.
- California Office of Environmental Health Hazard AssessmentOEHHA Administers Proposition 65, the separate Californian list with its own warning obligations for the substances named above.