Best Premium Handbag Production Capabilities for Brands: A Checklist With a Reason Beside Every Line
Which capabilities should a brand look for in a premium handbag production programme? Nine, in order of consequence: material sourcing with lot traceability, structured and soft construction on the same site, hardware in both stock and bespoke form, edge and skiving discipline, a development window that produces a real technical pack, per-lot compliance testing, an inspection plan agreed before cutting, presentation and packing, and logistics on named trade terms. Each capability below carries the reason it earns its place, because a capability list without reasons is just a brochure. The programme described runs across 7 production lines with about 200,000 pcs per month of capacity and export experience held since 2014.
The Capability Checklist, With a Reason Beside Each Line
Capability claims are easy to write and hard to verify, so the useful version of this list pairs each item with what it actually prevents. A house that can source a named calfskin lot prevents shade drift at the re-order; one that can prove a lock prevents a closure that drifts in tolerance across panels. The list below is ordered by how expensive the absence of each capability becomes.
- Material sourcing with lot traceability, because a report and a shade both name a lot.
- Structured and soft construction on one site, because a body rarely stays in one category.
- Hardware in stock and bespoke form, because tooling is a calendar decision as well as a cost.
- Skiving and edge discipline, because those two decide whether a corner survives a season.
- A development window producing a real technical pack, because everything later is measured against it.
- Per-lot compliance testing, because a report names the lot and the market it was issued for.
- An inspection plan agreed before cutting, because an audit negotiated at handover costs more.
- Presentation and packing, because packaging is part of how a buyer receives the bag.
- Logistics on named trade terms, because FOB, CIF and DDP allocate risk differently.
Capacity in Context: 7 Lines and About 200,000 Pcs a Month
Capacity numbers are only meaningful next to the commitment they serve. The programme runs across 7 production lines with about 200,000 pcs per month of capacity, against a MOQ of 500 pcs per style and colourway. Read together, those two figures say what the site is built for: repeatable runs at capsule scale rather than either one-off pieces or mass volume.
Reading a capacity figure properly
- Lines indicate parallel breadth: several styles can run at once without one blocking another.
- Monthly capacity indicates headroom, not a promise about your own delivery date.
- MOQ 500 pcs per style and colourway is the unit of commitment that capacity is organised around.
- Bulk of 35-50 days is the gate that actually governs your date, far more than capacity does.
- Export experience held since 2014 is the least glamorous and most useful line on the list.
The honest reading is that capacity matters less than most brands assume. A date is usually governed by material arrival, sampling and bulk intervals, and a larger site does not shorten any of those. What capacity protects is the ability to run a second style without displacing the first.
Material Capability: From Calfskin to Listed Skins
Material capability is measured by what a house can reserve, document and cut, not by what it can name. Full-grain calfskin at 1.2-1.4 mm, vegetable-tanned vachetta at 1.4-1.8 mm, corrected-grain bovine, suede and nubuck, and listed skins where permit documents can be produced: each needs a different handling discipline and a different set of papers.
| Capability | What it should include | Why the brand cares |
|---|---|---|
| European calfskin lots | Tannery named, lot reserved, certificate checked | One lot per colourway removes shade drift at re-order |
| Vegetable-tanned vachetta | Patina sampled before commitment | Handles and trims darken differently from panels |
| Corrected-grain and coated | Finish adhesion checked to ISO 11644 per lot | Coating lift is the commonest interior failure |
| Suede and nubuck | Nap direction controlled across panels | Reversed nap reads as a different colour on the shelf |
| Listed skins | CITES documents reconciled with the invoice | Permits run on an authority's calendar, not yours |
One further material capability is worth asking about separately, because it is omitted from most lists: what happens to offcuts. A house that records how much of a hide becomes panels, and what happens to the remainder, is a house that understands yield. Offcut discipline is not an environmental claim so much as a marker of cutting care, and it correlates closely with whether structural panels come from the shoulder rather than the belly.
Construction Capability: Structured, Soft and Framed
A brand rarely stays in one construction category, so the useful capability is range rather than specialisation. A structured body needs panel substance at 1.2-1.4 mm and reinforcement at 0.8 mm under the base; a soft body needs folds skived to 0.6-0.8 mm and a turned edge; a framed body needs a closure proved before panels are cut to it. Each is a different set of bench skills.
- Structured: panel substance 1.2-1.4 mm, reinforcement board at 0.8 mm, top line stiffener sized to the opening.
- Soft: skive width 8-10 mm, adhesive open time 8-12 minutes, press dwell 15-20 seconds at the fold.
- Framed: closure proved for at least 5,000 cycles before any panel is cut to it.
- Lined and gusseted: lining cut to the same tolerance as the exterior, not merely to fit.
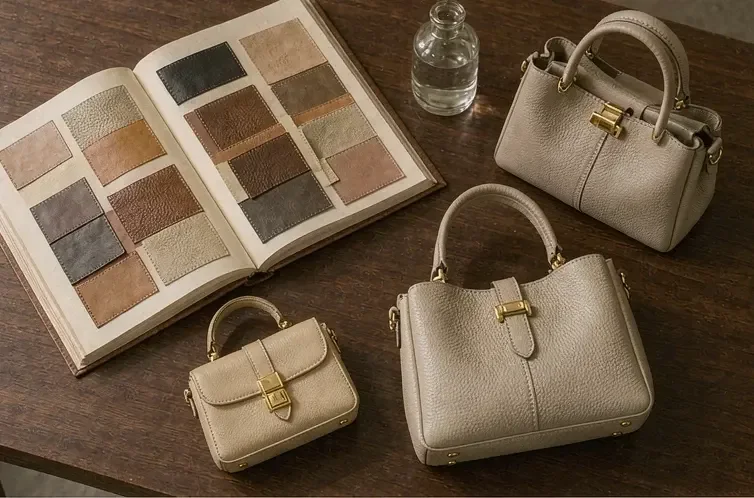
Hardware Capability: Stock, Bespoke and Proving
Hardware capability has two halves that are often confused. Sourcing covers stock brass arriving in 20-25 working days; development covers bespoke tooling at 30-40 working days including the proving step. A house that can only do the first will quietly steer every design towards its catalogue, which is worth knowing before the closure is chosen.
Stock sourcing
Catalogue brass at 0.15-0.3 µm plating, arriving in 20-25 working days. Enough for most first capsules, and it lets the body be proved before any tooling is committed.
Bespoke development
Tooling at 30-40 working days, a proving step on the bench, then a second sample. Best deferred to a later drop, when the tooling charge amortises across a larger run.
Finish consistency
One finish family across feet, rings, strap ends and the closure, checked against a signed reference component at intake so substitution is caught before fitting.
Finishing Capability: Edge, Skiving and Stitch
Finishing is where capability shows on a fiftieth unit rather than on a first one. Edges built from three coats of roughly 0.12 mm, cured and sanded between passes; folds skived to 0.6-0.8 mm over an 8-10 mm width; structural seams at 8-9 stitches per inch with a bonded thread around 0.45 mm. All three are measurable, which is what distinguishes a capability from a claim.
- Edge build
- Three coats of about 0.12 mm, cured and sanded between passes
- Skiving
- 0.6-0.8 mm at folds over an 8-10 mm skive width
- Stitch density
- 8-9 per inch on structural seams, 9-10 on handles and straps
- Thread
- Bonded filament around 0.45 mm, matched in shade to the lot
- Final inspection
- Every unit finished and examined before packing, not sampled after it
Development Capability: Pack, Toile and Sampling
Development capability is the one most often overstated, because sampling is easy to offer and a technical pack is hard to write. The window is 6-10 working days on a standard build and 12-15 on a complex one, and what it should produce is a measured sample, a written correction list, one corrected round and a pack that records tolerances. Without the pack, the sample is only a photograph.
- Dimensioned drawings reviewed and, where necessary, corrected against what the bench can build.
- Pattern graded and a calico toile fitted, usually two toiles on a structured body.
- First built sample measured against the pack rather than against an impression.
- Written correction list, numbered and priced, so each change lands at the right gate.
- Corrected round built to the corrected pack, then the spec freeze and a counter sample.
Compliance and Documentation Capability
Compliance capability means knowing which reports to book, against which lot, for which market, and doing it early enough to matter. REACH Annex XVII applies to articles placed on the EU market, California Prop 65 governs listed substances for the United States, EU Regulation 1007/2011 governs fibre naming, and CITES documents apply wherever a listed skin is used.
- Reports are issued per lot and per market, so both must be named at quotation.
- Testing is booked when the lot is named, not when the goods are finished.
- Tannery certificates should name the tannery itself under the Leather Working Group protocol.
- Shipping documents must reconcile with permit paperwork wherever a listed skin is involved.
Presentation and Logistics Capability
The last two capabilities are unglamorous and routinely underestimated. Presentation covers the rigid box, dust bag and tissue that add roughly USD 4.80 per unit, and packing that survives freight. Logistics covers the trade term: FOB Xiamen by default, with CIF and DDP available on request, each allocating freight risk and customs paperwork differently.
- Presentation packaging: around USD 4.80 per unit, settled once the unit cost is known.
- Packing: carton specification and unit count agreed before audit, not after it.
- Trade terms: FOB Xiamen by default, fixed at quotation rather than adjusted at handover.
- Documents: packing list, invoice and any permit paperwork reconciled before collection.
What the Checklist Does Not Tell You
A capability list describes what a programme can do, not how it will behave when something goes wrong. The two questions worth asking alongside it are what happens to a rejected batch, and how a correction is recorded. A house that re-checks corrections and records them against the operation that caused them will improve next season; one that replaces units and counts them will repeat the defect.
It is also worth asking what the programme is not set up for. Ours is built around MOQ 500 pcs per style and colourway with sampling at 6-10 working days and bulk at 35-50 days, carried out through our validated partner factory Quanzhou Yingming Bags, an SGS-validated site. A single showpiece, or a run of thirty units, is better placed on an atelier bench, where bench hours rather than line days set the pace and hand saddle stitching at 6-7 per inch replaces a machine seam at 8-9. The third question, then, is whether the programme will tell you when it is the wrong fit, which is a better sign than any capability it might claim.
Check your brief against the nine capabilities
Send your drawings, material direction and quantity per colourway. You will receive the nine capabilities applied to your brief, with anything missing marked, within two working days. Request a quote.
Frequently Asked Questions
What capacity should a premium handbag programme have?
Enough to run more than one style without displacing another. Ours runs across 7 production lines with about 200,000 pcs per month of capacity, organised around MOQ 500 pcs per style and colourway. Capacity matters less than brands assume, though: a delivery date is governed by material arrival, sampling and bulk intervals.
Why does MOQ apply per colourway rather than per style?
Because each colourway needs its own reserved lot, its own cutting run and its own inspection lot. A launch of one body in three colourways is three commitments of 500 pcs. That structure is what keeps shade consistent, since one lot covers one colourway rather than being split between several.
Can one programme handle both structured and soft bodies?
It should, because a collection rarely stays in one category. Structured work needs panel substance at 1.2-1.4 mm and reinforcement at 0.8 mm; soft work needs folds skived to 0.6-0.8 mm and a turned edge. Those are different bench skills and worth confirming before a mixed capsule is committed.
Does the programme offer bespoke hardware?
Yes, in two forms. Stock brass at 0.15-0.3 µm plating arrives in 20-25 working days, and bespoke tooling takes 30-40 including proving. Most first capsules prove the body on stock components and commission bespoke closures for a later drop, when the tooling amortises across more units.
What finishing values should a programme be able to hold?
Edges in three coats of roughly 0.12 mm cured and sanded between passes, folds skived to 0.6-0.8 mm over an 8-10 mm width, structural seams at 8-9 stitches per inch, and a bonded thread around 0.45 mm. All four are measurable, which is what separates a capability from a claim.
How long does the development stage take?
Six to ten working days for a standard build and 12-15 for a complex one. The window should produce a measured sample, a written correction list, one corrected round and a technical pack recording tolerances. A sample without a pack is only a photograph of an intention.
Which materials can be sourced?
Full-grain calfskin at 1.2-1.4 mm, vegetable-tanned vachetta at 1.4-1.8 mm, corrected-grain bovine, suede and nubuck, and listed skins where permit documents can be produced. The capability that matters in each case is documentation: a named lot with a certificate can be tested and repeated.
How is compliance handled across several markets?
Per lot, per destination market. REACH Annex XVII applies to the EU, California Prop 65 to the United States, EU Regulation 1007/2011 governs fibre naming, and CITES documents apply to listed skins. Because reports name a lot and a market, both should be stated at quotation.
What does presentation packaging cost and include?
Around USD 4.80 per unit for a rigid box with dust bag and tissue, before freight and duty. Carton specification and unit count are agreed before audit rather than after it, since packing that fails in transit is a defect no amount of finishing can compensate for.
Which trade terms are available?
FOB Xiamen by default, with CIF and DDP available on request. The term decides who carries freight risk and who prepares customs documentation, so it should be fixed at quotation. Changing it at handover re-prices the shipment entirely.
What inspection is included at the end of a run?
AQL 2.5 under ISO 2859-1, agreed before cutting. On a 500 pcs lot at general inspection level II the plan draws 50 units, accepting 3 and rejecting at 4. Defects are classified as critical, major and minor in advance, and third-party inspection can be arranged alongside it.
What is the programme not suited to?
Single showpieces and very small runs. MOQ 500 pcs per style and colourway, sampling at 6-10 working days and bulk at 35-50 days describe a repeatable capsule programme, not a one-off. A couture body or a thirty-piece order is better placed on an atelier bench.
People Also Ask
What capabilities matter most in a handbag production programme?
Material sourcing with lot traceability, construction range across structured and soft bodies, hardware in stock and bespoke form, measurable finishing discipline, and a development stage that produces a real technical pack.
How much capacity does a handbag programme need?
Enough to run two styles at once without one displacing the other. Capacity protects breadth; the delivery date is governed by material arrival, sampling at 6-10 working days and bulk at 35-50 days.
Why is lot traceability considered a capability?
Because a test report and a shade both name a lot. A programme that can reserve and document one lot per colourway removes drift at re-order and avoids the second testing cycle that follows any material substitution.
Should a first capsule use bespoke hardware?
Usually not. Tooling adds 30-40 working days and amortises poorly across 500 pcs. Proving the body on stock brass first and commissioning the closure for the second drop is normally the better sequence.
What should a capability claim be verified against?
Numbers rather than adjectives. Ask for plating in microns, skive thickness in millimetres, stitch count per inch and the inspection code letter. A capability that cannot be stated as a number has not really been defined.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- ISO - International Organization for StandardizationISO Publisher of ISO 2859-1 for inspection sampling, ISO 11644 for finish adhesion and ISO 9227 for salt spray on plated components.
- Leather Working GroupLeather Working Group Tannery audit protocol referenced when a calfskin lot is reserved; the certificate should name the tannery itself rather than an agent.
- ECHA - European Chemicals AgencyEuropean Chemicals Agency Administrator of REACH, whose Annex XVII restrictions apply to leather articles placed on the EU market.
- CITES - Convention on International Trade in Endangered SpeciesCITES Appendix listings determine the permit documents required where a listed skin is used in a design.
- Sourcing JournalSourcing Journal Reporting on production capacity, hardware sourcing and lead times across the leather goods supply chain.