8 Things to Check on a Premium Handbag Production Floor: A Buyer's Walkthrough in Eight Questions
What should a buyer check when walking a premium handbag production floor? Eight things, in this order: whether the material lot is named and held, how the cutting marker is built, whether folds are skived, the stitch count on a structural seam, how many coats build an edge, where hardware waits before fitting, whether the inspection plan was agreed before cutting, and whether corrections are re-checked or merely counted. Each check takes under five minutes and each one corresponds to a decision that is expensive to reverse later. Answered in sequence below, with the bench values worth holding and the reason each check sits where it does in the walk.
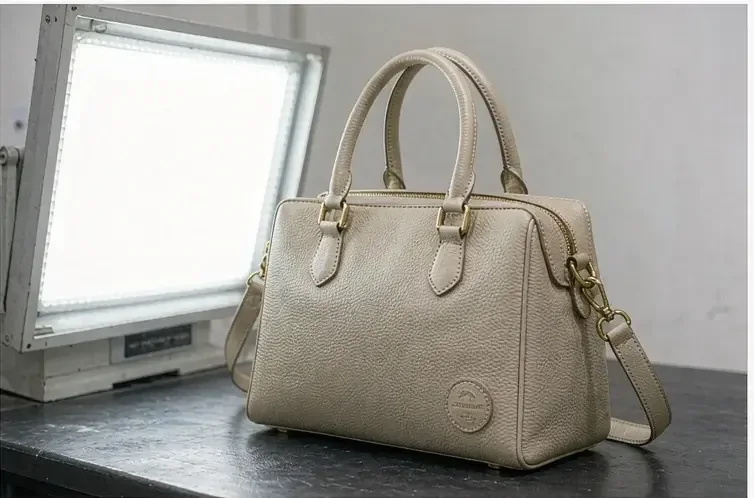
One: Is the Material Lot Named and Held?
The first check is documentary rather than physical, and it is the one that decides everything downstream. Ask which lot the leather came from and whether one lot covers the whole colourway, because a run drawn from two dye lots will show shade drift that no finishing technique can hide. A named lot should be traceable to a tannery certificate, and where the tannery is audited under the Leather Working Group protocol the certificate should name the tannery itself rather than an agent.
- Ask for the lot reference and the tannery name, then check that both appear on the pack.
- Confirm the lot covers the full colourway quantity, since topping up mid-run is how drift begins.
- Check the arrival record: a newly named European lot takes 15-20 working days to reach the bench.
- Ask whether compliance reports for the destination market were booked against that specific lot.
Two: Is the Cutting Marker Built for Yield or for Speed?
The second check is the marker, and it reveals more about a house than any showroom. A marker built for yield places panels around the natural shape of the hide and reaches roughly 78-85% utilisation; a marker built for speed runs panels in straight bands and quietly wastes material. Yield matters commercially because it sets the hide requirement, and it matters aesthetically because panels taken from the belly of a hide behave differently from panels taken from the shoulder.
Bench values to hold at the cutting table
- Marker utilisation: around 78-85% on a structured body in full-grain calfskin.
- Panel placement: structural panels taken from the shoulder and back, not from the belly.
- Direction: nap and grain direction consistent across all panels of one unit.
- Substance check: 1.2-1.4 mm before skiving, read at several points on the panel.
- Grading: each size step changes panel area by roughly 8%, which shifts yield per size.
The reason this check sits second is that it is the last point at which a material problem is still inexpensive to put right. Once panels are cut, every subsequent operation adds value to a piece that may already be wrong, which is why a floor that cuts first and checks later produces expensive corrections.
Three: Are Folds Skived, or Simply Folded?
The third check is tactile and takes ten seconds. Run a thumb along a fold: a premium fold tapers to 0.6-0.8 mm over a skive width of 8-10 mm, while a fold left at full substance steps and stands proud at the corner. Skiving is not cosmetic, because a double-thickness corner resists closing, wears at the edge finish from the inside, and eventually telegraphs through the surface as a ridge.
- Skive width of 8-10 mm gives a taper the hand reads as gradual rather than as a step.
- Fold thickness of 0.6-0.8 mm means two panels meeting at a corner make one thickness.
- Adhesive open time of 8-12 minutes before closing, so the bond has taken rather than slipped.
- Press dwell of 15-20 seconds at the fold, which is a gate rather than a habit.
Two conditions on the floor govern whether a skive holds: room humidity and adhesive discipline. A bench kept at roughly 50-60% relative humidity keeps leather at a stable moisture content, so a panel skived in the morning behaves the same way when it is closed in the afternoon. Adhesive applied outside its 8-12 minute open time either skins over or stays wet, and both produce a fold that lifts months later rather than immediately.
Four: What Is the Stitch Count on a Structural Seam?
The fourth check is arithmetic: count the stitches in one inch of a structural seam. Premium work runs 8-9 per inch with a bonded thread around 0.45 mm in diameter and a needle sized to match, commonly a 90/14 on calfskin. Standard work runs 6-7 per inch with a thicker thread that fills the needle hole instead of closing the seam, and the difference appears when the bag is overfilled rather than on the shelf.
- Structural seam
- 8-9 stitches per inch, tolerance ±0.5 per inch
- Handles and straps
- 9-10 stitches per inch, since they carry the load of the whole bag
- Thread
- Bonded filament around 0.45 mm in diameter, matched in shade to the lot
- Needle
- 90/14 on calfskin at 1.2-1.4 mm, changed on a set schedule rather than when it breaks
- Backstitch
- Present at the start and end of every run, and inspected specifically
Needle discipline is worth watching while you are there. A needle that is changed on a schedule produces clean holes; one that is run until it breaks produces torn fibre at the seam line, which is invisible on day one and visible as a frayed run within a season of being carried.
Five: How Many Coats Build the Edge?
The fifth check separates a finish that lasts from one that photographs well. Ask how many coats build the edge and how long each cures: three coats of roughly 0.12 mm, sanded between passes, is the premium answer. A single heavy pass looks acceptable under showroom light and then hairlines at the corner, because a thick film cannot follow the leather flexing beneath it.
- Three coats of about 0.12 mm each, sanded and re-checked between passes.
- A curing interval between coats that is treated as a gate rather than as a preference.
- Corners radiused so the film has no sharp turn to bridge.
- Edge shade matched to the lot rather than to a standard swatch card.
Six: Where Does Hardware Wait Before It Is Fitted?
The sixth check is about staging, and it catches the substitution that causes most late disputes. Components should arrive with a record, wait in a identified place, and be compared against a signed reference from the approved sample before fitting. Plating of 0.15-0.3 µm, proved at 24 hours of neutral salt spray under ISO 9227, is a measurable target; a finish name is not.
Component intake
Recorded against the purchase order and compared with the signed reference component. A component that arrives without a record is the one most likely to be substituted on the next run.
Proving on the bench
A turn-lock is cycled at least 5,000 times before panels are cut to it, since a closure that drifts in tolerance makes every subsequent panel fit badly.
Finish family
Feet, rings, strap ends and the closure share one finish so the bag reads as a single object rather than as assembled parts.
Seven: Was the Inspection Plan Agreed Before Cutting?
The seventh check is a question about timing rather than about rigour. A plan drawn at AQL 2.5 under ISO 2859-1 before cutting changes behaviour upstream, because the bench knows what the end of the run will be measured against. A plan discussed after the goods are finished is a negotiation, and negotiation at handover is always more expensive than measurement at intake.
| Lot size | Code letter at level II | Units drawn | Accept | Reject |
|---|---|---|---|---|
| 500 pcs | H | 50 | 3 | 4 |
| 1,200 pcs | J | 80 | 5 | 6 |
| 3,200 pcs | K | 125 | 7 | 8 |
| 10,000 pcs | L | 200 | 10 | 11 |
Also ask how defects are classified. Critical, major and minor should be defined before inspection rather than during it, because a classification agreed at the moment a defect is found is simply a negotiation conducted under time pressure.
Eight: Are Corrections Re-Checked or Merely Counted?
The eighth check is the one almost nobody asks, and it is the best predictor of whether the next run will be better. A floor that re-checks corrections and records them against the operation that caused them improves; a floor that counts corrections and packs the replacements repeats the same defect next season. Ask to see the record for the last rejected batch.
- Corrections are re-checked, not merely replaced, before the lot is released.
- Records name the operation rather than the individual, so the cause can be addressed.
- Rejected units are quarantined in a defined place, not returned to the line informally.
- The re-check result is recorded with the lot, which makes a later dispute resolvable on evidence.
What to Do With What You Saw
A walkthrough is only worth the record made during it. Write down the eight answers on the day, compare them with what the quotation promised, and raise any gap while the run is still in progress rather than at handover. Most disagreements that reach a lawyer began as a note someone did not write on a walkthrough.
- Record the lot reference, the marker utilisation and the skive reading as numbers, not impressions.
- Photograph the seam, the edge and the hardware reference under the same light each visit.
- Note the inspection plan and the defect classification, and confirm both in writing.
- Ask for the correction record of the last rejected batch before you leave the floor.
One further habit separates a useful walkthrough from a social one: ask the floor to state each value before you reveal what you expected it to be. A number given first is a number the house actually holds; a number confirmed after you have suggested it is worth very little. The same applies to the inspection plan, which should be quoted from the pack rather than recalled from memory.
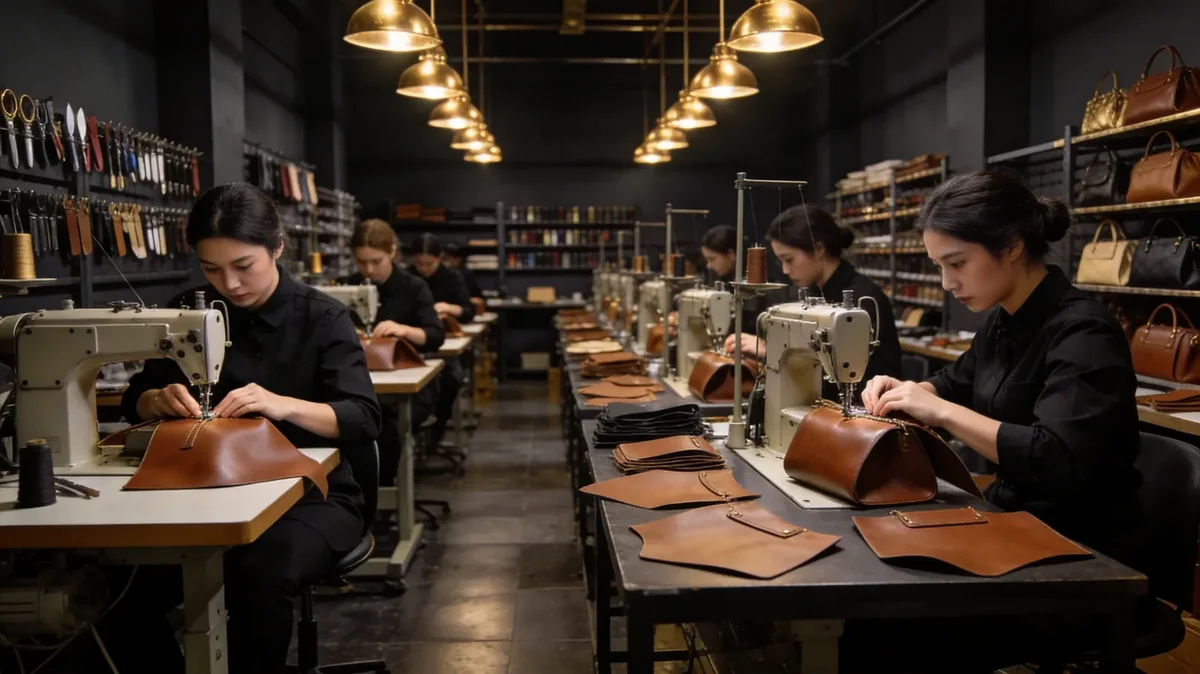
On our own programme these eight checks sit inside a run of 7 production lines with about 200,000 pcs per month of capacity and export experience held since 2014, carried out through our validated partner factory Quanzhou Yingming Bags, an SGS-validated site. Sampling takes 6-10 working days, bulk 35-50 days, and third-party inspection can be added alongside the internal AQL 2.5 audit.
Walk the floor before you commit the run
Send your drawings and quantity per colourway and we will walk you through these eight checks on a live run, on video or in person, before any deposit is discussed. Request a quote.
Frequently Asked Questions
What is the single most useful check on a production floor walk?
Whether the material lot is named and held for the whole colourway. That one answer determines shade consistency, whether compliance reports are valid, and whether a re-order will match the launch drop. It is documentary rather than physical, which is why it is often skipped in favour of looking at stitching.
How is cutting yield measured?
As marker utilisation, typically 78-85% on a structured body in full-grain calfskin. It is calculated from the panel area placed against the usable hide area. Yield matters twice: it sets how much hide the run needs, and it determines whether structural panels come from the shoulder rather than the belly.
Why does skiving matter on a fold?
Because an unskived fold carries double substance at the corner. That resists closing cleanly, wears the edge finish from the inside outward, and eventually shows through the surface as a ridge. Skiving to 0.6-0.8 mm over an 8-10 mm width lets two panels meet as one thickness.
What stitch count should I expect on a structural seam?
Eight to nine stitches per inch with a bonded thread around 0.45 mm in diameter, rising to 9-10 per inch on handles and straps. Below about 7 per inch the seam opens under load and shows daylight at the corner, which is exactly where structured bodies fail first.
How many coats should build a premium edge?
Three, each roughly 0.12 mm, cured and sanded between passes. A single heavy coat photographs acceptably and then hairlines within a season, because a thick film cannot flex with the leather beneath it. Corners should also be radiused so the film has no sharp turn to bridge.
How should hardware be checked before fitting?
Against a signed reference component kept from the approved sample, with the plating thickness stated in microns, typically 0.15-0.3 µm, and proved at 24 hours of neutral salt spray under ISO 9227. A finish name is not a measurement, and substitution is invisible until the component wears.
When should the inspection plan be agreed?
Before cutting begins. A plan drawn at AQL 2.5 under ISO 2859-1 shapes behaviour on the bench, while one discussed after the goods are finished becomes a negotiation. Defect classification into critical, major and minor should also be fixed in advance rather than at the moment a defect appears.
What sample size does AQL 2.5 draw on a 500 pcs lot?
At general inspection level II the code letter is H: 50 units drawn, accept 3, reject 4. At 1,200 units the plan moves to code letter J with 80 units drawn, accept 5, reject 6. The lot size fixes the plan, which is why quantity per colourway should be settled early.
Why ask to see the correction record?
Because it predicts the next run. A floor that re-checks corrections and records them against the operation that caused them improves season on season. One that counts corrections and packs replacements repeats the same defect, since nothing upstream has actually changed.
How long should a floor walkthrough take?
About two hours for the eight checks, assuming a run is in progress. Anything under an hour usually means the documentary checks were skipped, and those are the ones that decide shade consistency, compliance validity and whether a re-order matches.
What should be recorded during the walk?
Numbers rather than impressions: the lot reference, marker utilisation, skive reading, stitch count, coat count and the inspection plan. Photograph the seam, edge and hardware reference under the same light each visit so two runs can be compared honestly.
Which standards back these eight checks?
ISO 2859-1 for the sampling plan, ISO 9227 for salt spray on plated components, ISO 105-X12 for rubbing fastness, ISO 11644 for finish adhesion and ISO 3376 for tensile behaviour. Reports are issued against a named lot rather than against a material family.
People Also Ask
How do you audit a handbag production floor?
Walk it in sequence: lot records, cutting marker, skiving, stitch count, edge build, hardware staging, inspection plan and correction records. Each check takes minutes and each maps to a decision that is expensive to reverse once panels are cut and value has been added.
What is a good cutting yield for leather panels?
Around 78-85% for a structured body in full-grain calfskin. Below that the marker is being run for speed rather than for yield, which raises hide requirements and pushes structural panels towards the belly of the hide where the fibre is looser.
Why do seams matter more than surface finish?
Because a seam cannot be finished into looking better than it is. Stitch density, thread diameter and needle condition decide whether a seam holds under load or opens at the corner, and the failure appears months after approval rather than on the showroom table.
What is AQL 2.5 in plain terms?
A sampling plan under ISO 2859-1 that fixes how many units are drawn from a lot and how many defects are acceptable. On a 500 pcs lot at level II, 50 units are drawn with 3 accepted and 4 rejected, so roughly one unit in ten is examined.
Should corrections be re-checked after repair?
Yes. A correction that is replaced but not re-checked hides the operation that caused it, and the defect returns on the next run. Recording the cause against the operation is what makes the following season better rather than merely compliant.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- ISO - International Organization for StandardizationISO Publisher of ISO 2859-1 sampling plans, ISO 9227 salt spray testing, ISO 105-X12 rubbing fastness, ISO 11644 finish adhesion and ISO 3376 tensile behaviour.
- Leather Working GroupLeather Working Group Tannery audit protocol; the certificate scope checked during the first walkthrough should name the tannery itself rather than an agent.
- ECHA - European Chemicals AgencyEuropean Chemicals Agency Administrator of REACH, whose Annex XVII restrictions apply to leather articles and are tested against the named lot.
- California Proposition 65Office of Environmental Health Hazard Assessment The California substance list governing goods sold into the United States, booked per destination market before bulk intake.
- Sourcing JournalSourcing Journal Reporting on audit practice, component substitution and inspection standards across apparel and leather goods sourcing.