How Much Should a Luxury Handbag Programme Cost: Three Specifications Compared Line by Line
How much should a luxury handbag programme cost per unit? The honest answer is a structure rather than a number: material carries 45-60% of unit cost, hardware 8-18%, bench labour 15-25%, and compliance and documentation a further 3-6%. What moves the total is not negotiation but specification — hide grade, plating thickness, whether the edge is hand-finished in three coats, and how much tooling has to be amortised across 500 pcs. Below, three specifications of one silhouette are set side by side so you can see which line actually decides the price.
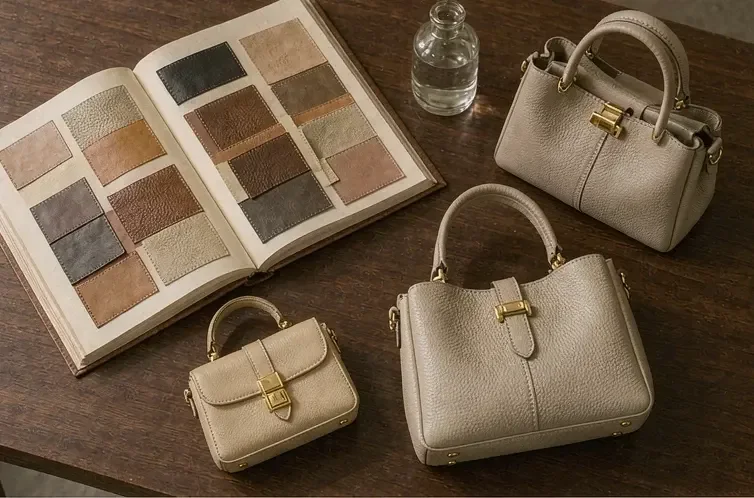
One Silhouette, Three Specifications
Ask three houses what a structured top-handle bag costs and you will get three numbers, because they are not quoting the same bag. The silhouette is identical in all three cases below. What differs is the hide, the closure, the edge treatment and the volume over which tooling is spread, and those four decisions account for almost the whole spread between the quotes.
| Cost line | Specification A: accessible luxury | Specification B: house standard | Specification C: flagship |
|---|---|---|---|
| Shell material | Corrected-grain calf, 1.0-1.2 mm | Full-grain calfskin, 1.2-1.4 mm | Full-grain calfskin with an exotic facing panel |
| Lining | Polyester twill, stock colour | Cotton twill or microsuede | Lambskin or silk, dyed to match |
| Closure | Stock zamak turn-lock, 0.10-0.15 µm | Custom brass turn-lock, 0.15-0.3 µm | Sand-cast brass with a struck logo, 0.3 µm |
| Edge treatment | Two coats, machine-applied | Three coats, hand-sanded, 0.35-0.45 mm | Three coats with a hand-turned fold |
| Stitch density | 7-8 per inch, machine | 8-9 per inch, machine with hand finishing | 8-9 per inch with hand-stitched handle attachment |
| Interior | Two slip pockets | Three pockets, one zipped, reinforced base | Graded interior with a framed base and foot studs |
| Bench hours per unit | Roughly 1.5-2 | Roughly 3-4 | Roughly 6-8 |
Read down the columns rather than across the rows. The flagship specification is not the house standard plus a margin; it is a different object, with roughly triple the bench hours and a hardware development that has to be amortised across the run.
Material: The Line That Moves First
Material is the largest single line on a luxury handbag and the one over which a brand has the least control once a season begins. It carries 45-60% of unit cost, and within that line the decisions are hide grade, thickness, finish and yield. Yield is the quiet one: an exotic facing panel can produce a usable area well under half that of a calfskin skin of the same nominal size, so the same bag costs more to make simply because more skin is issued per unit.
- Full-grain calfskin at 1.2-1.4 mm is the reference material for a structured body and prices above corrected grain.
- Corrected grain carries a finish that hides surface faults, raising yield and lowering the material line.
- An embossed or saffiano finish adds a plate step, and a new plate adds a tooling line of its own.
- Listed skins add permit documentation and lower yield, and they are usually cut last for that reason.
- Dyed-to-match lots add a lab dip cycle of 7-10 days and a strike-off, both of which are charged.
The lever most founders miss is not the grade but the thickness band. Holding a specification at 1.2-1.4 mm rather than demanding a narrow band at the top of it gives the cutter more of each skin to work with, which lowers the issued area per unit without changing how the bag looks.
Hardware: A Small Part Carrying a Large Number
Hardware typically carries 8-18% of unit cost, and it is the line where a small component produces a surprisingly large effect. Three variables drive it: the base alloy, whether the part is stock or bespoke, and the plating thickness. A stock zamak turn-lock carries no tooling; a custom brass one carries a die, a proving step and a longer plating cycle.
- Stock zamak closure
- No tooling; plating around 0.10-0.15 µm; shortest lead time
- Custom brass closure
- Die and proving step; plating 0.15-0.3 µm; longer component calendar
- Sand-cast brass with struck logo
- Pattern and die, plus a second proving sample before panels are cut
- Plating thickness
- 0.15-0.3 µm is the band that survives 24 hours neutral salt spray to ISO 9227
- Amortisation
- A bespoke die spread across 500 pcs carries a visible per-unit share; across 3,000 pcs it becomes negligible
That last line is the whole argument for volume discipline. The same custom closure is genuinely costly on a first capsule of 500 pcs and genuinely modest on a third re-order. Brands that commit to a closure they intend to keep are effectively pre-paying the tooling across several seasons.
Bench Labour and the Hour Count
Labour carries 15-25% of unit cost and is the line most often misunderstood, because it is quoted as a rate when it should be read as hours. Bench hours per unit are the honest measure: roughly 1.5-2 for a simple structure, 3-4 for a house-standard build, and 6-8 where a hand-turned fold, a hand-stitched handle or a framed base is specified.
Machine closing, stock edge
Around 1.5-2 bench hours. The bag closes quickly and the edge is applied in two coats. Appropriate for an entry price point and for a style intended to be re-ordered unchanged for several seasons.
Machine closing, hand-finished edge
Around 3-4 bench hours. Three coats, each sanded back and cured, to a build of 0.35-0.45 mm. This is where most house-standard programmes sit, because the edge is the first thing a customer touches.
Hand-stitched attachments, framed base
Around 6-8 bench hours. Handle attachment stitched by hand, a framed or reinforced base, and foot studs. The hour count, not the material, is what defines a flagship specification.
Where a quotation gives a labour rate without an hour count, ask for the hours. A rate alone tells you nothing about the bag, and it is the single question that most reliably distinguishes a considered quote from a placeholder.
Development, Tooling and Pattern Costs
Development is the line that surprises first-time founders, because it is charged once and appears before any bag exists. It covers the technical pack, pattern making, a toile, and any tooling for closures, plates or frames. Sampling itself runs 6-10 working days for a standard build and 12-15 where a complex construction or a bespoke closure is involved.
- Pattern and toile: charged once per style, and reusable across colourways of the same body.
- Closure tooling: charged once per part, and the reason a bespoke lock is a multi-season decision.
- Emboss or deboss plate: charged once, then held for re-orders.
- Graded pattern sets: each additional size or proportion changes panel area by roughly 8%, shifting yield.
- Revisions after approval: charged when they change specification rather than correct an error.
The pattern is the asset in that list. It is the one development cost that keeps paying: a second colourway on an existing pattern carries no development line at all, which is why an expanded colourway is the most efficient first growth move a young maison can make.
Compliance, Testing and Documentation
Compliance and documentation carry 3-6% of unit cost and are almost always omitted from a first cost plan. They are also the line most likely to be demanded by a retailer at the worst possible moment, and they are issued against a lot, so they cannot be produced retrospectively once that lot is gone.
| Item | When it is incurred | What triggers it |
|---|---|---|
| REACH Annex XVII declaration | At material lot release | Selling into the European market |
| California Prop 65 declaration | At material lot release | Selling into California |
| CPSIA testing | Before first shipment | Goods sold into children's product channels |
| ISO 105-X12 rub fastness | At lot release, around 7-10 days | Pale shades, or a retailer requirement |
| ISO 3376 and ISO 3377-2 strength reports | At lot release | A marketplace or retailer technical file |
| Permit documentation | Before cutting | The presence of a skin listed in the CITES appendices |
| Documentation handling | Per lot file, from USD 4.80 | Assembly of the document set itself |
Book these when the lot is named. A capsule held at the port waiting for a certificate costs more in delayed shelf presence than the whole compliance line costs to run properly in the first place.
Freight, Duty and the Trade Term
Freight is not part of the unit cost on FOB Xiamen terms, and it should not be confused with it. What the term decides is who carries the volatile lines: ocean freight, marine insurance, import duty and destination handling. A quotation that bundles them looks higher on the unit line and hides a margin inside the freight estimate.
- A 500 pcs capsule at 12 units per carton produces roughly 42 cartons and ships as a less-than-container load.
- A less-than-container load carries a minimum charge plus a rate per cubic metre, so consolidation halves the fixed element.
- Import duty is set by classification in the destination market, not by the quotation, and it belongs on your side of the ledger.
- Marine insurance is placed by the buyer under FOB, ordinarily at 110% of invoice value.
- Documentation handling is quoted from USD 4.80 per shipment file and covers the papers, not the freight.
The practical consequence is that two quotations on different terms are not comparable on the unit line. Ask for the same bag on the same term before comparing anything, and if you are shipping more than twice a year, ask for FOB and price the freight yourself.
What Pushes a Quotation Up, and What Pulls It Down
Once the structure is visible, the levers are obvious and mostly unglamorous. None of them involve asking for a smaller number; all of them involve changing what is being specified or how it is sequenced.
- Increase volume per colourway. Tooling and development spread across more units, and MOQ 500 pcs per style and colourway is where that spreading begins.
- Keep the closure across seasons. A bespoke die amortised over several capsules stops being a line and becomes an asset.
- Widen the thickness band rather than narrowing it, which raises yield without changing appearance.
- Freeze the specification before bulk. A change after intake re-prices material, tooling and calendar at once.
- Consolidate shipments, which halves the fixed element of a less-than-container load.
- Re-order on a frozen pattern, since a genuine re-order carries no development line at all.
The last lever is the largest and the least used. A re-order on a held pattern and a named lot removes development, tooling and most of the approval calendar, which is why repeat programmes reliably land at the lower end of every range in this article.
How to Read a Quotation You Have Been Sent
Three questions resolve most quotations. First, is the term stated, and is it the same term on every quote you are comparing. Second, are bench hours given, or only a labour rate. Third, is the material named as a lot with a tannery reference, or only as a colour and a grade.
Five checks before you sign
- The trade term is named, with the port and the rules edition current at the contract date.
- Bench hours are stated alongside any labour rate, so the hour count is negotiable rather than implied.
- Material is named by lot reference and tannery, with thickness and finish specified.
- Tooling is separated from unit cost, so you can see what is amortised across how many pieces.
- The inspection plan is stated: AQL 2.5 under ISO 2859-1, with the level and lot size agreed before bulk.
A quotation that survives those five checks is usually a quotation you can hold someone to. One that fails them is usually a number that will move, and the direction is rarely in your favour.
What the Programme Looks Like Behind the Price
Price only means something next to capacity and calendar. Bulk runs 35-50 days from approval, sampling 6-10 working days or 12-15 for complex builds, and inspection is drawn at AQL 2.5 under ISO 2859-1 at general inspection level II, which on a 500 pcs lot means 50 units drawn, accept 3, reject 4. Those figures are what the price is buying: a bench that is not fighting for space, and a lot that is drawn before it is packed.
Our validated partner factory Quanzhou Yingming Bags, an SGS-validated site, has run export programmes since 2014 across 7 production lines at about 200,000 pcs per month, on FOB Xiamen terms with CIF and DDP available. Documentation handling is quoted from USD 4.80 per lot file. Third-party inspection can be added where a retailer requires an independent draw.
See your own bag broken down by line
Send a drawing, a target quantity and the markets you sell into. You will receive the same silhouette quoted at three specifications, each broken down by material, hardware, hours, tooling and compliance, so you can choose the levers yourself. Request a quote.
Frequently Asked Questions
How much does a luxury handbag programme cost per unit?
There is no single figure, because the honest answer is a structure: material 45-60%, hardware 8-18%, bench labour 15-25%, compliance and documentation 3-6%. What moves the total is specification rather than negotiation, and bench hours per unit — roughly 1.5-2, 3-4 or 6-8 — is the clearest single indicator of where a bag sits.
Why do quotations for the same bag differ so much?
Because they are rarely quoting the same bag. Differences in hide grade, plating thickness, edge treatment and whether tooling is amortised across 500 or 3,000 pieces account for almost the whole spread. Ask for bench hours and a named material lot, and the comparison becomes meaningful.
What is the largest cost line on a luxury handbag?
Material, at 45-60% of unit cost. Within it, the largest lever is yield rather than grade: an exotic facing panel can yield well under half the usable area of a calfskin skin of the same nominal size, so more skin is issued per unit for the same silhouette.
How much does a custom closure add to the price?
It adds a die, a proving step and a longer plating cycle, and the visible effect depends on volume. Spread across 500 pcs the tooling carries a noticeable per-unit share; spread across 3,000 pcs it becomes negligible, which is why a bespoke lock is best treated as a multi-season commitment.
Is a bespoke hardware development worth it for a first capsule?
Usually not on volume grounds, though it can be right on brand grounds. The tooling is real and the proving step adds 12-15 working days to sampling. A common compromise is to launch on a high-quality stock closure and introduce the bespoke part on the second season.
What does the minimum order mean for the price?
MOQ 500 pcs per style and colourway is the point at which tooling and development begin to spread. Below it, a bespoke part cannot be amortised at a sensible per-unit figure, which is why the minimum exists as a commercial threshold rather than as an arbitrary rule.
Are development costs charged again on a re-order?
Not on a genuine re-order. Pattern and tooling are charged once per style and per part, so a second run on a frozen pattern carries material, labour and compliance but no development line. That is why repeat programmes land at the lower end of every range.
How does plating thickness affect cost?
Directly, because plating time and metal consumption both scale with thickness. The 0.15-0.3 µm band is what survives 24 hours of neutral salt spray to ISO 9227 without bloom; below roughly 0.15 µm the saving is small and the tarnishing appears within a season on the shelf.
Does freight appear in the unit price?
Not on FOB Xiamen terms, where freight, insurance, duty and destination handling all sit with the buyer. A quotation that bundles them will look higher on the unit line and hides an estimating margin. Always compare two quotes on the same term before drawing conclusions.
What compliance costs should I expect?
Compliance and documentation carry 3-6% of unit cost: REACH Annex XVII and California Prop 65 declarations at lot release, ISO 105-X12 rub fastness where shades are pale, strength reports where a retailer requires them, and permit documents where a listed skin is present. Documentation handling runs from USD 4.80 per lot file.
When should laboratory testing be booked?
When the material lot is named, not when goods are finished. Reports are issued against a lot and take their own calendar days, typically 7-10 for a fastness cycle. A capsule held at the port waiting for a certificate is the most avoidable delay in the programme, so book the laboratory at the moment you reserve the hide.
What is the most effective way to lower the unit price?
The most effective levers are structural rather than negotiable: widening the thickness band to raise yield, keeping a closure across seasons so tooling amortises, consolidating shipments to halve the fixed freight element, and re-ordering on a frozen pattern so no development line returns. None of them require asking anyone for a smaller figure, which is why they hold across quotations.
How long does bulk take once I have agreed a price?
35-50 days from approval on FOB Xiamen terms, following sampling of 6-10 working days, or 12-15 for complex builds. Inspection is drawn at AQL 2.5 under ISO 2859-1 before packing, which on a 500 pcs lot means 50 units drawn, accept 3, reject 4.
Should I ask for a breakdown by percentage or by rate?
By percentage, and then by hours. A percentage breakdown shows which specification decision is driving the total, and an hour count shows what the bench is actually doing. A rate alone tells you nothing about the bag and cannot be negotiated usefully, so ask for both on the written quotation rather than in an email.
People Also Ask
Why is there no fixed price for a luxury handbag?
Because the price is a structure rather than a number: material, hardware, bench hours, tooling and compliance each move independently with specification. Two quotes for one silhouette can legitimately differ by a wide margin and both be honest.
What are bench hours on a handbag?
The number of hours of bench work in one unit: roughly 1.5-2 for a simple build, 3-4 for a house-standard one, and 6-8 where hand-stitched attachments or a framed base are specified. It is the clearest single measure of specification level.
How can I reduce handbag unit cost?
Change the specification rather than the negotiation: widen the leather thickness band, keep a closure across seasons, consolidate shipments, and re-order on a frozen pattern so development does not return.
Does a second colourway cost more to develop?
No. Pattern and tooling are charged once per style and per part, so an additional colourway on an existing body carries material and labour but no development line, which makes it the most efficient first growth move.
Is tooling charged on every order?
Only on the first. A die or plate is charged once and then held for re-orders, so its per-unit effect falls with every subsequent run and becomes negligible by the third or fourth capsule.
Sources and further reading
Every figure on this page is either our own programme data or attributed below. Open the originals before you write them into a specification.
- Leather Working GroupLeather Working Group Tannery audit protocol referenced when a hide lot is named, which affects grade consistency, yield and therefore the material line.
- CITES Appendices I, II and IIICITES Listing that determines when permit documents are required for a facing panel, and why exotic material carries both a documentation cost and lower yield.
- REACH legislation (European Chemicals Agency)ECHA Annex XVII restrictions that generate the declaration line on goods sold into the European market, issued against each material lot.
- ISO — International Organization for StandardizationISO Publisher of ISO 105-X12, ISO 3376, ISO 3377-2, ISO 9227 and ISO 2859-1, the standards behind the compliance and inspection lines in the breakdown.
- Sourcing JournalSourcing Journal Reporting on material pricing, freight conditions and lead times across the leather goods supply chain, useful context for the cost levers described here.